Каталог Iscar дисковые фрезы и фрезерные пластины 2022 - страница 180
Навигация
 Каталог Iscar крепление инструмента
 Каталог Iscar инструмент для обработки отверстий
 Каталог Iscar резьбонарезные фрезы
 Каталог Iscar инструмента для сверления
 Каталог Iscar решения для глубокого сверления
MILLING INSERTS
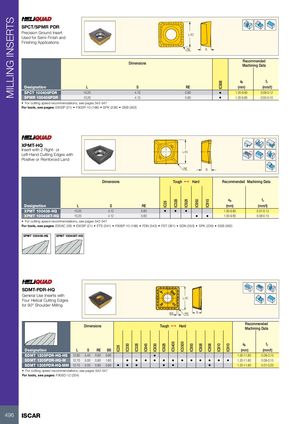
SPCT/SPMR PDR
Precision Ground Insert L/IC
Used for Semi-Finish and
Finishing Applications
RE S
Recommended
Dimensions
Machining Data
ap fz
IC808
Designation L S RE (mm) (mm/t)
SPCT 100408PDR 10.20 4.13 0.80 • 1.20-9.60 0.08-0.12
SPMR 100408PDR 10.20 4.13 0.80 • 1.20-9.60 0.05-0.10
• For cutting speed recommendations, see pages 542-547
For tools, see pages: E90SP (21) • F90SP-10 (198) • SPK (239) • SSB (362)
XPMT-HQ
HQ
Insert with 2 Right- or L/IC Rd°
Left-Hand Cutting Edges with
Positive or Reinforced Land HQ
RE S
Dimensions Tough 1 Hard Recommended Machining Data
ap fz
IC328
IC928
IC950
IC910
IC28
Designation L S RE (mm) (mm/t)
XPMT 100408-HQ 10.20 4.12 0.60 • • • 1.00-9.60 0.07-0.12
XPMT 100408T-HQ 10.20 4.12 0.60 • • 1.00-9.60 0.08-0.15
• For cutting speed recommendations, see pages 542-547
For tools, see pages: E90AC (36) • E90SP (21) • ETS (341) • F90SP-10 (198) • FDN (342) • FST (361) • SDN (353) • SPK (239) • SSB (362)
XPMT 100408-HQ XPMT 100408T-HQ
SDMT-PDR-HQ
General Use Inserts with
L/IC
Four Helical Cutting Edges
for 90° Shoulder Milling
BS RE S
Recommended
Dimensions Tough 1 Hard
Machining Data
ap fz
IC5400
IC5500
IC330
IC328
IC845
IC830
IC928
IC950
IC808
IC908
IC810
IC910
IC28
Designation L S RE BS (mm) (mm/t)
SDMT 1205PDR-HQ-HS 12.60 5.40 0.60 0.80 • 1.00-11.80 0.08-0.15
SDMT 1205PDR-HQ-M 12.70 5.00 0.80 1.60 • • • • • • • • • • • • 1.20-11.80 0.08-0.15
SDMT 1205PDR-HQ-MM 12.75 5.00 0.80 0.80 • • • • • • 1.20-11.80 0.07-0.20
• For cutting speed recommendations, see pages 542-547
For tools, see pages: F90SD-12 (204)
496 ISCAR