Каталог Iscar дисковые фрезы и фрезерные пластины 2022 - страница 174
Навигация
 Каталог Iscar крепление инструмента
 Каталог Iscar инструмент для обработки отверстий
 Каталог Iscar резьбонарезные фрезы
 Каталог Iscar инструмента для сверления
 Каталог Iscar решения для глубокого сверления
MILLING INSERTS
S W1
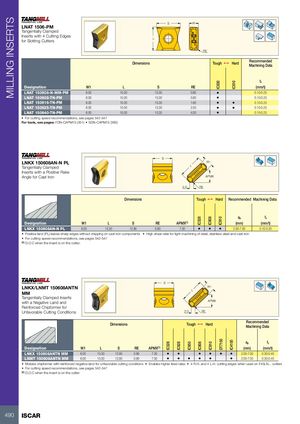
LNAT 1506-PM
Tangentially Clamped
Inserts with 4 Cutting Edges
L
for Slotting Cutters
RE
Recommended
Dimensions Tough 1 Hard
Machining Data
fz
IC830
IC810
Designation W1 L S RE (mm/t)
LNAT 150608-N-MM-PM 6.00 15.00 15.30 0.80 • 0.10-0.25
LNAT 150608-TN-PM 6.00 15.00 15.30 0.80 • 0.10-0.25
LNAT 150616-TN-PM 6.00 15.00 15.30 1.60 • • 0.10-0.25
LNAT 150625-TN-PM 6.00 15.00 15.30 2.50 • • 0.10-0.25
LNAT 150640-TN-PM 6.00 15.00 15.30 4.00 • 0.10-0.25
• For cutting speed recommendations, see pages 542-547
For tools, see pages: FDN-CAPM15 (351) • SDN-CAPM15 (360)
S
LNKX 150608AN-N PL W1
L
Tangentially Clamped
Inserts with a Positive Rake
Angle for Cast Iron APMX
2.0 RE
Dimensions Tough 1 Hard Recommended Machining Data
ap fz
IC328
IC908
IC910
Designation W1 L S RE APMX(1) (mm) (mm/t)
LNKX 150608AN-N PL 6.00 15.30 12.90 0.80 7.50 • • • 2.00-7.00 0.10-0.20
• Positive land (PL) leaves sharp edges without chipping on cast iron components • High shear rake for light machining of steel, stainless steel and cast iron
• For cutting speed recommendations, see pages 542-547
(1) D.O.C when the insert is on the cutter.
S
W1
LNKX/LNMT 150608ANTN L
MM
Tangentially Clamped Inserts
APMX
with a Negative Land and
Reinforced Chipformer for
Unfavorable Cutting Conditions 2.0 RE
Recommended
Dimensions Tough 1 Hard
Machining Data
DT7150
ap fz
IC4100
IC328
IC928
IC950
IC908
IC910
Designation W1 L S RE APMX(1) (mm) (mm/t)
LNKX 150608ANTN MM 6.00 15.30 12.90 0.80 7.50 • • • • • • 2.00-7.00 0.30-0.40
LNMT 150608ANTN MM 6.00 15.30 12.90 0.80 7.50 • • • • • • 2.00-7.00 0.30-0.40
• Molded chipformer with reinforced negative land for unfavorable cutting conditions • Enables higher feed rates • 4 R.H. and 4 L.H. cutting edges when used on F45LN... cutters
• For cutting speed recommendations, see pages 542-547
(1) D.O.C when the insert is on the cutter
490 ISCAR