Каталог Iscar дисковые фрезы и фрезерные пластины 2022 - страница 167
Навигация
 Каталог Iscar крепление инструмента
 Каталог Iscar инструмент для обработки отверстий
 Каталог Iscar резьбонарезные фрезы
 Каталог Iscar инструмента для сверления
 Каталог Iscar решения для глубокого сверления
X45PN-R-S X75PN-R-S
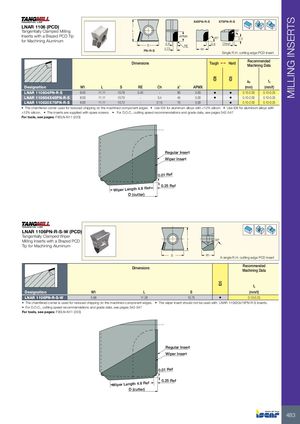
LNAR 1106 (PCD)
| Tangentially Clamped Milling | L | 15° | ||
| Inserts with a Brazed PCD Tip | APMX | |||
| 45° | 2.0 | |||
| for Machining Aluminum |
2.6 0.4 Chxa°
S RE 1.75 W PN-R-S 1 Single R.H. cutting edge PCD insert
Recommended
Dimensions Tough 1 Hard Machining Data
a f
p z
| Designation | W1 | L | S | RE | Ch | a° | APMX | (mm) | (mm/t) | ||
| LNAR 110604PN-R-S | 6.00 | 11.11 | 10.76 | 0.40 | - | 90 | 5.00 | • | • | 0.10-2.00 | 0.10-0.25 |
| LNAR 110604X45PN-R-S | 6.00 | 11.11 | 10.70 | - | 0.4 | 45 | 5.00 | • | • | 0.10-2.00 | 0.10-0.25 |
| LNAR 110620X75PN-R-S | 6.00 | 11.11 | 10.72 | - | 0.15 | 75 | 5.00 | • | 0.10-2.00 | 0.10-0.25 |
- The chamfered corner used for reduced chipping on the machined component edges
- Use ID5 for aluminum alloys with <12% silicon
- Use ID8 for aluminum alloys with
>12% silicon. The inserts are supplied with spare screws. For D.O.C., cutting speed recommendations and grade data, see pages 542-547
For tools, see pages: F90LN-N11 (203)
Wiper Length 4.6 Ref D (cutter)
Regular Insert Wiper Insert
0.01 Ref 0.25 Ref
LNAR 1106PN-R-S-W (PCD)
Tangentially Clamped Wiper
Milling Inserts with a Brazed PCD L 30º
Tip for Machining Aluminum S W1 A single R.H. cutting edge PCD insert Recommended
Dimensions
Machining Data
fz
| Designation | W1 | L | S | (mm/t) | |
| LNAR 1106PN-R-S-W | 5.98 | 11.26 | 10.75 | • | 0.10-0.25 |
- The chamfered corner is used for reduced chipping on the machined component edges.
- The wiper insert should not be used with LNAR 110620x75PN-R-S inserts.
- For D.O.C., cutting speed recommendations and grade data, see pages 542-547
For tools, see pages: F90LN-N11 (203)
Wiper Length 4.6 Ref D (cutter)
Regular Insert Wiper Insert
0.01 Ref 0.25 Ref