Каталог Iscar дисковые фрезы и фрезерные пластины 2022 - страница 168
Навигация
 Каталог Iscar крепление инструмента
 Каталог Iscar инструмент для обработки отверстий
 Каталог Iscar резьбонарезные фрезы
 Каталог Iscar инструмента для сверления
 Каталог Iscar решения для глубокого сверления
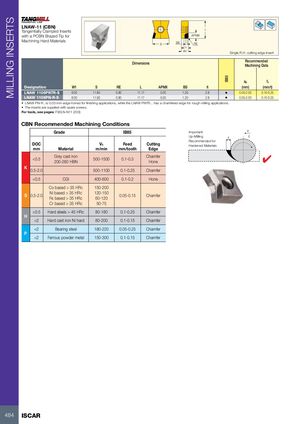
LNAW-11 (CBN) Tangentially Clamped Inserts L with a PCBN Brazed Tip for APMX Machining Hard Materials
S BS RE
lt W1 Single R.H. cutting edge insert Recommended Dimensions Machining Data
a f p z
| Designation | W1 | S | RE | L | APMX | BS | lt | (mm) | (mm/t) | |
| LNAW 1106PNTR-S | 6.00 | 11.80 | 0.80 | 11.17 | 5.00 | 1.20 | 2.8 | • | 0.05-2.00 | 0.10-0.25 |
| LNAW 1106PN-R-S | 6.00 | 11.90 | 0.80 | 11.17 | 5.00 | 1.20 | 2.8 | • | 0.05-2.00 | 0.10-0.25 |
- LNAW PN-R.. is 0.03 mm edge-honed for finishing applications, while the LNAW PNTR... has a chamfered edge for rough milling applications.
- The inserts are supplied with spare screws.
For tools, see pages: F90LN-N11 (203)
CBN Recommended Machining Conditions
| Grade | IB85 | ||||
| D | OC mm | Material | Vc m/min | Feed mm/tooth | Cutting Edge |
| Grey cast iron 200-280 HBN | 500-1500 | 0.1-0.3 | Chamfer Hone | ||
| K 0. | 5-2.0 | 500-1100 | 0.1-0.25 | Chamfer | |
| CGI | 400-600 | 0.1-0.2 | Hone | ||
| S 0. | 5-2.0 | Co based > 35 HRc Ni based > 35 HRc Fe based > 35 HRc | 150-200 120-150 60-120 | 0.05-0.15 | Chamfer |
| Cr based > 35 HRc | 50-75 | ||||
| H | Hard steels > 45 HRc | 80-180 | 0.1-0.25 | Chamfer | |
| Hard cast iron Ni hard | 80-200 | 0.1-0.15 | Chamfer | ||
| P | Bearing steel | 180-220 | 0.05-0.25 | Chamfer | |
| Ferrous powder metal | 150-300 | 0.1-0.15 | Chamfer |
Up-Milling f f
Recommended for Hardened Materials