Каталог Iscar дисковые фрезы и фрезерные пластины 2022 - страница 166
Навигация
 Каталог Iscar крепление инструмента
 Каталог Iscar инструмент для обработки отверстий
 Каталог Iscar резьбонарезные фрезы
 Каталог Iscar инструмента для сверления
 Каталог Iscar решения для глубокого сверления
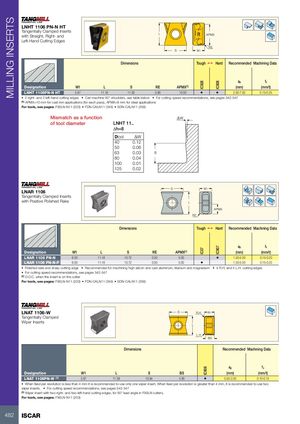
LNHT 1106 PN-N HT with Straight, Right- and Left-Hand Cutting Edges
L APMX
RE S W 1
Dimensions Tough 1 Hard Recommended Machining Data
a f p z
| Designation | W1 | L | S | RE | APMX(1) | (mm) | (mm/t) | ||
| LNHT 1106PN-N HT | 5.97 | 11.16 | 11.00 | 0.80 | 10.00 | • | • | 2.00-7.00 | 0.15-0.25 |
- 2 right- and 2 left-hand cutting edges
- Can machine 90° shoulders, see table below
- For cutting speed recommendations, see pages 542-547
(1) APMX=10 mm for cast iron applications (for each pass), APMX=8 mm for steel applications
For tools, see pages: F90LN-N11 (203) FDN-CALN11 (349) SDN-CALN11 (359)
Mismatch as a function ∆W
of tool diameter LNHT 11.. ∆h=8 Dtool ∆W 40 0.12 50 0.06
63 0.03 8
80 0.04 100 0.01 125 0.02
LNAR 1106 Tangentially Clamped Inserts with Positive Polished Rake
Dimensions
S
W1
L APMX RE
Tough 1 Hard Recommended Machining Data
a f p z
| Designation | W1 | L | S | RE | APMX(1) | (mm) | (mm/t) | ||
| LNAR 1106 PN-N | 6.00 | 11.16 | 10.72 | 0.50 | 5.00 | • | 1.50-5.00 | 0.15-0.20 | |
| LNAR 1106 PN-N-P | 6.00 | 11.16 | 10.72 | 0.50 | 5.00 | • | 1.50-5.00 | 0.15-0.20 |
- Polished rake and sharp cutting edge
- Recommended for machining high silicon and cast aluminum, titanium and magnesium
- 4 R.H. and 4 L.H. cutting edges
- For cutting speed recommendations, see pages 542-547
(1) D.O.C. when the insert is on the cutter
For tools, see pages: F90LN-N11 (203) FDN-CALN11 (349) SDN-CALN11 (359)
LNAT 1106-W Tangentially Clamped Wiper Inserts
S R.H W
1
L L.H BS Dimensions Recommended Machining Data
a f p z
| Designation | W1 | L | S | BS | (mm) | (mm/t) | |
| LNAT 1106PN-W (1) | 5.97 | 11.38 | 10.94 | 4.90 | • | 0.50-2.00 | 0.10-0.15 |
- When feed per revolution is less than 4 mm it is recommended to use only one wiper insert. When feed per revolution is greater than 4 mm, it is recommended to use two
wiper inserts. For cutting speed recommendations, see pages 542-547 (1) Wiper insert with two right- and two left-hand cutting edges, for 90° lead angle in F90LN cutters.
For tools, see pages: F90LN-N11 (203)