Каталог Iscar дисковые фрезы и фрезерные пластины 2022 - страница 165
Навигация
 Каталог Iscar крепление инструмента
 Каталог Iscar инструмент для обработки отверстий
 Каталог Iscar резьбонарезные фрезы
 Каталог Iscar инструмента для сверления
 Каталог Iscar решения для глубокого сверления
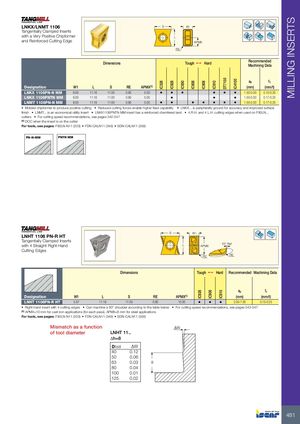
LNKX/LNMT 1106 with a Very Positive Chipformer and Reinforced Cutting Edge
S W L APMX RE Recommended
Dimensions Tough 1 Hard Machining Data
a f p z
| Designation | W1 | L | S | RE | APMX(1) | (mm) | (mm/t) | ||||||||
| LNKX 1106PN-N MM | 6.00 | 11.16 | 11.00 | 0.80 | 5.00 | • | • | • | • | • | • | 1.50-5.00 | 0.15-0.20 | ||
| LNKX 1106PNTN MM | 6.00 | 11.16 | 11.00 | 0.80 | 5.00 | • | • | • | 1.50-5.00 | 0.17-0.25 | |||||
| LNMT 1106PN-N MM | 6.00 | 11.16 | 11.00 | 0.80 | 5.00 | • | • | • | • | • | • | • | 1.50-5.00 | 0.17-0.25 |
- Molded chipformer to produce positive cutting
- Reduced cutting forces enable higher feed capability
- LNKX... is peripherally ground for accuracy and improved surface
finish LNMT... is an economical utility insert LNKX1106PNTN MM insert has a reinforced chamfered land 4 R.H. and 4 L.H. cutting edges when used on F90LN... cutters For cutting speed recommendations, see pages 542-547 (1) DOC when the insert is on the cutter
For tools, see pages: F90LN-N11 (203) FDN-CALN11 (349) SDN-CALN11 (359)
PN-N-MM PNTN MM
LNHT 1106 PN-R HT Tangentially Clamped Inserts with 4 Straight Right-Hand Cutting Edges
S
L
W1 10° Ref. APMX RE RE
Dimensions Tough 1 Hard Recommended Machining Data
a f p z
| Designation | W1 | L | S | RE | APMX(1) | (mm) | (mm/t) | |||
| LNHT 1106PN-R HT | 5.97 | 11.16 | 11.00 | 0.80 | 10.00 | • | • | • | 2.00-7.00 | 0.15-0.25 |
- Right-hand insert with 4 cutting edges
- Can machine a 90° shoulder according to the table below
- For cutting speed recommendations, see pages 542-547
(1) APMX=10 mm for cast iron applications (for each pass), APMX=8 mm for steel applications
For tools, see pages: F90LN-N11 (203) FDN-CALN11 (349) SDN-CALN11 (359)
Mismatch as a function ∆W
of tool diameter LNHT 11.. ∆h=8 Dtool ∆W 40 0.12 50 0.06
63 0.03 8
80 0.04 100 0.01 125 0.02