Каталог Iscar дисковые фрезы и фрезерные пластины 2022 - страница 159
Навигация
 Каталог Iscar крепление инструмента
 Каталог Iscar инструмент для обработки отверстий
 Каталог Iscar резьбонарезные фрезы
 Каталог Iscar инструмента для сверления
 Каталог Iscar решения для глубокого сверления
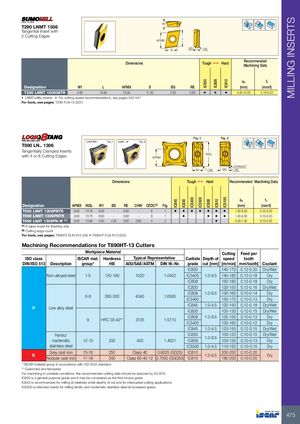
T290 LNMT 1506 Tangential Insert with 2 Cutting Edges
W 1
APMX S
Dimensions
L
BS RE Recommended
Tough 1 Hard Machining Data
a f p z
| Designation | W1 | L | APMX | S | BS | RE | (mm) | (mm/t) | |||
| T290 LNMT 150608TR | 5.60 | 15.90 | 15.00 | 11.50 | 2.00 | 0.80 | • | • | • | 5.00-15.00 | 0.10-0.22 |
- LNMT-utility inserts
- For cutting speed recommendations, see pages 542-547
For tools, see pages: T290 FLN-15 (207)
T890 LN.. 1306 Tangentially Clamped Inserts with 4 or 8 Cutting Edges
APMX
Dimensions
Fig. 1 Fig. 2
INSL
CHWx45°
| W | RE | BS | RE |
| 1 |
Tough 1 Hard Recommended Machining Data
a f p z
| Designation | APMX INSL | W1 | BS | RE | CHW CEDC(2) | Fig. | (mm) | (mm/t) | ||||||
| T890 LNHT 1306PNTR | 9.50 | 13.78 | 6.00 | - | 0.80 | - | 8 | 1 | • • • • • • • | 1.00-9.50 | 0.10-0.20 | |||
| T890 LNMT 1306PNTR | 9.50 | 13.75 | 6.00 | - | 0.80 | - | 8 | 1 | • | • • • | 1.00-9.50 | 0.10-0.20 | ||
| T890 LNAT 1306PN-W (1) | 9.50 | 13.92 | 5.90 | 4.30 | 0.60 | 0.60 | 4 | 2 | • | 0.50-1.00 | 0.10-0.20 |
(1) A wiper insert for finishing only (2) Cutting edge count For tools, see pages: T890HT ELN-R13 (29) T890HT FLN-R13 (202) Machining Recommendations for T890HT-13 Cutters
| Workpie | ce Material | Cutting | Feed per | ||||||
| ISO class | ISCAR mat. | Hardness | Typical Repr | esentative | Carbide | Depth of | speed | tooth | |
| DIN/ISO 513 Description | group | HB | AISI/SAE/ASTM | DIN W.-Nr. | grade | cut[mm] | [m/min] | mm/tooth] | Coolant |
| IC830 | 140-170 | 0.12-0.20 | Dry/Wet | ||||||
| Non-alloyed steel | 1-5 | 130-180 | 1020 | 1.0402 | IC5400 | 1.0-9.5 | 140-180 | 0.12-0.18 | Dry |
| IC808 | 150-180 | 0.12-0.18 | Dry | ||||||
| IC830 | 120-150 | 0.12-0.16 | Dry/Wet | ||||||
| 6-8 | 260-300 | 4340 | 16565 | IC808 | 1.0-9.5 | 130-160 | 0.10-0.14 | Dry | |
| . | IC5400 | 150-170 | 0.10-0.13 | Dry | |||||
| P Low allo steel | IC845 | 1.0-4.5 | 120-150 | 0.12-0.18 | Dry/Wet | ||||
| y | IC830 | 100-130 | 0.12-0.15 | Dry/Wet | |||||
| 9 | HRC 35-42 | 3135 | 15710 | IC808 | 1.0-9.5 | 120-150 | 0.10-0.13 | Dry | |
| . | IC5400 | 130-160 | 0.10-0.12 | Dry | |||||
| IC845 | 1.0-4.5 | 120-150 | 0.12-0.15 | Dry/Wet | |||||
| Ferritic/ | IC830 | 10-95 | 100-120 | 0.10-0.15 | Dry/Wet | ||||
| martensitic | 12-13 | 200 | 420 | 1.4021 | IC808 | .. | 100-130 | 0.10-0.13 | Dry |
| stainless steel | IC5500 | 1.0-4.5 | 110-150 | 0.10-0.15 | Dry | ||||
| K Greycast iron | 15-16 | 250 | Class 40 | 0.6025(GG25) | IC810 | 10-95 | 200-250 | 0.10-0.20 | Dr |
| Nodular cast iron | 17-18 | 200 | Class 65-45-12 | 0.7050(GGG50) | IC810 | .. | 180-200 | 0.10-0.20 | y |
* ISCAR material group in accordance with VDI 3323 standard ** Quenched and tempered For machining in unstable conditions, the recommended cutting data should be reduced by 20-30% IC830 is a general purpose grade and it may be considered as the first-choice grade IC845 is recommended for milling at relatively small depths of cut and for interrupted cutting applications IC5500 is intended mainly for milling ferritic and martensitic stainless steel at increased speed