Каталог Iscar дисковые фрезы и фрезерные пластины 2022 - страница 156
Навигация
 Каталог Iscar крепление инструмента
 Каталог Iscar инструмент для обработки отверстий
 Каталог Iscar резьбонарезные фрезы
 Каталог Iscar инструмента для сверления
 Каталог Iscar решения для глубокого сверления
MILLING INSERTS
W1
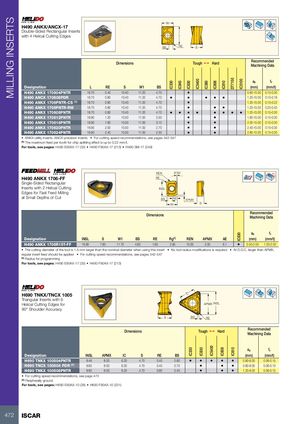
H490 ANKX/ANCX-17
Double-Sided Rectangular Inserts
1
with 4 Helical Cutting Edges L
3
BS RE S
Recommended
Dimensions Tough 1 Hard
Machining Data
DT7150
ap fz
IC5400
IC5100
IC330
IC845
IC830
IC380
IC808
IC810
Designation L RE S W1 BS (mm) (mm/t)
H490 ANKX 170604PNTR 16.70 0.40 10.40 11.20 4.70 • 0.80-15.00 0.15-0.30
H490 ANCX 170608PDR 16.70 0.80 10.40 11.20 4.70 • • • • • 1.20-15.00 0.10-0.18
H490 ANKX 1706PNTR-CS (1) 16.70 0.80 10.40 11.20 4.70 • 1.20-15.00 0.15-0.22
H490 ANKX 1706PNTR-RM 16.70 0.80 10.40 11.20 4.70 • • • 1.20-15.00 0.20-0.40
H490 ANKX 170608PNTR 16.70 0.80 10.40 11.20 4.70 • • • • • • • • 1.20-15.00 0.15-0.30
H490 ANKX 170612PNTR 16.90 1.20 10.50 11.00 3.50 • • 1.60-15.00 0.15-0.30
H490 ANKX 170616PNTR 16.90 1.60 10.50 11.00 3.10 • • 2.00-15.00 0.15-0.30
H490 ANKX 170620PNTR 16.90 2.00 10.50 11.00 2.70 • • 2.40-15.00 0.15-0.30
H490 ANKX 170624PNTR 16.90 2.40 10.50 11.00 2.30 • • 2.80-15.00 0.15-0.30
• ANKX-utility inserts. ANCX-precision inserts • For cutting speed recommendations, see pages 542-547
(1) The maximum feed per tooth for chip splitting effect is up to 0.22 mm/t.
For tools, see pages: H490 E90AX-17 (33) • H490 F90AX-17 (213) • H490 SM-17 (249)
REN 3º30’ Rd°
H490 ANKX 1706-FF RE
Single-Sided Rectangular
Inserts with 2 Helical Cutting lNSL
Edges for Fast Feed Milling
at Small Depths of Cut BS AE
APMX
W1 S
Recommended
Dimensions
Machining Data
ap fz
Designation INSL S W1 BS RE Rg(1) REN APMX AE IC830 (mm) (mm/t)
H490 ANKX 1706R15T-FF 16.80 7.80 11.70 4.60 1.60 2.85 15.00 2.00 6.1 • 0.50-2.00 1.00-2.00
• The cutting diameter of the tool is 1.5 mm larger than the nominal diameter when using this insert • No tool radius modifications is required • At D.O.C. larger than APMX,
regular insert feed should be applied • For cutting speed recommendations, see pages 542-547
(1) Radius for programming
For tools, see pages: H490 E90AX-17 (33) • H490 F90AX-17 (213)
IC
H690 TNKX/TNCX 1005 2
Triangular Inserts with 6
APMX INSL
1
Helical Cutting Edges for
90° Shoulder Accuracy 3
S BS RE
Recommended
Dimensions Tough 1 Hard
Machining Data
IC5400
ap fz
IC330
IC830
IC808
IC810
Designation INSL APMX IC S RE BS (mm) (mm/t)
H690 TNKX 100504PNTR 8.48 8.00 6.20 4.70 0.40 0.80 • • • • • 0.80-8.00 0.08-0.15
H690 TNCX 100504 PDR (1) 8.60 8.00 6.20 4.70 0.40 0.70 • • • 0.80-8.00 0.08-0.13
H690 TNKX 100508PNTR 8.60 8.00 6.20 4.70 0.80 0.40 • • • 1.20-8.00 0.08-0.15
• For cutting speed recommendations, see page 473
(1) Peripherally ground
For tools, see pages: H690 E90AX-10 (28) • H690 F90AX-10 (201)
472 ISCAR