Каталог Iscar дисковые фрезы и фрезерные пластины 2022 - страница 154
Навигация
 Каталог Iscar крепление инструмента
 Каталог Iscar инструмент для обработки отверстий
 Каталог Iscar резьбонарезные фрезы
 Каталог Iscar инструмента для сверления
 Каталог Iscar решения для глубокого сверления
MILLING INSERTS
REN 3°30’
RE
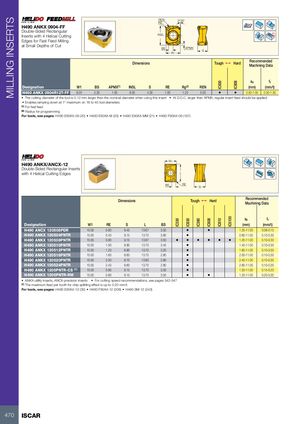
H490 ANKX 0904-FF
Double-Sided Rectangular Rd°
INSL
Inserts with 4 Helical Cutting
Edges for Fast Feed Milling
at Small Depths of Cut APMX
BS
S
W1
Recommended
Dimensions Tough 1 Hard
Machining Data
ap fz
IC830
IC808
Designation W1 BS APMX(1) INSL S RE Rg(2) REN (mm) (mm/t)
H490 ANKX 0904R12T-FF 6.20 2.30 1.00 8.50 4.30 1.00 1.20 5.00 • • 0.50-1.00 0.50-1.50
• The cutting diameter of the tool is 0.12 mm larger than the nominal diameter when using this insert • At D.O.C. larger than APMX, regular insert feed should be applied
• Enables ramping down at 1° maximum on 16 to 40 tool diameters
(1) For fast feed
(2) Radius for programming
For tools, see pages: H490 E90AX-09 (20) • H490 E90AX-M (20) • H490 E90AX-MM (21) • H490 F90AX-09 (197)
W1
H490 ANKX/ANCX-12
Double-Sided Rectangular Inserts 1
with 4 Helical Cutting Edges L
3
BS RE
S
Recommended
Dimensions Tough 1 Hard
Machining Data
ap fz
IC5100
IC330
IC830
IC380
IC808
IC810
Designation W1 RE S L BS (mm) (mm/t)
H490 ANCX 120508PDR 10.00 0.80 9.45 13.67 3.50 • • 1.20-11.00 0.08-0.15
H490 ANKX 120504PNTR 10.00 0.40 9.15 13.70 3.80 • 0.80-11.00 0.10-0.30
H490 ANKX 120508PNTR 10.00 0.80 9.15 13.67 3.50 • • • • • • 1.20-11.00 0.10-0.30
H490 ANKX 120510PNTR 10.00 1.00 8.90 13.70 3.40 • 1.40-11.00 0.10-0.30
H490 ANKX 120512PNTR 10.00 1.20 8.90 13.70 3.20 • 1.60-11.00 0.10-0.30
H490 ANKX 120516PNTR 10.00 1.60 8.60 13.70 2.80 • 2.00-11.00 0.10-0.30
H490 ANKX 120520PNTR 10.00 2.00 8.70 13.60 2.80 • 2.40-11.00 0.10-0.30
H490 ANKX 120524PNTR 10.00 2.40 8.60 13.70 2.80 • 2.80-11.00 0.10-0.30
H490 ANKX 1205PNTR-CS (1) 10.00 0.80 9.15 13.70 3.50 • 1.20-11.00 0.15-0.20
H490 ANKX 1205PNTR-RM 10.00 0.80 9.15 13.70 3.50 • • 1.20-11.00 0.20-0.30
• ANKX-utility inserts, ANCX-precision inserts • For cutting speed recommendations, see pages 542-547
(1) The maximum feed per tooth for chip splitting effect is up to 0.20 mm/t.
For tools, see pages: H490 E90AX-12 (30) • H490 F90AX-12 (206) • H490 SM-12 (243)
470 ISCAR