Каталог Iscar дисковые фрезы и фрезерные пластины 2022 - страница 138
Навигация
 Каталог Iscar крепление инструмента
 Каталог Iscar инструмент для обработки отверстий
 Каталог Iscar резьбонарезные фрезы
 Каталог Iscar инструмента для сверления
 Каталог Iscar решения для глубокого сверления
MILLING INSERTS
RE RE9.9 Rd°
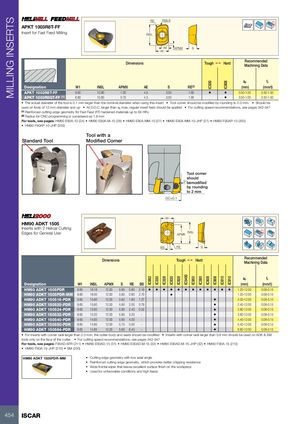
APKT 1003R8T-FF
Insert for Fast Feed Milling INSL
AE APMX S
W1
Recommended
Dimensions Tough 1 Hard
Machining Data
ap fz
IC830
IC808
Designation W1 INSL APMX AE S RE(2) (mm) (mm/t)
APKT 1003R8T-FF 6.60 10.80 1.00 4.5 3.50 1.90 • • 0.50-1.00 0.50-1.50
APKT 1003R8GT-FF (1) 6.60 10.80 0.70 4.5 3.50 1.90 • 0.50-1.00 0.50-1.50
• The actual diameter of the tool is 0.1 mm larger than the nominal diameter when using this insert • Tool corner should be modified by rounding to 2.0 mm. • Should be
used on tools of 12 mm diameter and up • At D.O.C. larger than ap max, regular insert feed should be applied • For cutting speed recommendations, see pages 542-547
(1) Reinforced cutting-edge geometry for Fast Feed (FF) hardened materials up to 64 HRc
(2) Radius for CNC programming is considered as 1.8 mm
For tools, see pages: HM90 E90A-10 (24) • HM90 E90A-M-10 (28) • HM90 E90A-MM-10 (27) • HM90 E90A-MM-10-JHP (27) • HM90 F90AP-10 (200)
• HM90 F90AP-10-JHP (200)
Tool with a
Standard Tool Modified Corner
Tool corner
should
3° bemodified
by rounding
to 2 mm
DC+0.1
W1
HM90 ADKT 1505
Inserts with 2 Helical Cutting Rd°
Edges for General Use INSL
APMX
BS RE S
Recommended
Dimensions Tough 1 Hard
Machining Data
IC5400
ap fz
IC882
IC330
IC328
IC830
IC928
IC950
IC380
IC808
IC908
IC810
IC910
Designation W1 INSL APMX S RE BS (mm) (mm/t)
HM90 ADKT 1505PDR 9.65 16.18 12.00 5.85 0.80 2.16 • • • • • • • • • • • • 1.20-12.00 0.08-0.15
HM90 ADKT 1505PDR-MM 9.60 16.00 12.00 5.80 0.80 2.70 • 1.20-12.00 0.08-0.15
HM90 ADKT 150516-PDR 9.65 15.60 12.00 5.92 1.60 1.37 • 2.00-12.00 0.08-0.15
HM90 ADKT 150520-PDR 9.65 15.60 12.00 5.90 2.00 0.79 • 2.40-12.00 0.08-0.15
HM90 ADKT 150524-PDR 9.65 15.60 12.00 5.80 2.40 0.52 • 2.80-12.00 0.08-0.15
HM90 ADKT 150532-PDR 9.65 15.20 12.00 5.85 3.20 - • 3.60-12.00 0.08-0.15
HM90 ADKT 150540-PDR 9.65 14.83 12.00 5.80 4.00 - • 4.40-12.00 0.08-0.15
HM90 ADKT 150550-PDR 9.65 14.85 12.00 5.75 5.00 - • 5.40-12.00 0.08-0.15
HM90 ADKT 150564-PDR 9.65 14.85 12.00 5.65 6.40 - • 6.80-12.00 0.08-0.15
• For inserts with corner radii larger than 2.0 mm, the cutter body and seats should be modified • Inserts with corner radii larger than 0.8 mm should be used on ADK & SM
tools only on the face of the cutter. • For cutting speed recommendations, see pages 542-547
For tools, see pages: F90AD-SFR (211) • HM90 E90AD-15 (31) • HM90 E90AD-M-15 (32) • HM90 E90AD-M-15-JHP (32) • HM90 F90A-15 (210)
• HM90 F90A-15-JHP (210) • SM (250)
HM90 ADKT 1505PDR-MM • Cutting edge geometry with low axial angle
• Reinforced cutting edge geometry, which provides better chipping resistance
• Wide frontal wiper that leaves excellent surface finish on the workpiece
• Used for unfavorable conditions and high feeds
454 ISCAR