Каталог Iscar дисковые фрезы и фрезерные пластины 2022 - страница 135
Навигация
 Каталог Iscar крепление инструмента
 Каталог Iscar инструмент для обработки отверстий
 Каталог Iscar резьбонарезные фрезы
 Каталог Iscar инструмента для сверления
 Каталог Iscar решения для глубокого сверления
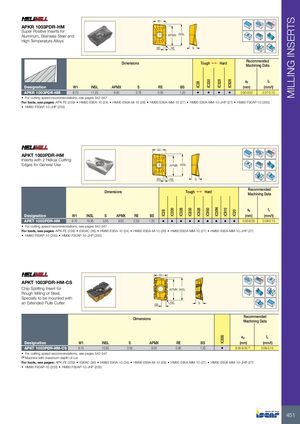
APKR 1003PDR-HM Super Positive Inserts for Aluminum, Stainless Steel and High Temperature Alloys
APMX INSL
BS RE S
Recommended
Dimensions Tough 1 Hard Machining Data
a f p z
| Designation | W1 | INSL | APMX | S | RE | BS | (mm) | (mm/t) | ||||
| APKR 1003PDR-HM | 6.70 | 11.20 | 8.00 | 3.76 | 0.50 | 1.20 | • | • | • | • | 0.90-8.00 | 0.07-0.15 |
- For cutting speed recommendations, see pages 542-547
For tools, see pages: APK-FE (239) HM90 E90A-10 (24) HM90 E90A-M-10 (28) HM90 E90A-MM-10 (27) HM90 E90A-MM-10-JHP (27) HM90 F90AP-10 (200)
- HM90 F90AP-10-JHP (200)
APKT 1003PDR-HM Inserts with 2 Helical Cutting Edges for General Use
W1
APMX INSL
BS RE S
Dimensions Tough 1 Hard
Rd°
Recommended Machining Data
a f p z
| Designation | W1 | INSL | S | APMX | RE | BS | (mm) | (mm/t) | |||||||||
| APKT 1003PDR-HM | 6.70 | 10.95 | 3.55 | 8.00 | 0.50 | 1.20 | • | • | • | • | • | • | • | • | • | 0.90-8.00 | 0.08-0.15 |
- For cutting speed recommendations, see pages 542-547
For tools, see pages: APK-FE (239) E90AC (36) HM90 E90A-10 (24) HM90 E90A-M-10 (28) HM90 E90A-MM-10 (27) HM90 E90A-MM-10-JHP (27)
- HM90 F90AP-10 (200)
- HM90 F90AP-10-JHP (200)
W1 Rd° APKT 1003PDR-HM-CS Chip Splitting Insert for APMX INSL Rough Milling of Steel, Specially to be mounted with
an Extended Flute Cutter RE S
BS Recommended Dimensions Machining Data
ap fz
| Designation | W1 | INSL | S | APMX | RE | BS | (mm) | (mm/t) | |
| APKT 1003PDR-HM-CS | 6.70 | 10.95 | 3.55 | 8.00 | 0.80 | 1.20 | • | 8.00-8.00 (1) | 0.08-0.15 |
- For cutting speed recommendations, see pages 542-547
(1) Machine with maximum depth of cut
For tools, see pages: APK-FE (239) E90AC (36) HM90 E90A-10 (24) HM90 E90A-M-10 (28) HM90 E90A-MM-10 (27) HM90 E90A-MM-10-JHP (27)
- HM90 F90AP-10 (200)
- HM90 F90AP-10-JHP (200)