Каталог Iscar дисковые фрезы и фрезерные пластины 2022 - страница 134
Навигация
 Каталог Iscar крепление инструмента
 Каталог Iscar инструмент для обработки отверстий
 Каталог Iscar резьбонарезные фрезы
 Каталог Iscar инструмента для сверления
 Каталог Iscar решения для глубокого сверления
APMX RE BS
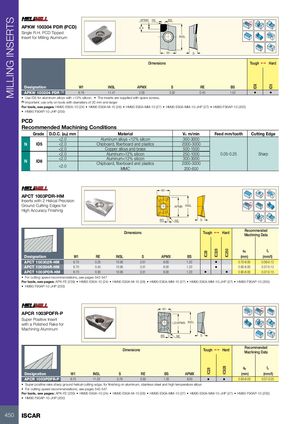
APKW 100304 PDR (PCD) Single R.H. PCD Tipped Insert for Milling Aluminum lNSL
W1 S
Dimensions Tough 1 Hard
| Designation | W1 | INSL | APMX | S | RE | BS | ||
| APKW 100304 PDR (1) | 6.76 | 11.47 | 2.00 | 3.50 | 0.40 | 1.52 | • | • |
- Use ID5 for aluminum alloys with <12% silicon.
- The inserts are supplied with spare screws.
(1) Important: use only on tools with diameters of 20 mm and larger
For tools, see pages: HM90 E90A-10 (24) HM90 E90A-M-10 (28) HM90 E90A-MM-10 (27) HM90 E90A-MM-10-JHP (27) HM90 F90AP-10 (200)
- HM90 F90AP-10-JHP (200)
PCD
Recommended Machining Conditions
| Grade | D.O.C.(ap) mm | Material | Vc m/min | Feed mm/tooth | Cutting Edge |
| Aluminum alloys | 300-3000 | ||||
| N ID5 | Chipboard, fiberboard and plastics | 2000-3000 | |||
| Copper alloys and brass | 500-1500 | ||||
| Aluminum>12% silicon | 250-1000 | 0.05-0.25 | Sharp | ||
| Aluminum | 300-3000 | ||||
| N ID8 | Chipboard, fiberboard and plastics MMC | 2000-3000 200-600 |
APCT 1003PDR-HM Inserts with 2 Helical Precision Ground Cutting Edges for High Accuracy Finishing
Dimensions
W 1 Rd° APMX INSL
BS RE S
Tough Hard Recommended
1 Machining Data
a f p z
| Designation | W1 | RE | INSL | S | APMX | BS | (mm) | (mm/t) | |||
| APCT 100302R-HM | 6.70 | 0.25 | 10.95 | 3.51 | 8.00 | 1.20 | • | 0.70-8.00 | 0.06-0.12 | ||
| APCT 100304R-HM | 6.70 | 0.45 | 10.95 | 3.51 | 8.00 | 1.20 | • | 0.90-8.00 | 0.07-0.12 | ||
| APCT 1003PDR-HM | 6.70 | 0.50 | 10.95 | 3.51 | 8.00 | 1.20 | • | • | 0.90-8.00 | 0.07-0.15 |
- For cutting speed recommendations, see pages 542-547
For tools, see pages: APK-FE (239) HM90 E90A-10 (24) HM90 E90A-M-10 (28) HM90 E90A-MM-10 (27) HM90 E90A-MM-10-JHP (27) HM90 F90AP-10 (200)
- HM90 F90AP-10-JHP (200)
APCR 1003PDFR-P Super Positive Insert with a Polished Rake for Machining Aluminum
Dimensions
W 1 Rd°
LE/APMX INSL
BS RE S
Tough Hard Recommended
1 Machining Data
a f p z
| Designation | W1 | INSL | S | RE | BS | APMX | (mm) | (mm/t) | ||
| APCR 1003PDFR-P | 6.70 | 11.20 | 3.76 | 0.50 | 1.20 | 8.00 | • | • | 0.90-8.00 | 0.07-0.25 |
- Super positive rake sharp ground helical cutting edge, for finishing on aluminum, stainless steel and high temperature alloys
For tools, see pages: APK-FE (239) HM90 E90A-10 (24) HM90 E90A-M-10 (28) HM90 E90A-MM-10 (27) HM90 E90A-MM-10-JHP (27) HM90 F90AP-10 (200)
- HM90 F90AP-10-JHP (200)