Каталог Iscar дисковые фрезы и фрезерные пластины 2022 - страница 132
Навигация
 Каталог Iscar крепление инструмента
 Каталог Iscar инструмент для обработки отверстий
 Каталог Iscar резьбонарезные фрезы
 Каталог Iscar инструмента для сверления
 Каталог Iscar решения для глубокого сверления
MILLING INSERTS
IC
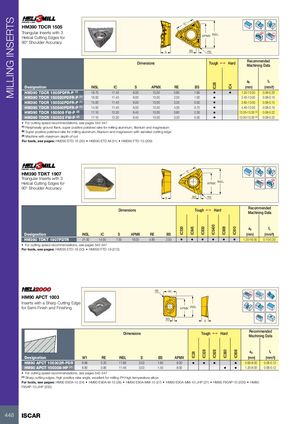
HM390 TDCR 1505
Triangular Inserts with 3 Rd°
APMX INSL
Helical Cutting Edges for
90° Shoulder Accuracy
S BS RE
Recommended
Dimensions Tough 1 Hard
Machining Data
ap fz
IC28
IC4
Designation INSL IC S APMX RE BS (mm) (mm/t)
HM390 TDCR 1505PDFR-P (1) 16.70 11.40 6.00 13.00 0.80 1.60 • • 1.20-13.00 0.08-0.20
HM390 TDCR 150520PDFR-P (1) 16.00 11.40 6.00 13.00 2.00 1.00 • 2.40-13.00 0.08-0.15
HM390 TDCR 150532PDFR-P (1) 15.00 11.40 6.00 13.00 3.20 0.50 • 3.60-13.00 0.08-0.15
HM390 TDCR 150540PDFR-P (1) 14.00 11.40 6.00 13.00 4.00 0.70 • 4.40-13.00 0.08-0.15
HM390 TDCR 150508 FW-P (2) 17.10 12.30 6.40 13.00 0.80 2.30 • 13.00-13.00 (3) 0.08-0.22
HM390 TDCR 150532 FW-P (2) 17.10 12.30 6.40 13.00 3.20 0.50 • 13.00-13.00 (3) 0.08-0.22
• For cutting speed recommendations, see pages 542-547
(1) Peripherally ground flank, super positive polished rake for milling aluminum, titanium and magnesium
(2) Super positive polished rake for milling aluminum, titanium and magnesium with serrated cutting edge
(3) Machine with maximum depth of cut
For tools, see pages: HM390 ETD-15 (30) • HM390 ETD-M (31) • HM390 FTD-15 (209)
IC
HM390 TDKT 1907
Triangular Inserts with 3 Rd°
INSL
Helical Cutting Edges for APMX
90° Shoulder Accuracy
S BS RE
Recommended
Dimensions Tough 1 Hard
IC5400 Machining Data
ap fz
IC330
IC845
IC830
IC808
Designation INSL IC S APMX RE BS IC810 (mm) (mm/t)
HM390 TDKT 1907PDTR 21.00 14.00 7.00 16.00 0.80 2.50 • • • • • • 1.20-16.00 0.10-0.20
• For cutting speed recommendations, see pages 542-547
For tools, see pages: HM390 ETD-19 (33) • HM390 FTD-19 (212)
RE W1 Rd°
HM90 APCT 1003
Inserts with a Sharp Cutting Edge
for Semi-Finish and Finishing APMX INSL
BS
S
Recommended
Dimensions Tough 1 Hard
Machining Data
ap fz
IC328
IC928
IC380
IC808
IC28
Designation W1 RE INSL S BS APMX (mm) (mm/t)
HM90 APCT 100302R-PDR 6.96 0.20 11.66 3.53 1.90 8.00 • • • • 0.60-8.00 0.06-0.12
HM90 APCT 100308-HP (1) 6.80 0.80 11.46 3.53 1.40 8.00 • • 1.20-8.00 0.06-0.12
• For cutting speed recommendations, see pages 542-547
(1) Sharp cutting edges, high positive rake angle, excellent for milling PH high temperature alloys
For tools, see pages: HM90 E90A-10 (24) • HM90 E90A-M-10 (28) • HM90 E90A-MM-10 (27) • HM90 E90A-MM-10-JHP (27) • HM90 F90AP-10 (200) • HM90
F90AP-10-JHP (200)
448 ISCAR
IC
HM390 TDCR 1505
Triangular Inserts with 3 Rd°
APMX INSL
Helical Cutting Edges for
90° Shoulder Accuracy
S BS RE
Recommended
Dimensions Tough 1 Hard
Machining Data
ap fz
IC28
IC4
Designation INSL IC S APMX RE BS (mm) (mm/t)
HM390 TDCR 1505PDFR-P (1) 16.70 11.40 6.00 13.00 0.80 1.60 • • 1.20-13.00 0.08-0.20
HM390 TDCR 150520PDFR-P (1) 16.00 11.40 6.00 13.00 2.00 1.00 • 2.40-13.00 0.08-0.15
HM390 TDCR 150532PDFR-P (1) 15.00 11.40 6.00 13.00 3.20 0.50 • 3.60-13.00 0.08-0.15
HM390 TDCR 150540PDFR-P (1) 14.00 11.40 6.00 13.00 4.00 0.70 • 4.40-13.00 0.08-0.15
HM390 TDCR 150508 FW-P (2) 17.10 12.30 6.40 13.00 0.80 2.30 • 13.00-13.00 (3) 0.08-0.22
HM390 TDCR 150532 FW-P (2) 17.10 12.30 6.40 13.00 3.20 0.50 • 13.00-13.00 (3) 0.08-0.22
• For cutting speed recommendations, see pages 542-547
(1) Peripherally ground flank, super positive polished rake for milling aluminum, titanium and magnesium
(2) Super positive polished rake for milling aluminum, titanium and magnesium with serrated cutting edge
(3) Machine with maximum depth of cut
For tools, see pages: HM390 ETD-15 (30) • HM390 ETD-M (31) • HM390 FTD-15 (209)
IC
HM390 TDKT 1907
Triangular Inserts with 3 Rd°
INSL
Helical Cutting Edges for APMX
90° Shoulder Accuracy
S BS RE
Recommended
Dimensions Tough 1 Hard
IC5400 Machining Data
ap fz
IC330
IC845
IC830
IC808
Designation INSL IC S APMX RE BS IC810 (mm) (mm/t)
HM390 TDKT 1907PDTR 21.00 14.00 7.00 16.00 0.80 2.50 • • • • • • 1.20-16.00 0.10-0.20
• For cutting speed recommendations, see pages 542-547
For tools, see pages: HM390 ETD-19 (33) • HM390 FTD-19 (212)
RE W1 Rd°
HM90 APCT 1003
Inserts with a Sharp Cutting Edge
for Semi-Finish and Finishing APMX INSL
BS
S
Recommended
Dimensions Tough 1 Hard
Machining Data
ap fz
IC328
IC928
IC380
IC808
IC28
Designation W1 RE INSL S BS APMX (mm) (mm/t)
HM90 APCT 100302R-PDR 6.96 0.20 11.66 3.53 1.90 8.00 • • • • 0.60-8.00 0.06-0.12
HM90 APCT 100308-HP (1) 6.80 0.80 11.46 3.53 1.40 8.00 • • 1.20-8.00 0.06-0.12
• For cutting speed recommendations, see pages 542-547
(1) Sharp cutting edges, high positive rake angle, excellent for milling PH high temperature alloys
For tools, see pages: HM90 E90A-10 (24) • HM90 E90A-M-10 (28) • HM90 E90A-MM-10 (27) • HM90 E90A-MM-10-JHP (27) • HM90 F90AP-10 (200) • HM90
F90AP-10-JHP (200)
448 ISCAR