Каталог Iscar дисковые фрезы и фрезерные пластины 2022 - страница 131
Навигация
 Каталог Iscar крепление инструмента
 Каталог Iscar инструмент для обработки отверстий
 Каталог Iscar резьбонарезные фрезы
 Каталог Iscar инструмента для сверления
 Каталог Iscar решения для глубокого сверления
MILLING INSERTS
IC
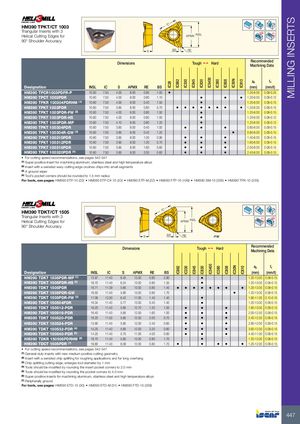
HM390 TPKT/CT 1003
Triangular Inserts with 3 Rd°
Helical Cutting Edges for APMX INSL
90° Shoulder Accuracy
S BS RE
Recommended
Dimensions Tough 1 Hard
Machining Data
IC5400
IC30N
ap fz
IC882
IC330
IC845
IC830
IC380
IC808
IC810
IC28
Designation INSL IC S APMX RE BS (mm) (mm/t)
HM390 TPCR1003PDFR-P 10.90 7.50 4.00 8.00 0.80 1.00 • 1.20-8.00 0.08-0.25
HM390 TPCT 1003PDR 10.90 7.50 4.00 8.00 0.80 1.10 • • • 1.20-8.00 0.08-0.12
HM390 TPKR 100304PDRHM (1) 10.90 7.50 4.00 8.00 0.40 1.50 • 1.20-8.00 0.08-0.15
HM390 TPKT 1003PDR 10.90 7.50 3.85 8.00 0.80 0.70 • • • • • • • • 1.20-8.00 0.08-0.15
HM390 TPKT 1003PDR-FW (2) 10.90 7.50 4.00 8.00 0.80 1.50 • 1.20-8.00 0.08-0.15
HM390 TPKT 1003PDR-HS 10.90 7.50 4.00 8.00 0.80 1.00 • 1.20-8.00 0.08-0.12
HM390 TPKT 1003PDR-MP 10.90 7.50 4.10 8.00 0.80 1.20 • 1.20-8.00 0.08-0.12
HM390 TPKT 100304PDR 10.90 7.50 3.85 8.00 0.40 1.00 • • • 0.80-8.00 0.08-0.15
HM390 TPKT 100304R-GW (3) 10.90 7.50 3.85 8.00 0.40 1.25 • 0.80-8.00 0.08-0.15
HM390 TPKT 100310PDR 10.90 7.50 3.85 8.00 1.00 0.90 • • • 1.40-8.00 0.08-0.15
HM390 TPKT 100312PDR 10.90 7.50 3.85 8.00 1.20 0.70 • • • 1.60-8.00 0.08-0.15
HM390 TPKT 100316PDR 10.90 7.50 3.85 8.00 1.60 0.60 • • • 2.00-8.00 0.08-0.15
HM390 TPKT 100320PDR (4) 10.90 7.50 3.85 8.00 2.00 0.60 • • • 2.40-8.00 0.08-0.15
• For cutting speed recommendations, see pages 542-547
(1) Super positive insert for machining aluminum, stainless steel and high temperature alloys
(2) Insert with a serrated wavy cutting edge crushes chips into small segments
(3) A ground wiper
(4) Tool's pocket corners should be rounded to 1.5 mm radius
For tools, see pages: HM390 ETP-10 (22) • HM390 ETP-C#-10 (23) • HM390 ETP-M (22) • HM390 FTP-10 (199) • HM390 SM-10 (236) • HM390 TPK-10 (235)
IC
HM390 TDKT/CT 1505
Triangular Inserts with 3 Rd°
Helical Cutting Edges for APMX INSL
90° Shoulder Accuracy
S BS RE -FW
Recommended
Dimensions Tough 1 Hard
Machining Data
ap fz
IC5400
IC30N
IC882
IC330
IC845
IC830
IC380
IC808
IC810
Designation INSL IC S APMX RE BS (mm) (mm/t)
HM390 TDKT 1505PDR-MP (1) 15.97 11.40 6.45 13.00 0.80 2.90 • 1.20-13.00 0.08-0.15
HM390 TDKT 1505PDR-HS (2) 16.70 11.40 6.24 13.00 0.80 1.35 • 1.20-13.00 0.08-0.15
HM390 TDKT 1505PDR 16.71 11.39 5.85 13.00 0.80 1.40 • • • • • • • • 1.20-13.00 0.08-0.15
HM390 TDKT 1505PDR-GW 16.50 11.40 5.80 13.00 0.80 1.70 • 1.20-13.00 0.08-0.15
HM390 TDKT 1505PDR-FW (3) 17.06 12.30 6.42 11.00 1.40 1.40 • 1.80-11.00 0.10-0.15
HM390 TDKT 150504PDR 16.34 11.40 5.77 13.00 0.40 1.40 • 1.20-13.00 0.08-0.15
HM390 TDKT 150512-PDR 16.20 11.40 5.85 12.70 1.20 1.00 • • • 1.60-13.00 0.08-0.15
HM390 TDKT 150516-PDR 16.40 11.40 5.85 12.50 1.60 1.00 • • • 2.00-12.50 0.08-0.15
HM390 TDKT 150520-PDR 16.20 11.50 5.85 12.50 2.00 0.70 • • • 2.40-12.50 0.08-0.15
HM390 TDKT 150524-PDR 15.90 11.40 5.85 12.00 2.40 0.60 • • • 2.80-12.00 0.08-0.15
HM390 TDKT 150532-PDR (4) 15.20 11.40 5.85 12.00 3.20 0.60 • • • 3.60-12.00 0.08-0.15
HM390 TDKT 150540-PDR (5) 14.25 11.40 5.75 11.00 4.00 0.60 • • • 4.40-11.00 0.08-0.15
HM390 TDKR 150508PDRHM (6) 16.70 11.40 5.85 13.00 0.80 1.70 • 1.20-13.00 0.08-0.15
HM390 TDCT 1505PDR (7) 16.80 11.40 6.08 12.00 0.80 1.70 • • • • • 1.20-12.00 0.08-0.15
• For cutting speed recommendations, see pages 542-547
(1) General-duty inserts with new medium positive cutting geometry
(2) Insert with a serrated chip splitting for roughing applications and for long overhang
(3) Chip splitting cutting edge, enlarges tool diameter by 1 mm
(4) Tools should be modified by rounding the insert pocket corners to 2.0 mm
(5) Tools should be modified by rounding the pocket corners to 4.0 mm
(6) Super positive inserts for machining aluminum, stainless steel and high temperature alloys
(7) Peripherally ground
For tools, see pages: HM390 ETD-15 (30) • HM390 ETD-M (31) • HM390 FTD-15 (209)
447
IC
HM390 TPKT/CT 1003
Triangular Inserts with 3 Rd°
Helical Cutting Edges for APMX INSL
90° Shoulder Accuracy
S BS RE
Recommended
Dimensions Tough 1 Hard
Machining Data
IC5400
IC30N
ap fz
IC882
IC330
IC845
IC830
IC380
IC808
IC810
IC28
Designation INSL IC S APMX RE BS (mm) (mm/t)
HM390 TPCR1003PDFR-P 10.90 7.50 4.00 8.00 0.80 1.00 • 1.20-8.00 0.08-0.25
HM390 TPCT 1003PDR 10.90 7.50 4.00 8.00 0.80 1.10 • • • 1.20-8.00 0.08-0.12
HM390 TPKR 100304PDRHM (1) 10.90 7.50 4.00 8.00 0.40 1.50 • 1.20-8.00 0.08-0.15
HM390 TPKT 1003PDR 10.90 7.50 3.85 8.00 0.80 0.70 • • • • • • • • 1.20-8.00 0.08-0.15
HM390 TPKT 1003PDR-FW (2) 10.90 7.50 4.00 8.00 0.80 1.50 • 1.20-8.00 0.08-0.15
HM390 TPKT 1003PDR-HS 10.90 7.50 4.00 8.00 0.80 1.00 • 1.20-8.00 0.08-0.12
HM390 TPKT 1003PDR-MP 10.90 7.50 4.10 8.00 0.80 1.20 • 1.20-8.00 0.08-0.12
HM390 TPKT 100304PDR 10.90 7.50 3.85 8.00 0.40 1.00 • • • 0.80-8.00 0.08-0.15
HM390 TPKT 100304R-GW (3) 10.90 7.50 3.85 8.00 0.40 1.25 • 0.80-8.00 0.08-0.15
HM390 TPKT 100310PDR 10.90 7.50 3.85 8.00 1.00 0.90 • • • 1.40-8.00 0.08-0.15
HM390 TPKT 100312PDR 10.90 7.50 3.85 8.00 1.20 0.70 • • • 1.60-8.00 0.08-0.15
HM390 TPKT 100316PDR 10.90 7.50 3.85 8.00 1.60 0.60 • • • 2.00-8.00 0.08-0.15
HM390 TPKT 100320PDR (4) 10.90 7.50 3.85 8.00 2.00 0.60 • • • 2.40-8.00 0.08-0.15
• For cutting speed recommendations, see pages 542-547
(1) Super positive insert for machining aluminum, stainless steel and high temperature alloys
(2) Insert with a serrated wavy cutting edge crushes chips into small segments
(3) A ground wiper
(4) Tool's pocket corners should be rounded to 1.5 mm radius
For tools, see pages: HM390 ETP-10 (22) • HM390 ETP-C#-10 (23) • HM390 ETP-M (22) • HM390 FTP-10 (199) • HM390 SM-10 (236) • HM390 TPK-10 (235)
IC
HM390 TDKT/CT 1505
Triangular Inserts with 3 Rd°
Helical Cutting Edges for APMX INSL
90° Shoulder Accuracy
S BS RE -FW
Recommended
Dimensions Tough 1 Hard
Machining Data
ap fz
IC5400
IC30N
IC882
IC330
IC845
IC830
IC380
IC808
IC810
Designation INSL IC S APMX RE BS (mm) (mm/t)
HM390 TDKT 1505PDR-MP (1) 15.97 11.40 6.45 13.00 0.80 2.90 • 1.20-13.00 0.08-0.15
HM390 TDKT 1505PDR-HS (2) 16.70 11.40 6.24 13.00 0.80 1.35 • 1.20-13.00 0.08-0.15
HM390 TDKT 1505PDR 16.71 11.39 5.85 13.00 0.80 1.40 • • • • • • • • 1.20-13.00 0.08-0.15
HM390 TDKT 1505PDR-GW 16.50 11.40 5.80 13.00 0.80 1.70 • 1.20-13.00 0.08-0.15
HM390 TDKT 1505PDR-FW (3) 17.06 12.30 6.42 11.00 1.40 1.40 • 1.80-11.00 0.10-0.15
HM390 TDKT 150504PDR 16.34 11.40 5.77 13.00 0.40 1.40 • 1.20-13.00 0.08-0.15
HM390 TDKT 150512-PDR 16.20 11.40 5.85 12.70 1.20 1.00 • • • 1.60-13.00 0.08-0.15
HM390 TDKT 150516-PDR 16.40 11.40 5.85 12.50 1.60 1.00 • • • 2.00-12.50 0.08-0.15
HM390 TDKT 150520-PDR 16.20 11.50 5.85 12.50 2.00 0.70 • • • 2.40-12.50 0.08-0.15
HM390 TDKT 150524-PDR 15.90 11.40 5.85 12.00 2.40 0.60 • • • 2.80-12.00 0.08-0.15
HM390 TDKT 150532-PDR (4) 15.20 11.40 5.85 12.00 3.20 0.60 • • • 3.60-12.00 0.08-0.15
HM390 TDKT 150540-PDR (5) 14.25 11.40 5.75 11.00 4.00 0.60 • • • 4.40-11.00 0.08-0.15
HM390 TDKR 150508PDRHM (6) 16.70 11.40 5.85 13.00 0.80 1.70 • 1.20-13.00 0.08-0.15
HM390 TDCT 1505PDR (7) 16.80 11.40 6.08 12.00 0.80 1.70 • • • • • 1.20-12.00 0.08-0.15
• For cutting speed recommendations, see pages 542-547
(1) General-duty inserts with new medium positive cutting geometry
(2) Insert with a serrated chip splitting for roughing applications and for long overhang
(3) Chip splitting cutting edge, enlarges tool diameter by 1 mm
(4) Tools should be modified by rounding the insert pocket corners to 2.0 mm
(5) Tools should be modified by rounding the pocket corners to 4.0 mm
(6) Super positive inserts for machining aluminum, stainless steel and high temperature alloys
(7) Peripherally ground
For tools, see pages: HM390 ETD-15 (30) • HM390 ETD-M (31) • HM390 FTD-15 (209)
447