Каталог Iscar дисковые фрезы и фрезерные пластины 2022 - страница 121
Навигация
 Каталог Iscar крепление инструмента
 Каталог Iscar инструмент для обработки отверстий
 Каталог Iscar резьбонарезные фрезы
 Каталог Iscar инструмента для сверления
 Каталог Iscar решения для глубокого сверления
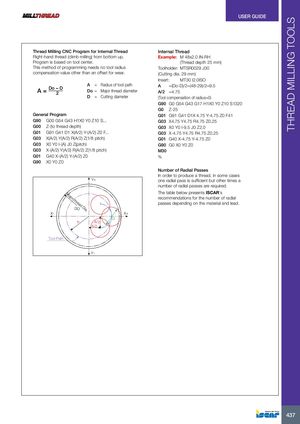
Thread Milling CNC Program for Internal Thread Internal Thread
| Right-hand thread (climb milling) from bottom up. | Example: | M 48x2.0 IN-RH |
| Program is based on tool center. | (Thread depth 25 mm) | |
| This method of programming needs no tool radius | Toolholder: MTSR0029 J30 | |
| compensation value other than an offset for wear. | (Cutting dia. 29 mm) | |
| Insert: | MT30 I2.0ISO |
| A | = Radius of tool path A | =(Do-D)/2=(48-29)/2=9.5 | ||
| A = Do – D | ||||
| 2 Do = Major thread diameter | A/2 | =4.75 | ||
| D | = Cutting diameter (Tool compensation of radius=0) | |||
| G90 | G0 G54 G43 G17 H1X0 Y0 Z10 S1320 | |||
| G0 | Z-25 | |||
| General Program | G01 | G91 G41 D1X 4.75 Y-4.75 Z0 F41 | ||
| G90 | G00 G54 G43 H1X0 Y0 Z10 S... | G03 X4.75 Y4.75 R4.75 Z0.25 | ||
| G00 | Z-(to thread depth) | G03 | X0 Y0 I-9.5 J0 Z2.0 | |
| G01 | G91 G41 D1 X(A/2) Y-(A/2) Z0 F... | G03 | X-4.75 Y4.75 R4.75 Z0.25 | |
| G03 | X(A/2) Y(A/2) R(A/2) Z(1/8 pitch) | G01 | G40 X-4.75 Y-4.75 Z0 | |
| G03 | X0 Y0 I-(A) J0 Z(pitch) | G90 | G0 X0 Y0 Z0 | |
| G03 | X-(A/2) Y(A/2) R(A/2) Z(1/8 pitch) | M30 | ||
| G01 | G40 X-(A/2) Y-(A/2) Z0 | % |
G90 X0 Y0 Z0 Number of Radial Passes In order to produce a thread, in some cases Y+ one radial pass is sufficient but other times a
number of radial passes are required. Major thread Dia. The table below presents ISCAR's recommendations for the number of radial passes depending on the material and lead. DO X- X+ D A A/2 A/2
Tool Path
Y-