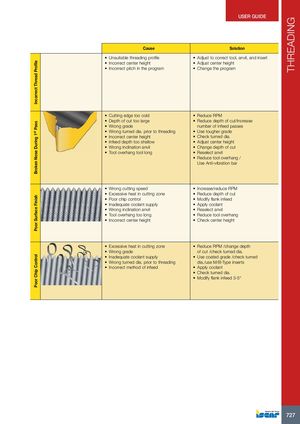
| Incorrect Thread Profile | Cause • Unsuitable threading profile • Incorrect center height • Incorrect pitch in the program | Solution • Adjust to correct tool, anvil, and insert • Adjust center height • Change the program |
| Broken Nose During 1st Pass | • Cutting edge too cold • Depth of cut too large • Wrong grade • Wrong turned dia. prior to threading • Incorrect center height • Infeed depth too shallow • Wrong inclination anvil • Tool overhang tool long | • Reduce RPM • Reduce depth of cut/Increase number of infeed passes • Use tougher grade • Check turned dia. • Adjust center height • Change depth of cut • Reselect anvil • Reduce tool overhang / Use Anti-vibration bar |
| Poor Surface Finish | • Wrong cutting speed • Excessive heat in cutting zone • Poor chip control • Inadequate coolant supply • Wrong inclination anvil • Tool overhang too long • Incorrect center height | • Increase/reduce RPM • Reduce depth of cut • Modify flank infeed • Apply coolant • Reselect anvil • Reduce tool overhang • Check center height |
| Poor Chip Control | • Excessive heat in cutting zone • Wrong grade • Inadequate coolant supply • Wrong turned dia. prior to threading • Incorrect method of infeed | • Reduce RPM /change depth of cut /check turned dia. • Use coated grade /check turned dia./use M/B-Type inserts • Apply coolant • Check turned dia. • Modify flank infeed 3-5° |
 Каталог Iscar сверла со сменной режущей частью 2022
 Каталог Iscar новые продукты 2018
 Каталог Iscar концевые фрезы со сменными пластинами 2022
 Каталог Iscar инструмент для нарезания резьбы
 Каталог Iscar отрезка 2022
 Каталог Iscar торцевые фрезы 2022