Каталог Guhring сверла со сменными пластинами - страница 37
Навигация
 Каталог Guhring пластины PKD и CBN
 Основной каталог Guhring 2011
 Каталог Guhring резьбонарезной инструмент
 Каталог Guhring зенкеры и зенковки
 Каталог Guhring резьбонарезной инструмент 2010
 Каталог Guhring высокопроизводительный инструмент по отличной цене SuperLine
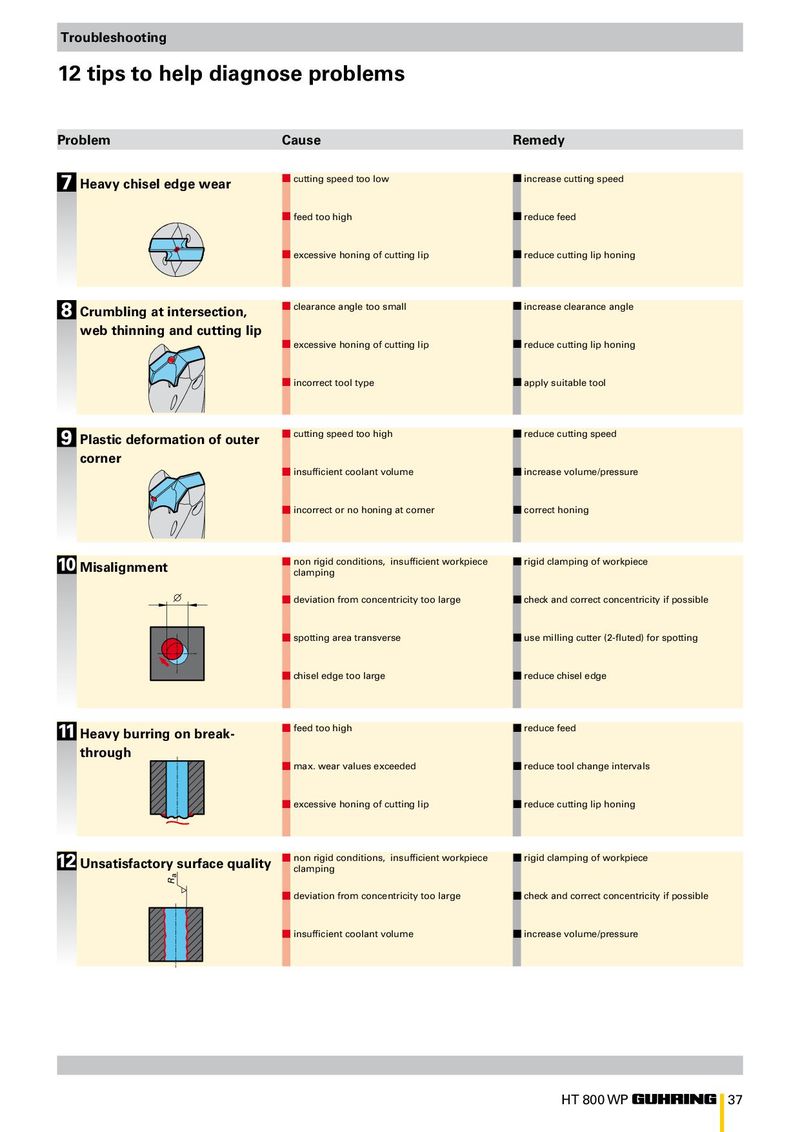
Troubleshooting
12 tips to help diagnose problems
| Problem | Cause | Remedy | |
| Heavy chisel edge wear | cutting speed too low | increase cutting speed |
- feed too high
- reduce feed
- excessive honing of cutting lip
- reduce cutting lip honing
Crumbling at intersection, clearance angle too small increase clearance angle
web thinning and cutting lip
- excessive honing of cutting lip
- reduce cutting lip honing
- incorrect tool type
- apply suitable tool
Plastic deformation of outer cutting speed too high reduce cutting speed
corner
- insufficient coolant volume
- increase volume/pressure
- incorrect or no honing at corner
- correct honing
Misalignment non rigid conditions, insufficient workpiece rigid clamping of workpiece
clamping
- deviation from concentricity too large
- check and correct concentricity if possible
- spotting area transverse
- use milling cutter (2-fluted) for spotting
- chisel edge too large
- reduce chisel edge
Heavy burring on break- feed too high reduce feed
through
- max. wear values exceeded
- reduce tool change intervals
- excessive honing of cutting lip
- reduce cutting lip honing
Unsatisfactory surface quality non rigid conditions, insufficient workpiece rigid clamping of workpiece
clamping
- deviation from concentricity too large
- check and correct concentricity if possible
- insufficient coolant volume
- increase volume/pressure