Общий каталог Dijet 2018 - страница 76
Навигация
 Общий каталог Dijet 2012 на русском
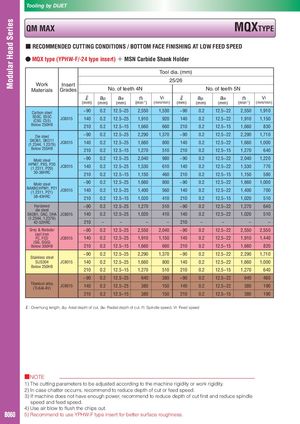
■ RECOMMENDED CUTTING CONDITIONS / BOTTOM FACE FINISHING AT LOW FEED SPEED
- MQX type (YPHW-F/-24 type insert) + MSN Carbide Shank Holder
| Work | Insert | Tool d 25 | ia.(mm) /26 | ||||||||
| Materials | Grades | No. of teet | h4N | N | o. of teeth | 5N | |||||
| ℓ (mm) | ap (mm) | ae (mm) | n (min-1) | Vf (mm/min) | ℓ (mm) | ap (mm) | ae (mm) | n (min-1) | Vf (mm/min) | ||
| Carbon steel | ~90 | 0.2 | 12.5~25 | 2,550 | 1,530 | ~90 | 0.2 | 12.5~22 | 2,550 | 1,910 | |
| S50C, S55C (C50, C55) | JC8015 | 140 | 0.2 | 12.5~25 | 1,910 | 920 | 140 | 0.2 | 12.5~22 | 1,910 | 1,150 |
| Below 250HB | 210 | 0.2 | 12.5~15 | 1,660 | 660 | 210 | 0.2 | 12.5~15 | 1,660 | 830 | |
| Die steel | ~90 | 0.2 | 12.5~25 | 2,290 | 1,370 | ~90 | 0.2 | 12.5~22 | 2,290 | 1,710 | |
| SKD61, SKD11 (1.2344, 1.2379) | JC8015 | 140 | 0.2 | 12.5~25 | 1,660 | 800 | 140 | 0.2 | 12.5~22 | 1,660 | 1,000 |
| Below 255HB | 210 | 0.2 | 12.5~15 | 1,270 | 510 | 210 | 0.2 | 12.5~15 | 1,270 | 640 | |
| Mold steel | ~90 | 0.2 | 12.5~25 | 2,040 | 980 | ~90 | 0.2 | 12.5~22 | 2,040 | 1,220 | |
| HPM7, PX5, P20 (1.2311, P20) | JC8015 | 140 | 0.2 | 12.5~25 | 1,530 | 610 | 140 | 0.2 | 12.5~22 | 1,530 | 770 |
| 30-36HRC | 210 | 0.2 | 12.5~15 | 1,150 | 460 | 210 | 0.2 | 12.5~15 | 1,150 | 580 | |
| Mold steel | ~90 | 0.2 | 12.5~25 | 1,660 | 800 | ~90 | 0.2 | 12.5~22 | 1,660 | 1,000 | |
| NAK80,HPM1, P21 (1.2311, P21) | JC8015 | 140 | 0.2 | 12.5~25 | 1,400 | 560 | 140 | 0.2 | 12.5~22 | 1,400 | 700 |
| 38-43HRC | 210 | 0.2 | 12.5~15 | 1,020 | 410 | 210 | 0.2 | 12.5~15 | 1,020 | 510 | |
| Hardened di tl | ~90 | 0.2 | 12.5~25 | 1,270 | 510 | ~90 | 0.2 | 12.5~22 | 1,270 | 640 | |
| e see SKD61, DAC, DHA (12344 12379) | JC8015 | 140 | 0.2 | 12.5~25 | 1,020 | 410 | 140 | 0.2 | 12.5~22 | 1,020 | 510 |
| ., . 42-52HRC | 210 | – | – | – | – | 210 | – | – | – | – | |
| Grey & Nodular t i | ~90 | 0.2 | 12.5~25 | 2,550 | 2,040 | ~90 | 0.2 | 12.5~22 | 2,550 | 2,550 | |
| cas ron FC, FCD | JC8015 | 140 | 0.2 | 12.5~25 | 1,910 | 1,150 | 140 | 0.2 | 12.5~22 | 1,910 | 1,440 |
| (GG, GGG) Below 300HB | 210 | 0.2 | 12.5~15 | 1,660 | 660 | 210 | 0.2 | 12.5~15 | 1,660 | 820 | |
| Stainless steel | ~90 | 0.2 | 12.5~25 | 2,290 | 1,370 | ~90 | 0.2 | 12.5~22 | 2,290 | 1,710 | |
| SUS304 | JC8015 | 140 | 0.2 | 12.5~25 | 1,660 | 800 | 140 | 0.2 | 12.5~22 | 1,660 | 1,000 |
| Below 250HB | 210 | 0.2 | 12.5~15 | 1,270 | 510 | 210 | 0.2 | 12.5~15 | 1,270 | 640 | |
| ~90 | 0.2 | 12.5~25 | 640 | 380 | ~90 | 0.2 | 12.5~22 | 640 | 480 | ||
| Titanium alloy (Ti-6Al-4V) | JC8015 | 140 | 0.2 | 12.5~25 | 380 | 150 | 140 | 0.2 | 12.5~22 | 380 | 190 |
| 210 | 0.2 | 12.5~15 | 380 | 150 | 210 | 0.2 | 12.5~15 | 380 | 190 |
ℓ: Overhung length, a Axial depth of cut, a : Radial depth of cut, n: Spindle speed, V : Feed speed
p: e f
■NOTE
B060 5) Recommend to use YPHW-F type insert for better surface roughness.