Каталог ZCC-CT фрезы монолитные - страница 167
Навигация
 Каталог ZCC-CT оснастка
 Каталог ZCC-CT фрезы со сменными пластинами
 Каталог ZCC-CT сверла со сменными пластинами
 Каталог ZCC-CT токарная обработка
 Каталог ZCC-CT сверла монолитные
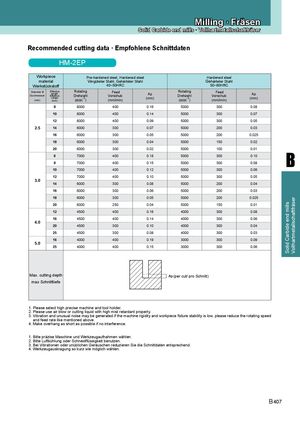
Recommended cutting data · Empfohlene Schnittdaten
HM-2EP
| Work mat Werkstü | piece erial ckstoff | Pre-ha Vergü | rdened steel,Hard 40~50HRC teter Stahl, Gehärt | ened steel eter Stahl | Hardened steel 50~60HRC Gehärteter Stahl | ||
| Diameter Ø | Effective lth | Rotating | Feed | Rotating | Feed | ||
| Durchmesser | eng Effektive Lä | Drehzahl | Vorschub | Ap | Drehzahl | Vorschub | Ap |
| (mm) | (mm) nge | (min-1) | (mm/min) | (mm) | (min-1) | (mm/min) | (mm) |
| 8 | 8000 | 400 | 0.16 | 5000 | 300 | 0.08 | |
| 10 | 8000 | 400 | 0.14 | 5000 | 300 | 0.07 | |
| 12 | 8000 | 400 | 0.09 | 5000 | 300 | 0.05 | |
| 2.5 | 14 | 6000 | 300 | 0.07 | 5000 | 200 | 0.03 |
| 16 | 6000 | 300 | 0.05 | 5000 | 200 | 0.025 | |
| 18 | 6000 | 300 | 0.04 | 5000 | 150 | 0.02 | |
| 20 | 6000 | 300 | 0.02 | 5000 | 100 | 0.01 | |
| 6 | 7000 | 400 | 0.18 | 5000 | 300 | 0.10 | |
| 8 | 7000 | 400 | 0.15 | 5000 | 300 | 0.08 | |
| 10 | 7000 | 400 | 0.12 | 5000 | 300 | 0.06 | |
| 30 | 12 | 7000 | 400 | 0.10 | 5000 | 300 | 0.05 |
| . | 14 | 6000 | 300 | 0.08 | 5000 | 200 | 0.04 |
| 16 | 6000 | 300 | 0.06 | 5000 | 200 | 0.03 | |
| 18 | 6000 | 300 | 0.05 | 5000 | 200 | 0.025 | |
| 20 | 6000 | 250 | 0.04 | 5000 | 150 | 0.01 | |
| 12 | 4500 | 400 | 0.16 | 4000 | 300 | 0.08 | |
| 40 | 16 | 4500 | 400 | 0.14 | 4000 | 300 | 0.06 |
| . | 20 | 4500 | 300 | 0.10 | 4000 | 300 | 0.04 |
| 25 | 4500 | 300 | 0.08 | 4000 | 300 | 0.03 | |
| 50 | 16 | 4000 | 400 | 0.19 | 3000 | 300 | 0.09 |
| . | 25 | 4000 | 400 | 0.15 | 3000 | 300 | 0.06 |
| Max. cutti max Sch | ng depth nitttiefe | (per cut/ pro S | chnitt) |
1. Please select high precise machine and tool holder. 2. Please use air blow or cutting liquid with high mist retardant property. 3. Vibration and unusual noise may be generated if the machine rigidity and workpiece fixture stability is low, please reduce the rotating speed and feed rate like mentioned above. 4. Make overhang as short as possible if no interference. 1. Bitte präzise Maschine und Werkzeugaufnahmen wählen. 2. Bitte Luftkühlung oder Schneidflüssigkeit benutzen. 3. Bei Vibrationen oder unüblichen Geräuschen reduzieren Sie die Schnittdaten entsprechend. 4. Werkzeugauskragung so kurz wie möglich wählen.