Общий каталог Yamawa 2021 - страница 703
Навигация
 Обший каталог Yamawa 2016 - 2017
 Краткое руководство Yamawa по каталогам
 Общий каталог Yamawa 2022 - 2023
 Каталоги Yamawa твердосплавные метчики для закаленной стали
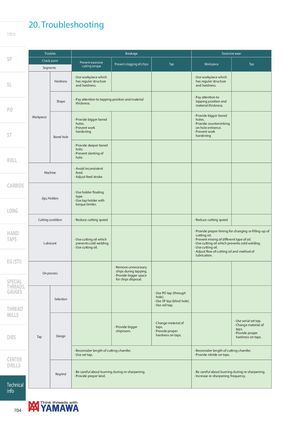
| Troubles Check point Segments | Prevent excessive cutting torque | Breakage Prevent clogging of chips | Tap | Excessiv Workpiece | e wear Tap |
| Hardness | ∙ Use workpiece which has regular structure and hardness. | ∙ Use workpiece which has regular structure and hardness. | |||
| Shape | ∙ Pay attention to tapping thickness. | position and material | ∙ Pay attention to tapping position and material thickness. | ||
| Workpiece Bored hole | ∙ Provide bigger bored holes. ∙ Prevent work hardening. | ∙ Provide bigger bored holes. ∙ Provide countersinking on hole entrance. ∙ Prevent work hardening | |||
| ∙ Provide deeper bored hole. ∙ Prevent slanting of hole. | |||||
| Machine | ∙ Avoid inconsistent feed. ∙ Adjust feed stroke | ||||
| Jigs, Holders | ∙ Use holder fl oating type. ∙ Use tap holder with torque limiter. | ||||
| Cutting condition | ∙ Reduce cutting speed | ∙ Reduce cutting speed | |||
| Lubricant | ∙ Use cutting oil which prevents cold welding. ∙ Use cutting oil. | ∙ Provide proper timing for i cutting oil. ∙ Prevent mixing of diff ere ∙ Use cutting oil which pre ∙ Use cutting oil. ∙ Adjust fl ow of cutting oil lubrication. | changing or fi lling-up of f nt type of oil. vents cold welding. l and method of | ||
| On process | ∙ Remove unnecessary chips during tapping. ∙ Provide bigger space for chips disposal. | ||||
| Selection | ∙ Use PO tap (through hole). ∙ Use SP tap (blind hole). ∙ Use roll tap. | ||||
| Tap Design | ∙ Provide bigger chiproom. | ∙ Change material of taps. ∙ Provide proper hardness on taps. | ∙ Use serial set tap. ∙ Change material of taps. ∙ Provide proper hardness on taps. | ||
| ∙ Reconsider length of cutt ∙ Use set tap. | ing chamfer. | ∙ Reconsider length of cutt ∙ Provide nitride on taps. | ing chamfer. | ||
| Regrind | ∙ Be careful about burning ∙ Provide proper land. | during re-sharpening. | ∙ Be careful about burning ∙ Increase re-sharpening fr | during re-sharpening. equency. |
SP
PO
CARBIDE
LONG
EG (STI)
THREADS,