Общий каталог Yamawa 2021 - страница 623
Навигация
 Обший каталог Yamawa 2016 - 2017
 Краткое руководство Yamawa по каталогам
 Общий каталог Yamawa 2022 - 2023
 Каталоги Yamawa твердосплавные метчики для закаленной стали
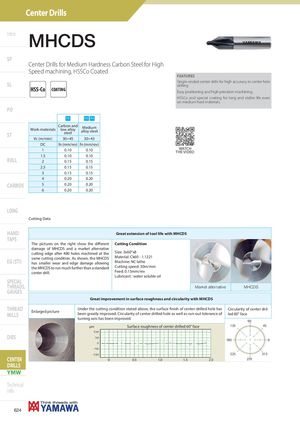
Intro MHCDS
SP
Center Drills for Medium Hardness Carbon Steel for High
Speed machining, HSSCo Coated
SL
HSS-Co COATING
PO
FEATURES Single-ended center drills for high accuracy in center hole drilling. Easy positioning and high precision machining. HSSCo and special coating for long and stable life even on medium hard materials.
| P2 | P3 P4 | |
| Work-materials | Carbon and low alloy steel | Medium alloy steel |
| Vc(m/min) | 30÷45 | 30÷45 |
| DC | fn(mm/rev) | fn(mm/rev) |
| 1 | 0.10 | 0.10 |
| 1.5 | 0.10 | 0.10 |
| 2 | 0.15 | 0.15 |
| 2.5 | 0.15 | 0.15 |
| 3 | 0.15 | 0.15 |
| 4 | 0.20 | 0.20 |
| 5 | 0.20 | 0.20 |
| 6 | 0.20 | 0.20 |
THE VIDEO
LONG
Cutting Data
| HAND | Great extension of tool life with MHCDS | |
| TAPS | ||
| The pictures on the right show the diff erent | Cutting Condition | |
| damage of MHCDS and a market alternative | ||
| cutting edge after 480 holes machined at the | Size: 3x60°x8 | |
| same cutting condition. As shown, the MHCDS | Material: Ck60 - 1.1221 | |
| EG (STI) | Machine: NC lathe | |
| has smaller wear and edge damage allowing | ||
| the MHCDS to run much further than a standard | Cutting speed: 30m/min | |
| center drill. | Feed: 0.15mm/rev | |
| Lubricant : water soluble oil | ||
| SPECIAL | ||
| THREADS, | MHCDS Market alternative | |
| GAUGES | ||
| Great improvement in surface roughness and circularity with MHCDS |
| THREAD | Under the cutting condition stated above, the surface fi nish of center-drilled hole has | Circularity of center dril- | ||
| Enlarged picture | ||||
| MILLS | been greatly improved. Circularity of center drilled hole as well as run-out tolerance of | led 60° face | ||
| turning axis has been improved. | ||||
| 90 |
μm Surface roughness of center drilled 60° face 135 45
DIES 180 0
225 315
CENTER 0 0.5 1.0 1.5 2.0 270
DRILLS YMW