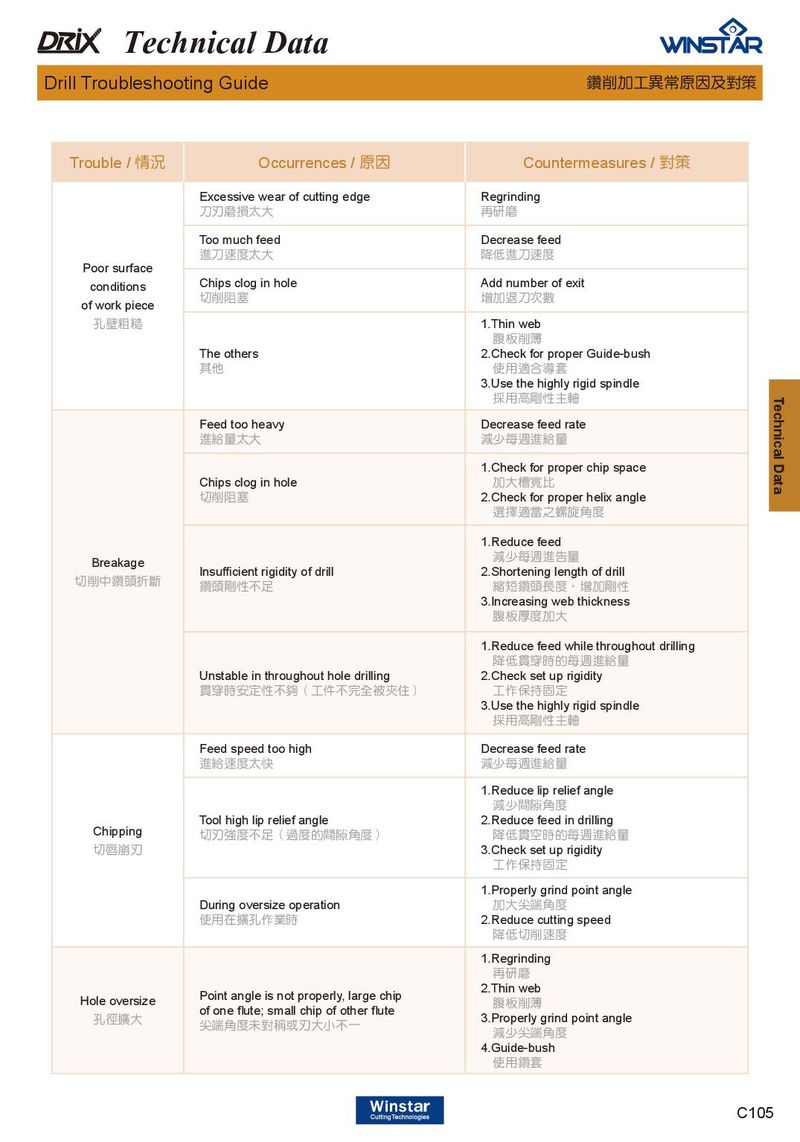
| Trouble /情況 | Occurrences /原因 | Countermeasures /對策 |
| Excessive wear of cutting edge 刀刃磨損太大 | Regrinding 再研磨 |
| Poor surface | Too much feed 進刀速度太大 | Decrease feed 降低進刀速度 |
| conditions of work piece | Chips clog in hole 切削阻塞 | Add number of exit 增加退刀次數 |
| 孔壁粗糙 | | 1.Thin web 腹板削薄 |
| The others 其他 | 2.Check for proper Guide-bush 使用適合導套 3.Use the highly rigid spindle 採用高剛性主軸 |
| Feed too heavy 進給量太大 | Decrease feed rate 減少每週進給量 |
| Chips clog in hole 切削阻塞 | 1.Check for proper chip space 加大槽寬比 2.Check for proper helix angle 選擇適當之螺旋角度 |
| Breakage 切削中鑽頭折斷 | Insufficient rigidity of drill 鑽頭剛性不足 | 1.Reduce feed 減少每週進告量 2.Shortening length of drill 縮短鑽頭長度,增加剛性 3.Increasing web thickness 腹板厚度加大 |
| Unstable in throughout hole drilling 貫穿時安定性不夠( 工件不完全被夾住) | 1.Reduce feed while throughout drilling 降低貫穿時的每週進給量 2.Check set up rigidity 工作保持固定 3.Use the highly rigid spindle 採用高剛性主軸 |
| Feed speed too high 進給速度太快 | Decrease feed rate 減少每週進給量 |
| | 1.Reduce lip relief angle 減少間隙角度 |
| Chipping 切唇崩刃 | Tool high lip relief angle 切刃強度不足( 過度的間隙角度) | 2.Reduce feed in drilling 降低貫空時的每週進給量 3.Check set up rigidity 工作保持固定 |
| During oversize operation 使用在擴孔作業時 | 1.Properly grind point angle 加大尖端角度 2.Reduce cutting speed 降低切削速度 |
| | 1.Regrinding 再研磨 |
| Hole oversize 孔徑擴大 | Point angle is not properly, large chip of one flute; small chip of other flute 尖端角度未對稱或刃大小不一 | 2.Thin web 腹板削薄 3.Properly grind point angle 減少尖端角度 4.Guide-bush 使用鑽套 |
 Каталог Winstar инструмент со сменными пластинами 2020
 Брошюра Winstar основная номенклатура 2021
 Основной каталог Winstar 2021
 Общий каталог Winstar 2015 - 2016
 Брошюра Winstar пластины 2021
 Каталог Winstar твердосплавные пластины и вставки