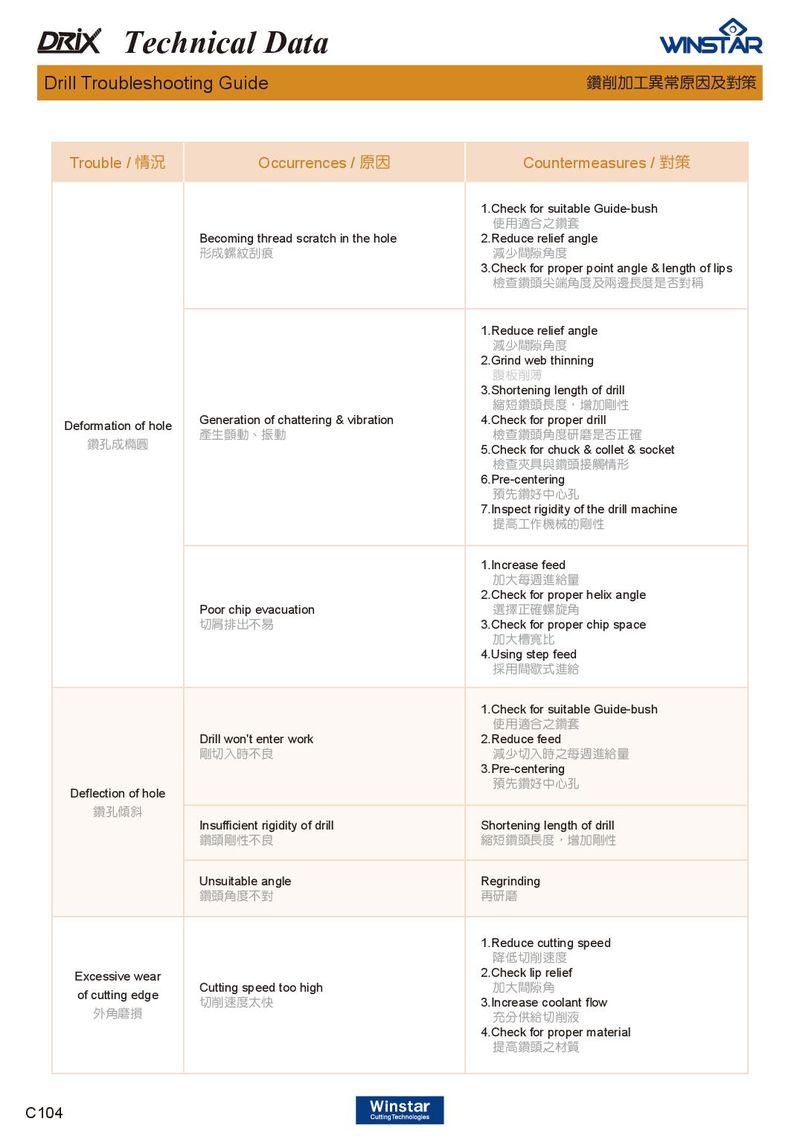
| Trouble /情況 | Occurrences /原因 | Countermeasures /對策 |
| Becoming thread scratch in the hole 形成螺紋刮痕 | 1.Check for suitable Guide-bush 使用適合之鑽套 2.Reduce relief angle 減少間隙角度 3.Check for proper point angle & length of lips 檢查鑽頭尖端角度及兩邊長度是否對稱 |
| | 1.Reduce relief angle 減少間隙角度 2.Grind web thinning 腹板削薄 3.Shortening length of drill 縮短鑽頭長度,增加剛性 |
| Deformation of hole 鑽孔成橢圓 | Generation of chattering & vibration 產生顫動、振動 | 4.Check for proper drill 檢查鑽頭角度研磨是否正確 5.Check for chuck & collet & socket 檢查夾具與鑽頭接觸情形 6.Pre-centering 預先鑽好中心孔 7.Inspect rigidity of the drill machine 提高工作機械的剛性 |
| Poor chip evacuation 切屑排出不易 | 1.Increase feed 加大每週進給量 2.Check for proper helix angle 選擇正確螺旋角 3.Check for proper chip space 加大槽寬比 4.Using step feed 採用間歇式進給 |
| Deflection of hole 鑽孔傾斜 | Drill won't enter work 剛切入時不良 Insufficient rigidity of drill 鑽頭剛性不良 | 1.Check for suitable Guide-bush 使用適合之鑽套 2.Reduce feed 減少切入時之每週進給量 3.Pre-centering 預先鑽好中心孔 Shortening length of drill 縮短鑽頭長度,增加剛性 |
| Unsuitable angle 鑽頭角度不對 | Regrinding 再研磨 |
| | 1.Reduce cutting speed 降低切削速度 |
| Excessive wear of cutting edge 外角磨損 | Cutting speed too high 切削速度太快 | 2.Check lip relief 加大間隙角 3.Increase coolant flow 充分供給切削液 |
| | 4.Check for proper material 提高鑽頭之材質 |
 Каталог Winstar инструмент со сменными пластинами 2020
 Брошюра Winstar основная номенклатура 2021
 Основной каталог Winstar 2021
 Общий каталог Winstar 2015 - 2016
 Брошюра Winstar пластины 2021
 Каталог Winstar твердосплавные пластины и вставки