Общий каталог Widia 2017 - страница 605
Навигация
 Каталог Widia токарный инструмент 2017
 Каталог Widia трохоидальное фрезерование
 Каталог Widia техническое руководство по разверткам
 Каталог Widia фрезы со сменными пластинами 2016
 Каталог Widia достижения 2020
- Table of Contents
- Turning
- Turning • ISO Inserts
- Turning • Tools for External Turning and Internal Boring
- Turning • Tools for External Turning and Internal Boring
- Turning • Tools for Small Hole Boring
- com E1Turning • Grooving and Cut-Off
- Turning • Threading
- Indexable Milling
- Indexable Milling • Face Mills
- Indexable Milling • Chamfer Mills
- Indexable Milling • 90° Shoulder Mills
- Indexable Milling • Helical Mills
- Indexable Milling • Slotting Mills
- Indexable Milling • Copy Mills
- Solid End Milling
- Solid End Milling • High-Performance Solid Carbide End Mills
- Solid End Milling • General Purpose Solid Carbide End Mills
- Solid End Milling • High-Performance High-Speed Steel (HSS-E/PM)
- Solid End Milling • Burs
- Holemaking
- Holemaking • High-Performance Solid Carbide Drills
- Holemaking • Modular Drills
- Holemaking • Indexable Drills
- Holemaking • Modular Drills
- Holemaking • Indexable Drills
- Holemaking • Hole Finishing
- Tapping
- Tapping Portfolio
- Index by Order Number
- Index by Catalogue Number
- Global Contacts
- Informational Icons Guide
- Material Overview • DIN
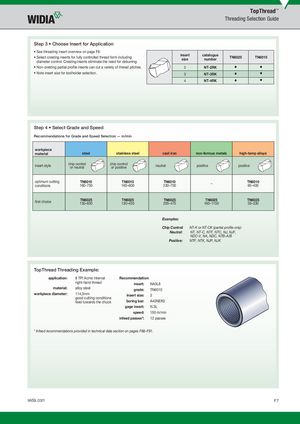
Threading Selection Guide
| • Select cresting inserts for fully controlled thread form including diameter control. Cresting inserts eliminate the need for deburring. | insert size | catalogue number | TN6025 | TN6010 |
| • Non-cresting partial profi le inserts can cut a variety of thread pitches. | 2 | NT-2RK | � | � |
| • Note insert size for toolholder selection. | 3 4 | NT-3RK NT-4RK | � � | � � |
4 NT-4RK
Step 4 Select Grade and Speed
Recommendations for Grade and Speed Selection — m/min
workpiece
material steel stainless steel cast iron non-ferrous metals high-temp alloys
chip control chip control
insert style neutral positive positive
or neutral or positive
| optimum cutting | TN6010 | TN6010 | TN6010 | TN6010 |
| conditions | 160–750 | 160–600 | 230–700 | 65–400 |
| TN6025 | TN6025 | TN6025 | TN6025 | TN6025 | |
| fi rst choice | |||||
| 130–650 | 130–450 | 200–475 | 160–1150 | 35–330 |
Examples:
Chip Control: NT-K or NT-CK (partial profi le only)
Neutral: NT, NT-C, NTF, NTC, NJ, NJF, NDC-V, NA, NDC, NTB-A/B
Positive: NTP, NTK, NJP, NJK
TopThread Threading Example:
| application: | 8 TPI Acme internal | Recommendation: | ||
| right-hand thread | insert: NA3L8 | |||
| material: alloy steel | grade: TN6010 |
workpiece diameter: 114,3mm insert size: 3
good cutting conditions feed towards the chuck boring bar: A40NER3 gage insert: N.3L speed: 150 m/min
infeed passes*: 12 passes
* Infeed recommendations provided in technical data section on pages F88–F91.