Общий каталог Widia 2017 - страница 1700
Навигация
 Каталог Widia токарный инструмент 2017
 Каталог Widia трохоидальное фрезерование
 Каталог Widia техническое руководство по разверткам
 Каталог Widia фрезы со сменными пластинами 2016
 Каталог Widia достижения 2020
- Table of Contents
- Turning
- Turning • ISO Inserts
- Turning • Tools for External Turning and Internal Boring
- Turning • Tools for External Turning and Internal Boring
- Turning • Tools for Small Hole Boring
- com E1Turning • Grooving and Cut-Off
- Turning • Threading
- Indexable Milling
- Indexable Milling • Face Mills
- Indexable Milling • Chamfer Mills
- Indexable Milling • 90° Shoulder Mills
- Indexable Milling • Helical Mills
- Indexable Milling • Slotting Mills
- Indexable Milling • Copy Mills
- Solid End Milling
- Solid End Milling • High-Performance Solid Carbide End Mills
- Solid End Milling • General Purpose Solid Carbide End Mills
- Solid End Milling • High-Performance High-Speed Steel (HSS-E/PM)
- Solid End Milling • Burs
- Holemaking
- Holemaking • High-Performance Solid Carbide Drills
- Holemaking • Modular Drills
- Holemaking • Indexable Drills
- Holemaking • Modular Drills
- Holemaking • Indexable Drills
- Holemaking • Hole Finishing
- Tapping
- Tapping Portfolio
- Index by Order Number
- Index by Catalogue Number
- Global Contacts
- Informational Icons Guide
- Material Overview • DIN
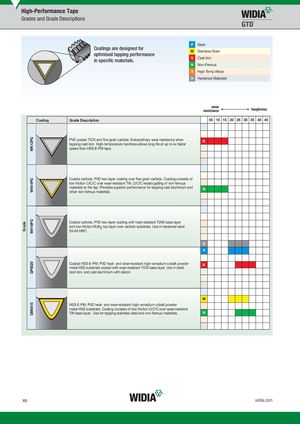
Coatings are designed for
optimised tapping performance
in specifi c materials .
| P | Steel |
| M | Stainless Steel |
| K | Cast Iron |
| N | Non-Ferrous |
| S | High-Temp Alloys |
| H | Hardened Materials |
wear toughness resistance
Coating Grade Description 05 10 15 20 25 30 35 40 45
PVD coated TiCN and fi ne grain carbide. Extraordinary wear resistance when K tapping cast iron. High-temperature hardness allows long life at up to 4x faster speed than HSS-E-PM taps.
Coated carbide, PVD two-layer coating over fi ne-grain carbide. Coating consists of low friction CrC/C over wear-resistant TiN. CrC/C resists galling of non-ferrous materials to the tap. Provides superior performance for tapping cast aluminium and N other non-ferrous materials.
Coated carbide, PVD two-layer coating with heat-resistant TiAlN base layer and low-friction MoS2 top layer over carbide substrate. Use in hardened steel 55–63 HRC.
Coated HSS-E-PM, PVD heat- and wear-resistant high-vanadium cobalt powder metal HSS substrate coated with wear-resistant TiCN base layer. Use in steel, cast iron, and cast aluminium with silicon.
H P
K
M HSS-E-PM, PVD heat- and wear-resistant high-vanadium cobalt powder metal HSS substrate. Coating consists of low-friction CrC/C over wear-resistant TiN base layer. Use for tapping stainless steel and non-ferrous materials. N
WID_Master16_Taps_X006_X007_Metric_REBRAND.indd 6LViWID M16 T X006 X007 M i REBRAND O b 23 2015 9 48 AM 10/30/15 3:01 PM