Каталог Tungaloy глубокое сверление 1 - страница 2
Навигация
 Брошюра Tungaloy новая продукция
 Каталог Tungaloy инструмент для автоматов швейцарского типа
 Каталог Tungaloy глубокое сверление 2
 Общий каталог Tungaloy 2020 - 2021
 Каталог Tungaloy зубофрезерование
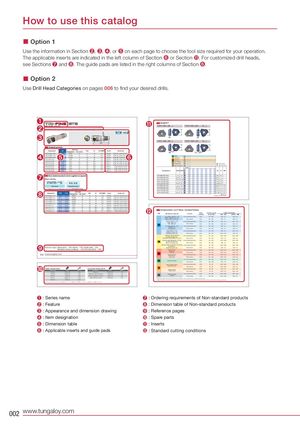
How to use this catalog
- Option 1
Use the information in Section ❷, ❸, ❹, or ❺ on each page to choose the tool size required for your operation. The applicable inserts are indicated in the left column of Section ❻ or Section . For customized drill heads, see Sections ❼ and ❽. The guide pads are listed in the right columns of Section ❻.
- Option 2
Use Drill Head Categories on pages 006 to find your desired drills.
❶❶
INSERT
| ❷❷ T R I - F I N E STS - E X | TO H T- N D J ( 0 8 . . .) | TO H T- N D J ( 0 9 . . . - 12 . . .) | |
| Indexable head with external 4 - s t a r t thread for single tube system ( STS ) |
❸❸ S S
| LF | TO H T- N D L ( 0 8 . . .) | TO H T- N D L ( 0 9 . . . - 12 . . .) | ||
| OAL | ||||
| Standard products | ||||
| Drill tube |
| Designation DC | Designation | Dia. (mm) | OAL | LF | DCONMS | Insert | Guide pad | S RE | RE | |||||||
| S | ||||||||||||||||
| ❹❹ FNTR-0097S-16.00 ❺❺16.00 | ST0097 | 14 | 57 | 55 | 12.6 | TOHT08... | GP06-075, GP06-20-075-DC❻❻ | |||||||||
| FNTR-0098S-17.00 | 17.00 | ST0098 | 15 | 57 | 55 | 13.6 | TOHT08... | GP06-075, GP06-20-075-DC | P | Steel | ||||||
| FNTR-0000S-20.00 | 20.00 | ST0000 | 17 | 59 | 56 | 15.5 | TOHT09... | GP06-085, GP06-20-085-DC | M | Stainless | ||||||
| FNTR-00S-21.00 | 21.00 | ST00 | 18 | 63 | 60 | 16 | TOHT10... | GP06-085, GP06-20-085-DC | K | Cast iron | ||||||
| FNTR-01S-22.00 | 22.00 | ST01 | 20 | 69 | 65.5 | 18 | TOHT11... | GP06-100, GP06-20-100-DC | N | Non-ferrous | ||||||
| FNTR-01S-24.00 | 24.00 | ST01 | 20 | 69 | 65.5 | 18 | TOHT11... | GP06-100, GP06-20-100-DC | S | Superalloys | : First choice | |||||
| FNTR-02S-25.00 | 25.00 | ST02 | 22 | 69 | 65.5 | 19.5 | TOHT11... | GP06-100, GP06-20-100-DC | H | Hard materials | : Second choice | |||||
| FNTR-02S-25.40 | 25.40 | ST02 | 22 | 69 | 65.5 | 19.5 | TOHT12... | GP06, GP06-20-120-DC | Coated | |||||||
| FNTR-02S-26.00 | 26.00 | ST02 | 22 | 69 | 65.5 | 19.5 | TOHT12... | GP06, GP06-20-120-DC | ||||||||
| FNTR-03S-28.00 | 28.00 | ST03 | 24 | 69 | 65.5 | 21 | TOHT12... | GP06, GP06-20-120-DC | Designation | DCN DCX | IC S RE | |||||
| ❼❼ | Non-standard products (to be supplied on request) | TOHT080305R-NDJ | 16 | 18 | 8.55 2.8 - | |||||||||||
| TOHT090305R-NDJ | 18.01 | 20 | 8.32 3 - | |||||||||||||
| When ordering | TOHT100305R-NDJ | 20.01 21.99 | 9.23 3.3 - | |||||||||||||
| FNTR-**S - | xx.xx | TOHT110405R-NDJ | 22 | 25 | 10.4 3.8 - | |||||||||||
| TOHT120405R-NDJ | 25.01 | 28 | 11.59 4.3 - | |||||||||||||
| TOHT080305R-NDL | 16 | 18 | 8.55 2.8 0.5 | |||||||||||||
| Drill head | Diameter (mm) | TOHT090305R-NDL | 18.01 | 20 | 8.32 3 0.5 | |||||||||||
| e.g. Designation for tool diameter ø16.5 mm: FNTR-0097S-16.50 | TOHT100305R-NDL | 20.01 21.99 | 9.23 3.3 0.5 | |||||||||||||
| ❽❽ | Drill tube | TOHT110405R-NDL | 22 | 25 | 10.4 3.8 0.5 | |||||||||||
| DCN Designation DCX | OAL | LF DCONMS | Insert | Guide pad | TOHT120405R-NDL | 25.01 | 28 | 11.59 4.3 0.5 | ||||||||
| Designation | Dia. (mm) | 䖃: Line up | ||||||||||||||
| FNTR-0097S-xx.xx | 16.00 16.70 | ST0097 14 | 57 | 55 12.6 | TOHT08... | GP06-075, GP06-20-075-DC | Package quantity = 10 pcs. | |||||||||
| FNTR-0098S-xx.xx | 16.71 17.70 | ST0098 15 | 57 | 55 13.6 | TOHT08... | GP06-075, GP06-20-075-DC | ||||||||||
| FNTR-0099S-xx.xx | 17.71 18.00 | ST0099 16 | 59 | 56 14.5 | TOHT09... | GP06-075, GP06-20-075-DC | ||||||||||
| FNTR-0099S-xx.xx | 18.01 18.90 | ST0099 16 | 59 | 56 14.5 | TOHT09... | GP06-085, GP06-20-085-DC | ||||||||||
| FNTR-0000S-xx.xx | 18.91 20.00 | ST0000 17 | 59 | 56 15.5 | TOHT09... | GP06-085, GP06-20-085-DC | ||||||||||
| FNTR-00S-xx.xx | 20.01 21.80 | ST00 18 | 63 | 60 16 | TOHT10... | GP06-085, GP06-20-085-DC | ||||||||||
| FNTR-01S-xx.xx | 21.81 24.10 | ST01 20 | 69 | 65.5 18 | TOHT11... | GP06-100, GP06-20-100-DC | ||||||||||
| FNTR-02S-xx.xx | 24.11 26.40 | ST02 22 | 69 | 65.5 19.5 | TOHT11... | GP06-100, GP06-20-100-DC | STANDARD CUTTING CONDITIONS | |||||||||
| FNTR-03S-xx.xx | 26.41 28.00 | ST03 24 | 69 | 65.5 21 | TOHT12... | GP06, GP06-20-120-DC | f | |||||||||
| ISO Workpiece material | Priority | Chip- | Cutting speed | Feed: (mm/rev) | ||||||||||||
| breaker | Vc (m/min) | ø16 - ø18 | ø18.01 - ø28 | |||||||||||||
| Low carbon steel (C < 0.3) | For low feed machines | NDL | 50 - 100 | 0.03 - 0.1 | 0.03 - 0.1 | |||||||||||
| SS400, SM490, S25C, etc. | First choice | NDJ | 80 - 140 | 0.05 - 0.1 | 0.05 - 0.1 | |||||||||||
| St42-1, St52-3, C25, etc. | ||||||||||||||||
| Carbon steel (C > 0.3) | For low feed machines | NDL | 50 - 100 | 0.03 - 0.1 | 0.03 - 0.12 | |||||||||||
| S45C, S55C, etc. | First choice | NDJ | 80 - 140 | 0.05 - 0.16 | 0.05 - 0.2 | |||||||||||
| C45, C55, etc. | ||||||||||||||||
| Low alloy steel (C < 0.3) | For low feed machines | NDL | 50 - 100 | 0.03 - 0.1 | 0.03 - 0.1 | |||||||||||
| SCM415, etc. | ||||||||||||||||
| 18CrMo4, etc. | First choice | NDJ | 80 - 140 | 0.05 - 0.1 | 0.05 - 0.1 | |||||||||||
| Alloy steel (C > 0.3) | For low feed machines | NDL | 50 - 100 | 0.03 - 0.1 | 0.03 - 0.12 | |||||||||||
| SCM440, SCr420, etc. | ||||||||||||||||
| 42CrMo4, 20Cr4, etc. | First choice | NDJ | 80 - 120 | 0.05 - 0.16 | 0.05 - 0.2 | |||||||||||
| Stainless steel (Austenitic) | For low feed machines | NDL | 50 - 100 | 0.03 - 0.06 | 0.03 - 0.06 | |||||||||||
| SUS304, SUS316, etc. | ||||||||||||||||
| X5CrNi18-9, X5CrNiMo17-12-3, etc. | First choice | NDJ | 60 - 100 | 0.05 - 0.1 | 0.05 - 0.1 | |||||||||||
| Stainless steel (Martensitic, Ferritic) | For low feed machines | NDL | 50 - 100 | 0.03 - 0.06 | 0.03 - 0.06 | |||||||||||
| SUS430, SUS416, etc. | First choice | NDJ | 60 - 100 | 0.05 - 0.1 | 0.05 - 0.1 | |||||||||||
| X6Cr17, X12CrS13, etc. | ||||||||||||||||
| ❾❾ | Stainless steel (Precipitation hardening) | For low feed machines | NDL | 50 - 100 | 0.03 - 0.06 | 0.03 - 0.06 | ||||||||||
| Reference pages: Spare parts → 012, Inserts → 013, Guide pads → 014, | SUS630, etc. | First choice | NDJ | 60 - 100 | 0.05 - 0.1 | 0.05 - 0.1 | ||||||||||
| X5CrNiCuNb16-4, etc. | ||||||||||||||||
| Standard cutting conditions → 015, Drill tube (STS) → 062 | Grey cast iron | For low feed machines | NDL | 50 - 100 | 0.03 - 0.15 | 0.05 - 0.18 | ||||||||||
| FC250, etc. | First choice | NDJ | 80 - 140 | 0.05 - 0.25 | 0.05 - 0.3 | |||||||||||
| 010 www.tungaloy.com | 250, etc. | |||||||||||||||
| Ductile cast iron | For low feed machines | NDL | 50 - 100 | 0.03 - 0.15 | 0.05 - 0.18 | |||||||||||
| FCD700, etc. | ||||||||||||||||
| 700-2, etc. | First choice | NDJ | 80 - 140 | 0.05 - 0.25 | 0.05 - 0.3 | |||||||||||
| Aluminium alloys | For low feed machines | NDL | 80 - 160 | 0.03 - 0.15 | 0.03 - 0.15 | |||||||||||
| First choice | NDJ | 100 - 200 | 0.05 - 0.2 | 0.05 - 0.2 | ||||||||||||
| Heat-resistant alloys | For low feed machines | NDL | 20 - 50 | 0.03 - 0.06 | 0.03 - 0.08 | |||||||||||
| ➓➓ | Inconel 718, etc. | First choice | NDJ | 20 - 50 | 0.04 - 0.08 | 0.04 - 0.1 | ||||||||||
| INSERT SPARE PARTS | GUIDE PAD SPARE PARTS | Titanium alloys | For low feed machines | NDL | 30 - 60 | 0.03 - 0.1 | 0.03 - 0.12 | |||||||||
| Designation | Screw | Wrench | Designation | Screw | Wrench | Ti-6Al-4V, etc. | First choice | NDJ | 30 - 60 | 0.05 - 0.13 | 0.05 - 0.15 | |||||
| TOHT08... CSTB-2.5S | T-8F | GP06-075 | CSTB-2.2S | T-7F | ||||||||||||
| TOHT09... CSTB-2.5S | T-8F | GP06-085, GP06-20-085-DC | CSTB-2.2S | T-7F | Hardened steel | For low feed machines | NDL | 40 - 100 | 0.03 - 0.08 | 0.03 - 0.08 | ||||||
| TOHT10... CSTB-3S | T-9F | GP06-100, GP06-20-100-DC | CSTB-2.2S | T-7F | ≥ 40HRC | First choice | NDJ | 50 - 100 | 0.04 - 0.08 | 0.04 - 0.1 | ||||||
| TOHT11... CSTB-3.5H | T-15F | GP06, GP06-20-120-DC | CSTB-2.2S | T-7F | Cutting parameters shown here are relating to the basic recommendations for cutting materials given. | |||||||||||
| TOHT12... CSTB-4S | T-15F | Cutting conditions, material hardness, and other relevant variables must be taken into considerations to determine the actual cutting parameters. |
Recommended clamping torque: CSTB-2.2S = 1 N∙m, CSTB-2.5S/CSTB-3S = 2.3 N∙m, CSTB-3.5H/CSTB-4S = 3 N∙m
| ❶ : Series name | ❼ : Ordering requirements of Non-standard products |
| ❷ : Feature | ❽ : Dimension table of Non-standard products |
| ❸ : Appearance and dimension drawing | ❾ : Reference pages |
| ❹ : Item designation | ➓ : Spare parts |
❺ : Dimension table : Inserts ❻ : Applicable inserts and guide pads : Standard cutting conditions