Брошюра Tungaloy новая продукция - страница 99
Навигация
 Каталог Tungaloy глубокое сверление 2
 Каталог Tungaloy глубокое сверление 1
 Каталог Tungaloy зубофрезерование
 Общий каталог Tungaloy 2020 - 2021
 Каталог Tungaloy инструмент для автоматов швейцарского типа
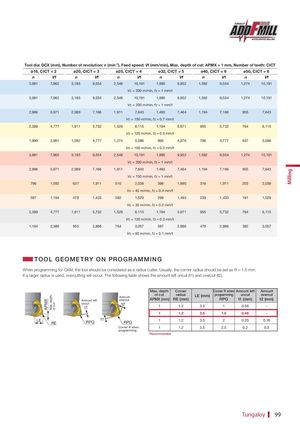
Tool dia: DCX (mm), Number of revolution: n (min-1), Feed speed: Vf (mm/min), Max. depth of cut: APMX = 1 mm, Number of teeth: CICT
| ø16, CI | CT = 2 | ø20, CI | CT = 3 | ø25, | CICT = 4 | ø32, CIC | T = 5 | ø40, CI | CT = 6 | ø50, C | ICT = 8 |
| n | Vf | n | Vf | n | Vf | n | Vf | n | Vf | n | Vf |
| 3,981 | 7,962 | 3,185 | 9,554 | 2,548 | 10,191 | 1,990 | 9,952 | 1,592 | 9,554 | 1,274 | 10,191 |
| Vc = 200 m/m | in,fz = 1 mm/t | ||||||||||
| 3,981 | 7,962 | 3,185 | 9,554 | 2,548 | 10,191 | 1,990 | 9,952 | 1,592 | 9,554 | 1,274 | 10,191 |
| Vc = 200 m/m | in,fz = 1 mm/t | ||||||||||
| 2,986 | 5,971 | 2,389 | 7,166 | 1,911 | 7,643 | 1,493 | 7,464 | 1,194 | 7,166 | 955 | 7,643 |
| Vc = 150 m/mi | n,fz = 0.7 mm/t | ||||||||||
| 2,389 | 4,777 | 1,911 | 5,732 | 1,529 | 6,115 | 1,194 | 5,971 | 955 | 5,732 | 764 | 6,115 |
| Vc = 120 m/mi | n,fz = 0.5 mm/t | ||||||||||
| 1,990 | 3,981 | 1,592 | 4,777 | 1,274 | 5,096 | 995 | 4,976 | 796 | 4,777 | 637 | 5,096 |
| Vc = 100 m/mi | n,fz = 0.3 mm/t | ||||||||||
| 3,981 | 7,962 | 3,185 | 9,554 | 2,548 | 10,191 Vc = 200 m/m | 1,990 in,fz = 1 mm/t | 9,952 | 1,592 | 9,554 | 1,274 | 10,191 |
| 2,986 | 5,971 | 2,389 | 7,166 | 1,911 | 7,643 | 1,493 | 7,464 | 1,194 | 7,166 | 955 | 7,643 |
| Vc = 150 m/m | in,fz = 1 mm/t | ||||||||||
| 796 597 | 1,592 1,194 | 637 478 | 1,911 1,433 | 510 382 | 2,038 Vc = 40 m/min 1,529 | 398 ,fz = 0.4 mm/t 299 | 1,990 1,493 | 318 239 | 1,911 1,433 | 255 191 | 2,038 1,529 |
| Vc = 30 m/min | ,fz = 0.2 mm/t | ||||||||||
| 2,389 | 4,777 | 1,911 | 5,732 | 1,529 | 6,115 | 1,194 | 5,971 | 955 | 5,732 | 764 | 6,115 |
| Vc = 120 m/mi | n,fz = 0.3 mm/t | ||||||||||
| 1,194 | 2,389 | 955 | 2,866 | 764 | 3,057 Vc = 60 m/min | 597 ,fz = 0.1 mm/t | 2,986 | 478 | 2,866 | 382 | 3,057 |
TOOL GEOMETRY O N PROGRAMMING
When programming for CAM, the tool should be considered as a radius cutter. Usually, the corner radius should be set as R = 1.5 mm. If a larger radius is used, overcutting will occur. The following table shows the amount left uncut (t1) and overcut (t2).
| APMX (mm) Max. depth of cut | RE (mm) Corner radius | LE (mm) | RPG Corner R when programming | t1 (mm) Amount left uncut | t2 (mm) Amount overcut |
| 1 | 1.2 | 3.5 | 1 | 0.56 | - |
| 1 | 1.2 | 3.5 | 1.5 | 0.46 | - |
| 1 | 1.2 | 3.5 | 2 | 0.35 | 0.16 |
| 1 | 1.2 | 3.5 | 2.5 | 0.2 | 0.5 |
Amount left overcut uncut t2
RE RPG RPG
programming *Recommended