Брошюра Tungaloy новая продукция - страница 93
Навигация
 Каталог Tungaloy глубокое сверление 2
 Каталог Tungaloy глубокое сверление 1
 Каталог Tungaloy зубофрезерование
 Общий каталог Tungaloy 2020 - 2021
 Каталог Tungaloy инструмент для автоматов швейцарского типа
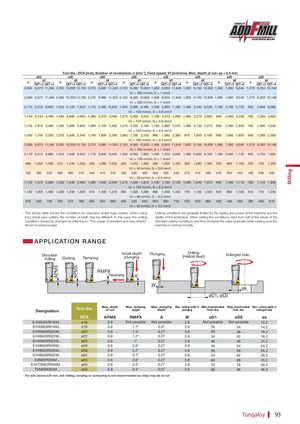
| T | ool dia.: | DCX( | mm), | Number | of revo | lution | s:n (min-1), F | eed sp | eed:Vf | (mm/m | in), M | ax. dep | th of c | ut:ap | = 0.5 m | m | ||||||
| ø22 | ø25 | ø28 | ø30 | ø32 | ø35 | ø40 | ø50 | |||||||||||||||
| V | f | Vf | V | f | Vf | V | f | V | f | Vf | Vf | |||||||||||
| n | CICT = 3 | CICT = 4 | n | CICT = 4 C | ICT = 5 | n | CICT = 4 | CICT = 5 | n | CICT = 4 CICT = 5 | n | CICT = 5 | CICT = 6 | n | CICT = 5 | CICT = 6 | n | CICT = 5 | CICT = 6 | n | CICT = | 5 CICT = 8 |
| 2,890 | 8,670 | 11,560 | 2,550 | 10,200 1 | 2,750 | 2,270 | 9,080 | 11,350 | 2,120 | 8,480 10,600 Vc =200 m/m | 1,990 in,fz = | 9,950 1 mm/t | 11,940 | 1,820 | 9,100 | 10,920 | 1,590 | 7,950 | 9,540 | 1,270 | 6,350 | 10,160 |
| 2,890 | 8,670 | 11,560 | 2,550 | 10,200 1 | 2,750 | 2,270 | 9,080 | 11,350 | 2,120 | 8,480 10,600 Vc =200 m/m | 1,990 in,fz = | 9,950 1 mm/t | 11,940 | 1,820 | 9,100 | 10,920 | 1,590 | 7,950 | 9,540 | 1,270 | 6,350 | 10,160 |
| 2,170 | 5,210 | 6,950 | 1,910 | 6,120 | 7,640 | 1,710 | 5,480 | 6,840 | 1,590 | 5,090 6,360 Vc =150 m/mi | 1,490 n,fz = | 5,960 0.8 mm/t | 7,160 | 1,360 | 5,440 | 6,530 | 1,190 | 4,760 | 5,720 | 950 | 3,800 | 6,080 |
| 1,740 | 3,140 | 4,180 | 1,530 | 3,680 | 4,590 | 1,360 | 3,270 | 4,080 | 1,270 | 3,050 3,810 Vc =120 m/mi | 1,190 n,fz = | 3,570 0.6 mm/t | 4,290 | 1,090 | 3,270 | 3,930 | 950 | 2,850 | 3,420 | 760 | 2,280 | 3,650 |
| 1,740 | 2,610 | 3,480 | 1,530 | 3,060 | 3,830 | 1,360 | 2,720 | 3,400 | 1,270 | 2,540 3,180 Vc =120 m/mi | 1,190 n,fz = | 2,980 0.5 mm/t | 3,570 | 1,090 | 2,730 | 3,270 | 950 | 2,380 | 2,850 | 760 | 1,900 | 3,040 |
| 1,450 | 1,740 | 2,320 | 1,270 | 2,040 | 2,540 | 1,140 | 1,830 | 2,280 | 1,060 | 1,700 2,120 Vc =100 m/mi | 990 n,fz = | 1,980 0.4 mm/t | 2,380 | 910 | 1,820 | 2,190 | 800 | 1,600 | 1,920 | 640 | 1,280 | 2,050 |
| 2,890 | 8,670 | 11,560 | 2,550 | 10,200 1 | 2,750 | 2,270 | 9,080 | 11,350 | 2,120 | 8,480 10,600 Vc =200 m/m | 1,990 in,fz = | 9,950 1 mm/t | 11,940 | 1,820 | 9,100 | 10,920 | 1,590 | 7,950 | 9,540 | 1,270 | 6,350 | 10,160 |
| 2,170 | 6,510 | 8,680 | 1,910 | 7,640 | 9,550 | 1,710 | 6,840 | 8,550 | 1,590 | 6,360 7,950 Vc =150 m/m | 1,490 in,fz = | 7,450 1 mm/t | 8,940 | 1,360 | 6,800 | 8,160 | 1,190 | 5,950 | 7,140 | 950 | 4,750 | 7,600 |
| 580 | 1,050 | 1,400 | 510 | 1,230 | 1,530 | 450 | 1,080 | 1,350 | 420 | 1,010 1,260 Vc =40 m/min | 400 ,fz = 0 | 1,200 .6 mm/t | 1,440 | 360 | 1,080 | 1,300 | 320 | 960 | 1,160 | 250 | 750 | 1,200 |
| 430 | 390 | 520 | 380 | 460 | 570 | 340 | 410 | 510 | 320 | 390 480 Vc =30 m/min | 300 ,fz = 0 | 450 .3 mm/t | 540 | 270 | 410 | 490 | 240 | 360 | 440 | 190 | 290 | 460 |
| 1,740 | 1,570 | 2,090 | 1,530 | 1,840 | 2,300 | 1,360 | 1,640 | 2,040 | 1,270 | 1,530 1,910 Vc =120 m/mi | 1,190 n,fz = | 1,790 0.3 mm/t | 2,150 | 1,090 | 1,640 | 1,970 | 950 | 1,430 | 1,710 | 760 | 1,140 | 1,830 |
| 1,160 | 1,050 | 1,400 | 1,020 | 1,230 | 1,530 | 910 | 1,100 | 1,370 | 850 | 1,020 1,280 Vc = 80 m/min | 800 ,fz = 0 | 1,200 .3 mm/t | 1,440 | 730 | 1,100 | 1,320 | 640 | 960 | 1,160 | 510 | 770 | 1,230 |
| 870 | 530 | 700 | 760 | 610 | 760 | 680 | 550 | 680 | 640 | 520 640 Vc = 60 m/min | 600 ,fz = 0 | 600 .2 mm/t | 720 | 550 | 550 | 660 | 480 | 480 | 580 | 380 | 380 | 610 |
| - The above table shows the conditions for standard shank type cutters. When using | - Cutting conditions are generally limited by the rigidity and power of the machine and the |
| long shank type cutters, the number of teeth may be different. In this case, the cutting | rigidity of the workpiece. When setting the conditions, start from half of the values of the |
| conditions should be changed by referring to: “The usage of standard and long shanks” | standard cutting conditions and then increase the value gradually while making sure the |
| shown in previous page | machine is running normally |
APPLICATION R ANGE
| APMX Shoulder milling Slot | APMX ting Rampin | RMPX Traversin g | A g Small depth plunging | Plunging | Drilling (Helical feed) | Enlarged hole | |
| W | ae | ||||||
| øD1, øD | 2 | ||||||
| Designation | DCX Tool dia. | APMX Max. depth of cut | RMPX Max. ramping angle | A Max. plunging depth | W øD1 Max. cutting width in plunging Min.machinable hole dia. | øD2 Max.machinable hole dia. | ae Max. cutting width in enlarged hole |
| E/HXN03R016M... | ø16 | 0.9 | Not possible | Not possible | 3.8 Not possible | Not possible | 12.2 |
| E/HXN03R018M... | ø18 | 0.9 | 1.7° | 0.27 | 3.8 26 | 34 | 14.2 |
| E/HXN03R020M... | ø20 | 0.9 | 1.4° | 0.27 | 3.8 30 | 38 | 16.2 |
| E/HXN03R022M... | ø22 | 0.9 | 1.2° | 0.27 | 3.8 34 | 42 | 18.2 |
| E/HXN03R025M... | ø25 | 0.9 | 1° | 0.27 | 3.8 40 | 48 | 21.2 |
| E/HXN03R028M... | ø28 | 0.9 | 0.8° | 0.27 | 3.8 46 | 54 | 24.2 |
| E/HXN03R030M... | ø30 | 0.9 | 0.7° | 0.27 | 3.8 50 | 58 | 26.2 |
| E/HXN03R032M... | ø32 | 0.9 | 0.7° | 0.27 | 3.8 54 | 62 | 28.2 |
| EXN03R035M... | ø35 | 0.9 | 0.6° | 0.27 | 3.8 60 | 68 | 31.2 |
| E/H/TXN03R040M… | ø40 | 0.9 | 0.5° | 0.27 | 3.8 70 | 78 | 36.2 |
| TXN03R050M... | ø50 | 0.9 | 0.4° | 0.27 | 3.8 90 | 98 | 46.2 |
・ For øDc above ø33 mm, slot milling, ramping or contouring is not recommended as chips may be re-cut