Брошюра Tungaloy новая продукция - страница 144
Навигация
 Каталог Tungaloy глубокое сверление 2
 Каталог Tungaloy глубокое сверление 1
 Каталог Tungaloy зубофрезерование
 Общий каталог Tungaloy 2020 - 2021
 Каталог Tungaloy инструмент для автоматов швейцарского типа
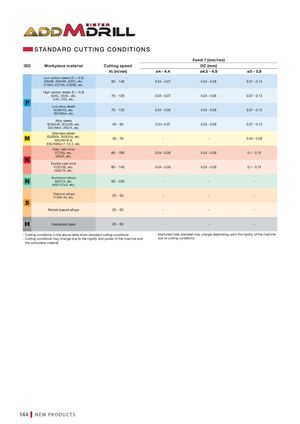
STANDARD CUTTING CONDITIONS
| Feed:f (mm/rev) | |||||
| ISO | Workpiece material | Cutting speed | DC(mm) | ||
| Vc (m/min) | ø4 - 4.4 | ø4.5 - 4.9 | ø5 - 5.9 | ||
| Low carbon steels (C < 0.3) SS400, SM490, S25C, etc. C15E4, E275A, E355D, etc. | 80 - 140 | 0.04 - 0.07 | 0.04 - 0.08 | 0.07 - 0.13 | |
| High carbon steels (C > 0.3) S45C, S55C, etc. C45, C55, etc. | 70 - 120 | 0.04 - 0.07 | 0.04 - 0.08 | 0.07 - 0.13 | |
| Low alloy steels SCM415, etc. 18CrMo4, etc. | 70 - 120 | 0.04 - 0.06 | 0.05 - 0.08 | 0.07 - 0.13 | |
| Alloy steels SCM440, SCr420, etc. 42CrMo4, 20Cr4, etc. | 40 - 90 | 0.04 -0.07 | 0.05 - 0.08 | 0.07 - 0.13 | |
| Stainless steels SUS304, SUS316, etc. X5CrNi18-9, X5CrNiMo17-12-2, etc. | 30 - 70 | - | - | 0.04 - 0.08 | |
| Grey cast irons FC250, etc. | 80 - 180 | 0.04 - 0.08 | 0.04 - 0.08 | 0.1 - 0.15 | |
| GG25, etc. | |||||
| Ductile cast irons FCD700, etc. GGG70, etc. | 80 - 140 | 0.04 - 0.08 | 0.04 - 0.08 | 0.1 - 0.15 | |
| Aluminium alloys ADC12, etc. AlSi11Cu3, etc. | 80 - 220 | - | - | - | |
| Titanium alloys Ti-6Al-4V, etc. | 20 - 50 | - | - | - | |
| Nickel-based alloys | 20 - 50 | - | - | - | |
| Hardened steel | 20 - 50 | - | - | - |
- Cutting conditions in the above table show standard cutting conditions - Machined hole diameter may change depending upon the rigidity of the machine - Cutting conditions may change due to the rigidity and power of the machine and tool or cutting conditions the workpiece material