Брошюра Tungaloy новая продукция - страница 115
Навигация
 Каталог Tungaloy глубокое сверление 2
 Каталог Tungaloy глубокое сверление 1
 Каталог Tungaloy зубофрезерование
 Общий каталог Tungaloy 2020 - 2021
 Каталог Tungaloy инструмент для автоматов швейцарского типа
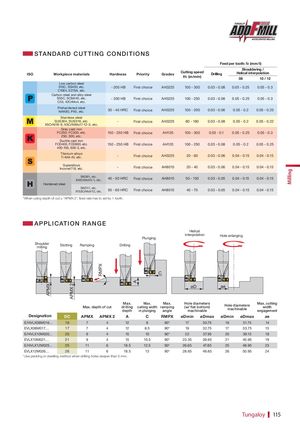
STANDARD CUT TING CONDITIONS
| Feed | per tooth:fz ( | mm/t) | ||||||
| ISO | Workpiece materials | Hardness | Priority | Grades | Cutting speed V (m/min) | Drilling | Should Helical int | ering / erpolation |
| c | 08 | 10 / 12 | ||||||
| Low carbon steel S15C, SS400, etc. C15E4, E275A, etc. | - 200 HB | First choice | AH3225 | 100 - 300 | 0.03 - 0.08 | 0.05 - 0.25 | 0.05 - 0.3 | |
| Carbon steel and alloy steel S55C, SCM440, etc. C55, 42CrMo4, etc. | - 300 HB | First choice | AH3225 | 100 - 250 | 0.03 - 0.08 | 0.05 - 0.25 | 0.05 - 0.3 | |
| Prehardened steel NAK80, PX5, etc. | 30 - 40 HRC | First choice | AH3225 | 100 - 200 | 0.03 - 0.06 | 0.05 - 0.2 | 0.05 - 0.25 | |
| Stainless steel SUS304, SUS316, etc. X5CrNi18-9, X5CrNiMo17-12-3, etc. | - | First choice | AH3225 | 80 - 180 | 0.03 - 0.08 | 0.05 - 0.2 | 0.05 - 0.22 | |
| Grey cast iron FC250, FC300, etc. 250, 300, etc. | 150 - 250 HB | First choice | AH120 | 100 - 300 | 0.03 - 0.1 | 0.05 - 0.25 | 0.05 - 0.3 | |
| Ductile cast iron FCD400, FCD600, etc. 400-15S, 600-3, etc. | 150 - 250 HB | First choice | AH120 | 100 - 250 | 0.03 - 0.08 | 0.05 - 0.2 | 0.05 - 0.25 | |
| Titanium alloys Ti-6AI-4V, etc. | - | First choice | AH3225 | 20 - 60 | 0.03 - 0.06 | 0.04 - 0.15 | 0.04 - 0.15 | |
| Superalloys Inconel718, etc. | - | First choice | AH8015 | 20 - 40 | 0.03 - 0.06 | 0.04 - 0.15 | 0.04 - 0.15 | |
| Hdd tl SKD61, etc. X40CrMoV5-1, etc. | 40 - 50 HRC | First choice | AH8015 | 50 - 150 | 0.03 - 0.05 | 0.04 - 0.15 | 0.04 - 0.15 | |
| arene see SKD11, etc. X153CrMoV12, etc. | 50 - 60 HRC | First choice | AH8015 | 40 - 70 | 0.03 - 0.05 | 0.04 - 0.15 | 0.04 - 0.15 |
*When using depth of cut ≥ "APMX 2", feed rate has to set by 1 tooth.
APPLICATION R ANGE
| Shoulder milling | Slotting | Ramping | RMPX | Drilling | Plunging | C | Helic interpola | al tion | Hole enlar | ging | |
| A | |||||||||||
| APMX Designation | APMX 2 DC | APMX Max. de | APMX 2 pth of cut | A Max. drilling depth | C Max. cutting width in plunging | RMPX Max. ramping angle | øD øDmin Hole dia (w/ flat b machi | øDmax meters ottom) nable | ae øDmin Hole di mach | øDmax ameters inable | ae Max. cutting width engagement |
| E/HVLX08M016… | 16 | 7 | 4 | 12 | 8 | 90° | 17 | 30.75 | 16 | 31.75 | 14 |
| EVLX08M017… | 17 | 7 | 4 | 12 | 8.5 | 90° | 19 | 32.75 | 17 | 33.75 | 15 |
| E/HVLX10M020... | 20 | 9 | 4 | 15 | 10 | 90° | 22 | 37.95 | 20 | 39.15 | 18 |
| EVLX10M021… | 21 | 9 | 4 | 15 | 10.5 | 90° | 23.35 | 39.95 | 21 | 40.95 | 19 |
| E/HVLX12M025... | 25 | 11 | 6 | 18.5 | 12.5 | 90° | 26.65 | 47.85 | 25 | 48.95 | 23 |
| EVLX12M026… | 26 | 11 | 6 | 18.5 | 13 | 90° | 28.65 | 49.85 | 26 | 50.95 | 24 |
*Use pecking or dwelling method when drilling holes deeper than 5 mm.