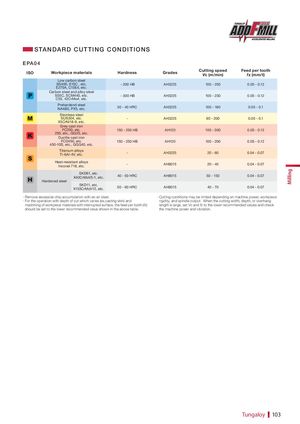
| ISO | Workpiece materials | Hardness | Grades | Cutting speed Vc (m/min) | Feed per tooth fz (mm/t) |
| Low carbon steel SS400, S15C , etc. E275A, C15E4, etc. | - 200 HB | AH3225 | 100 - 250 | 0.05 - 0.12 |
| Carbon steel and alloy steel S55C, SCM440, etc. C55, 42CrMo4, etc. | - 300 HB | AH3225 | 100 - 230 | 0.05 - 0.12 |
| Prehardend steel NAK80, PX5, etc. | 30 - 40 HRC | AH3225 | 100 - 180 | 0.05 - 0.1 |
| Stainless steel SUS304, etc. X5CrNi18-9, etc. | - | AH3225 | 90 - 200 | 0.05 - 0.1 |
| Grey cast iron FC250, etc. 250, etc., GG25, etc. | 150 - 250 HB | AH120 | 100 - 300 | 0.05 - 0.12 |
| Ductile cast iron FCD450, etc. 450-10S, etc., GGG45, etc. | 150 - 250 HB | AH120 | 100 - 200 | 0.05 - 0.12 |
| Titanium alloys Ti-6AI-4V, etc. | - | AH3225 | 20 - 60 | 0.04 - 0.07 |
| Heat-resistant alloys Inconel 718, etc. | - | AH8015 | 20 - 40 | 0.04 - 0.07 |
| SKD61, etc. X40CrMoV5-1, etc. | 40 - 50 HRC | AH8015 | 50 - 150 | 0.04 - 0.07 |
| SKD11, etc. X153CrMoV12, etc. Hardened steel | 50 - 60 HRC | AH8015 | 40 - 70 | 0.04 - 0.07 |
 Каталог Tungaloy глубокое сверление 2
 Каталог Tungaloy глубокое сверление 1
 Каталог Tungaloy зубофрезерование
 Общий каталог Tungaloy 2020 - 2021
 Каталог Tungaloy инструмент для автоматов швейцарского типа