Каталог TooTool техническая информация 2 - страница 181
Навигация
 Каталог TooTool техническая информация 1
 Общий каталог TooTool
 Каталог TooTool монолитные фрезы
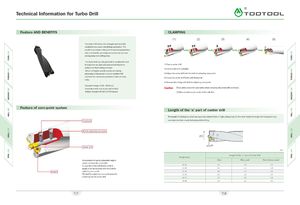
Technical Information for Turbo Drill A\
Feature AND BENEFITS CLAMPING
—
(D (2) (3) (4 ) (5)
The turbo drill delivers the strength and versatility
needed for any deep hole drilling application.The
go* -K
V
excellent geometry is designed to increase penetration
i
rates and tool life,providing the lowest cost per hole
among deep hole drilling lines.
•The Turbo Drill uses the pilot drill to stabilize the tool
through the cut, and outboard carbide inserts to 1) Place a center drill.
achieve the final cutting diameter
2) Clamp insert and cartridge .
•Allows for higher spindle speeds and taking
advantage of the power curve on modern CNC 3) Adjust the center drill with the bolt for adjusting cone point.
machines for maximum penetration rates on deep
4) Clamp the center drill firmly with fixing bolt.
holes.
5) Reassure the clamp with bolt for adjusting cone point.
•Diameter Range: 25.00 - 80.00mm.
•Available in 4xD, SxD, 6.5xD, 8xD & 10xD Caution ®Use safety covers for your safety when clamping the center drill and insert.
•Utilizes Standard WCMX & SPMG Inserts ©When machining, be careful of the drill disk
Feature of corn- point system
Length of the ‘a’ part of center drill
The length of 'a' being too short can cause bad surface finish or high cutting load. On the other hand, the length of 'a' being too long
-| Fixed bolt | can make tool failure and chattering while drilling.
j Bolt for adjusting cone point ]
(
a.
sS (
j Center drill |
mm
i Designation
Length of the "a" part of center drill
•Convenient and quick adjustable heights Steel Alloy steel Non- ferrous metal
when inserting the center drill.
25- 30 1.2 1.0 1.5
•In case the centerdrill brakes while in
usage, it can be replaced with the bolt for 31-40 1.5 1.3 1.8
j Insert adjusting cone point. 41- 50 1.8 1.5 2.2
•The bolt for adjusting cone point prevents 51- 59 2.2 1.8 2.5
chattering on the centerdrill. 60-75 2.5 2.0 2.8
76-80 3.0 2.5 3.5
717 718