Каталог TooTool техническая информация 1 - страница 60
Навигация
 Общий каталог TooTool
 Каталог TooTool монолитные фрезы
 Каталог TooTool техническая информация 2
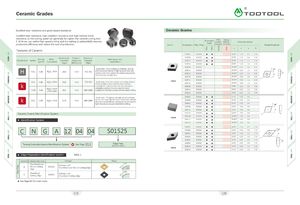
Ceramic Grades A\
Excellent wear resistance and good impact resistance. Ceramic Grades
Excellent heat resistance, high oxidation resistance and high thermal shock
resistance, so the cutting speed can generally be higher than carbide cutting tool
Aluminum PVD Silicon
3 -10 times, can realize high speed cutting and dry cutting to substantially improve Coated Nitride Dimensions(mm)
Oxide Ceramic Ceramic
production efficiency and reduce the cost of production. Inserts Designation Ddge Prep Geometries (mm)
I
— rn
o
—
i i
d t r D
j
—
j- oo
Features of Ceramic
120404 T02020 12.70 4.76 0.4 5.16
120408 T02020 12.70 4.76 0.8 5.16
Hardness of Fracture Transverse
Density Main Advantages and
Classification Symbol Substrate Toughness Strength 120412 T02020 12.70 4.76 1.2 5.16
(g/cm3) Component Applications
(Gpa) (MPa.ml/2) (Mpa) 120416 T02020 12.70 4.76 1.6 5.16
160608 T02020 15.875 6.35 0.8 6.35
• Application : Semi - roughing to finishing turning
and interrupted milling of high hardness steel and 160612 T02020 15.875 6.35 1.2 6.35
TT01 4.40 AI203+ TiCN 20.0 > 5.5 750-950
cast iron. It is most suitable for cutting mangnaness 160616 T02020 15.875 6.35 1.6 6.35
steel and high strength steel.
160708 T02020 15.875 7.94 0.8 6.35
160712 T02020 15.875 7.94 1.2 6.35
CNGA
TT03 4.80 AI203 + TiCN 19.0 >6.0 700 -900 •Application : It is most suitable for cutting all kinds
160716 T02020 15.875 7.94 1.6 6.35
of high hardness alloy steel and alloy cast iron,
especially for cutting ductile cast iron and boron - 190608 T02020 19.05 6.35 0.8 7.94
AI203 + TiCN containing cast iron. It can be used for semi -
190612 T02020 19.05 6.35 1.2 7.94
TT03N 4.60 20.1 >6.0 800 -1000 roughing to finishing turning and interrupted milling.
(TiN COAT)
190616 T02020 19.05 6.35 1.6 7.94
• Application : Roughing and high speed machining
120404 T02020 12.70 4.76 0.4
of cast iron, especially the nickel - based heat-resistant 120408 T02020 12.70 4.76 0.4
TSOI 3.40 Si3N4 +TiCN 17.0 >6.5 800 -1000
alloy has a good effect in cutting and can be used for
high feed processing and intermittent milling.
- 120412 T02020 12.70 4.76 0.4
120708 T02020 12.70 7.94 0.8
120712 T02020 12.70 7.94 0.8
120716 T02020 12.70 7.94 0.8
Ceramic Inserts Identification System
160708 T02020 15.875 7.94 0.8
CNGN
• Identification System 160712
160716
T02020
T02020
15.875
15.875
7.94
7.94
0.8
0.8
150404 T02020 12.70 4.76 0.4 5.16
C N G A 12 04 04 S01525 150408
150412
T02020
T02020
12.70
12.70
4.76
4.76
0.8
1.2
5.16
5.16 d
I J 150416 T02020 12.70 4.76 1.6 5.16
r_
} r 150604 T02020 12.70 6.35 0.4 5.16
" Turning Indexable Inserts Identification System " Q See Page 013 Edge Prep. 150608 T02020 12.70 6.35 0.8 5.16
.
(Ref to the Table 1) 150612 T02020 12.70 6.35 1.2 5.16
DNGA
150616 T02020 12.70 6.35 1.6 5.16
• Edge Preparation Identification System Table 1
Symbol Cutting Edge Spec. Example Shape
0.15
Chamfered and
d. 0.15 mm x 25”
a
CL
s Honed Cutting S01525 Chamfered and Honed Cutting Edge C^Honed
a> Edge
cn 0.20
s Chamfered 0.20mm x 25'
T Cutting Edge T02025
Chamfered Cutting Edge
•See Page B3 for insert color
119 120