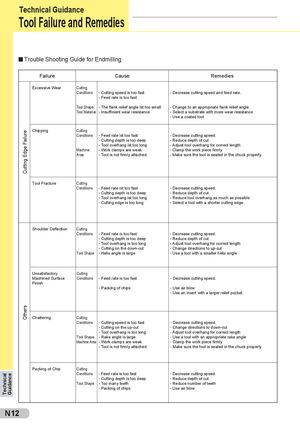
| Failure | | Cause | Remedies |
| Excessive Wear | Cutting Conditions Tool Shape Tool Material | - Cutting speed is too fast - Feed rate is too fast - The flank relief angle ist too small - Insufficient wear resistance | - Decrease cutting speed and feed rate. - Change to an appropriate flank relief angle. - Select a substrate with more wear resistance - Use a coated tool |
| Cutting Edge Failure | Chipping | Cutting Conditions Machine Area | - Feed rate ist too fast - Cutting depth is too deep - Tool overhang ist too long - Work clamps are weak - Tool is not firmly attached | - Decrease cutting speed. - Reduce depth of cut - Adjust tool overhang for correct length - Clamp the work piece firmly - Make sure the tool is seated in the chuck properly |
| Tool Fracture | Cutting Conditions | -Feed rate ist too fast - Cutting depth is too deep - Tool overhang ist too long - Cutting edge is too long | - Decrease cutting speed. - Reduce depth of cut - Reduce tool overhang as much as possible - Select a tool with a shorter cutting edge |
| Shoulder Deflection | Cutting Conditions Tool Shape | - Feed rate is too fast - Cutting depth is too deep - Tool overhang is too long - Cutting on the down-cut - Helix angle is large | - Decrease cutting speed. - Reduce depth of cut - Adjust tool overhang for correct length - Change directions to up-cut - Use a tool with a smaller helix angle |
| Unsatisfactory Machined Surface Finish | Cutting Conditions | - Feed rate is too fast - Packing of chips | - Decrease cutting speed. - Use air blow - Use an insert with a larger relief pocket. |
| Others | Chattering | Cutting Conditions Tool Shape Machine Area | - Cutting speed is too fast - Cutting on the up-cut - Tool overhang is too long - Rake angle is large - Work clamps are weak - Tool is not firmly attached | - Decrease cutting speed. - Change directions to down-cut - Adjust tool overhang for correct length - Use a tool with an appropriate rake angle - Clamp the work piece firmly - Make sure the tool is seated in the chuck properly |
| Packing of Chip | Cutting Conditions Tool Shape | -Feed rate is too fast - Cutting depth is too deep - Too many teeth - Packing of chips | - Decrease cutting speed. - Reduce depth of cut - Reduce number of teeth - Use air blow |
 Общий каталог Sumitomo 2012
 Каталог Sumitomo резьбонарезной инструмент
 Каталог Sumitomo пластины с режущей кромкой-моноалмаз Sumicristal
 Каталог Sumitomo инструмент для обработки канавок
 Общий каталог Sumitomo 2019 - 2020
 Каталог Sumitomo запасные части