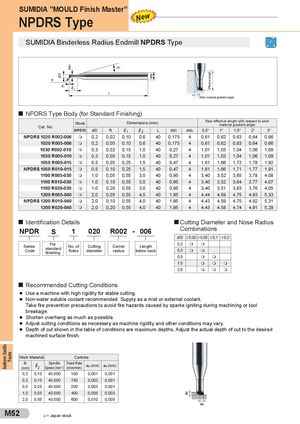
NPDRS Type New
SUMIDIA Binderless Radius Endmill NPDRS Type
15°
R 1 2 L Work material gradient angle
NPDRS Type Body (for Standard Finishing)
| Ct N | Stock | | | Dim | ensions ( | mm) | | | Real | effective l materi | ength with algradien | respect to t angle | work |
| a. o. | NPD10 | ØD | R | 1 | 2 | L | Ød1 | Øds | 0,5° | 1° | 1,5° | 2° | 3° |
| NPDRS 1020 R002-006 | m | 0,2 | 0,02 | 0,10 | 0,6 | 40 | 0,175 | 4 | 0,61 | 0,62 | 0,63 | 0,64 | 0,66 |
| 1020 R005-006 | m | 0,2 | 0,05 | 0,10 | 0,6 | 40 | 0,175 | 4 | 0,61 | 0,62 | 0,63 | 0,64 | 0,66 |
| 1030 R002-010 | m | 0,3 | 0,02 | 0,15 | 1,0 | 40 | 0,27 | 4 | 1,01 | 1,03 | 1,04 | 1,06 | 1,09 |
| 1030 R005-010 | m | 0,3 | 0,05 | 0,15 | 1,0 | 40 | 0,27 | 4 | 1,01 | 1,03 | 1,04 | 1,06 | 1,09 |
| 1050 R005-015 | m | 0,5 | 0,05 | 0,25 | 1,5 | 40 | 0,47 | 4 | 1,61 | 1,66 | 1,72 | 1,78 | 1,92 |
| NPDRS 1050 R010-015 | m | 0,5 | 0,10 | 0,25 | 1,5 | 40 | 0,47 | 4 | 1,61 | 1,66 | 1,71 | 1,77 | 1,91 |
| 1100 R005-030 | m | 1,0 | 0,05 | 0,55 | 3,0 | 40 | 0,95 | 4 | 3,40 | 3,52 | 3,65 | 3,78 | 4,08 |
| 1100 R010-030 | m | 1,0 | 0,10 | 0,55 | 3,0 | 40 | 0,95 | 4 | 3,40 | 3,52 | 3,64 | 3,77 | 4,07 |
| 1100 R020-030 | m | 1,0 | 0,20 | 0,55 | 3,0 | 40 | 0,95 | 4 | 3,40 | 3,51 | 3,63 | 3,76 | 4,05 |
| 1200 R005-040 | m | 2,0 | 0,05 | 0,55 | 4,0 | 40 | 1,95 | 4 | 4,44 | 4,59 | 4,75 | 4,93 | 5,33 |
| NPDRS 1200 R010-040 | m | 2,0 | 0,10 | 0,55 | 4,0 | 40 | 1,95 | 4 | 4,43 | 4,59 | 4,75 | 4,92 | 5,31 |
| 1200 R020-040 | m | 2,0 | 0,20 | 0,55 | 4,0 | 40 | 1,95 | 4 | 4,43 | 4,58 | 4,74 | 4,91 | 5,29 |
Identification Details Cutting Diameter and Nose Radius
| NPDR | S | 1 | 020 | R002 | 006 - |
| Series Code | For standard finishing | No. of flutes | Cutting diameter | Corner radius | Length below neck |
| ØD | r0,02 | r0,05 | r0,1 | r0,2 |
| 0,2 | m | m | | |
| 0,3 | m | m | | |
| 0,5 | | m | m | |
| 1,0 | | m | m | m |
| 2,0 | | m | m | m |
Recommended Cutting Conditions
- Use a machine with high rigidity for stable cutting.
- Non-water soluble coolant recommended. Supply as a mist or external coolant. Take fire prevention precautions to avoid fire hazards caused by sparks igniting during machining or tool breakage.
- Shorten overhang as much as possible.
- Adjust cutting conditions as necessary as machine rigidity and other conditions may vary.
- Depth of cut shown in the table of conditions are maximum depths. Adjust the actual depth of cut to the desired machined surface finish.
| Work M | aterial | | Carbi | de | |
| R (mm) | 2 | Spindle Speed(min-1) | FeedRate (mm/min) | ap(mm) | ae(mm) |
| 0,2 | 0,10 | 40.000 | 100 | 0,001 | 0,001 |
| 0,3 | 0,15 | 40.000 | 150 | 0,002 | 0,001 |
| 0,5 | 0,25 | 40.000 | 200 | 0,003 | 0,001 |
| 1,0 | 0,55 | 40.000 | 400 | 0,005 | 0,003 |
| 2,0 | 0,55 | 40.000 | 600 | 0,010 | 0,005 |
 Общий каталог Sumitomo 2012
 Каталог Sumitomo резьбонарезной инструмент
 Каталог Sumitomo пластины с режущей кромкой-моноалмаз Sumicristal
 Каталог Sumitomo инструмент для обработки канавок
 Общий каталог Sumitomo 2019 - 2020
 Каталог Sumitomo запасные части