Общий каталог Sumitomo 2018 - 2019 - страница 550
Навигация
 Общий каталог Sumitomo 2012
 Каталог Sumitomo резьбонарезной инструмент
 Каталог Sumitomo пластины с режущей кромкой-моноалмаз Sumicristal
 Каталог Sumitomo инструмент для обработки канавок
 Общий каталог Sumitomo 2019 - 2020
 Каталог Sumitomo запасные части
- Pages 3-6_CS6_EN_web
- A 1-20 insert selection EN_web
- B 1-14 grades_EN_web
- C01-17 inserts intro pages_EN_web
- C18-56 negative inserts_EN_web
- C57-86 positive inserts_EN_web
- D 1-46 tool holders_EN_web
- E 1-24 boring bars_EN_web
- F 1-48 grooving_thread tools_EN_web
- G 1-54 milling cutters_EN_web
- H 1-48 insert type endmills_EN_web
- J 1-24 new endmills_EN_web
- J 25-50 endmills_EN_web
- K 1-46 Multi-Drills_EN_web
- K 47-76 Multi-Drills_EN_web
- L 1-28 cbn_pcd grades_EN_web
- M 1-34 cbn_pcd inserts_EN_web
- M 35-56 SHM tools_EN_web
- N1-24 technical guidance_EN_web
- P 1-8 spare parts_neu_EN_web
- P 9-22 index_notes_EN_web
SUMIBORON ”MOULD Finish Master”
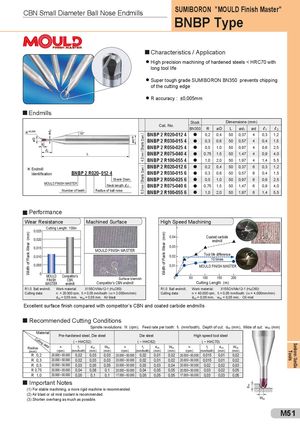
CBN Small Diameter Ball Nose Endmills BNBP Type
Characteristics / Application
l High precision machining of hardened steels < HRC70 with
long tool life
l Super tough grade SUMIBORON BN350 prevents chipping
of the cutting edge
l R accuracy : ±0,005mm
Endmills
| Stock | Dime | nsions( | mm) | ||||||
| Cat. No. | |||||||||
| BN350 | R | øD | L | ød1 | ød | l1 | l2 | ||
| am.) | BNBP 2 R020-012 4 | l | 0,2 | 0,4 | 50 | 0,37 | 4 | 0,3 | 1,2 |
| nkDi | BNBP 2 R030-015 4 | l | 0,3 | 0,6 | 50 | 0,57 | 4 | 0,4 | 1,5 |
| Sha | BNBP 2 R050-025 4 | l | 0,5 | 1,0 | 50 | 0,97 | 4 | 0,6 | 2,5 |
| mm( | BNBP 2 R075-040 4 | l | 0,75 | 1,5 | 50 | 1,47 | 4 | 0,9 | 4,0 |
| 4,0 | BNBP 2 R100-055 4 | l | 1,0 | 2,0 | 50 | 1,97 | 4 | 1,4 | 5,5 |
| am.) | BNBP 2 R020-012 6 | l | 0,2 | 0,4 | 50 | 0,37 | 6 | 0,3 | 1,2 |
| nkDi | BNBP 2 R030-015 6 | l | 0,3 | 0,6 | 50 | 0,57 | 6 | 0,4 | 1,5 |
| Sha | BNBP 2 R050-025 6 | l | 0,5 | 1,0 | 50 | 0,97 | 6 | 0,6 | 2,5 |
| mm( | BNBP 2 R075-040 6 | l | 0,75 | 1,5 | 50 | 1,47 | 6 | 0,9 | 4,0 |
| 6,0 | BNBP 2 R100-055 6 | l | 1,0 | 2,0 | 50 | 1,97 | 6 | 1,4 | 5,5 |
h Endmill
Performance
Wear Resistance Machined Surface High Speed Machining
Cutting Length: 100m -- 0,025 0,04 -- Coated carbide 0,020 endmill
0,015 0,03 -- MOULD FINISH MASTER Tool life difference 0,010 0,02 -- 10 times
0,005 0,01 -- MOULD FINISH MASTER
0 MOULD Competitor’s llll
| FINISH | CBN | Surface blemish | 0 50 100 150 200 | ||
| MASTER | endmill | Competitor’s CBN endmill | Cutting Length (m) |
| R1,0 Ball endmill, Work material: | X155CrVMo12-1 (H C60) X155CrVMo12-1 (H C60) R1,0 Ball endmill, Work material: |
| R R | |
| Cutting data: | n = 40.000 rpm, f t = 0,05 mm/tooth (vf = 4.000mm/min) n = 20.000 rpm, f t = 0,05 mm/tooth (v f = 2.000mm/min) Cutting data: |
| doc = 0,05 mm, woc = 0,05 mm, Air blast | doc = 0,05 mm, w oc = 0,05 mm, Oil mist |
| Excellent surface finish compared with competitor’s CBN and coated carbide endmills | |
| Recommended Cutting Conditions |
| Spindle revolutions: N (rpm), Feed rate per tooth: f (mm/tooth), Depth of cut: d | (mm), Wide of cut: w | (mm) | |
| t | oc | oc |
| Material Cutting d | Pre-har | (~ HRC5 dened ste | 2) el, Die s | teel | (~ HRC6 Die ste | 2) el | High | (~ HRC speed to | 70) ol steel | ||||
| Rad (m | ata ius m) | n (rpm) | ft (mm/tooth) | doc (mm) | Woc (mm) | n (rpm) | ft (mm/tooth) | doc (mm) | Woc (mm) | n (rpm) | ft (mm/tooth) | doc (mm) | Woc (mm) |
| R | 0,2 | 20.000~50.000 | 0,02 | 0,03 | 0,03 | 20.000~50.000 | 0,02 | 0,01 | 0,02 | 20.000~50.000 | 0,015 | 0,01 | 0,02 |
| R | 0,3 | 20.000~50.000 | 0,02 | 0,03 | 0,03 | 20.000~50.000 | 0,02 | 0,01 | 0,02 | 20.000~50.000 | 0,015 | 0,01 | 0,02 |
| R | 0,5 | 20.000~50.000 | 0,03 | 0,05 | 0,05 | 20.000~50.000 | 0,03 | 0,03 | 0,04 | 20.000~50.000 | 0,02 | 0,02 | 0,03 |
| R | 0,75 | 20.000~50.000 | 0,04 | 0,08 | 0,1 | 20.000~50.000 | 0,04 | 0,05 | 0,05 | 20.000~50.000 | 0,03 | 0,02 | 0,05 |
| R | 1,0 | 20.000~50.000 | 0,05 | 0,1 | 0,1 | 17.000~50.000 | 0,05 | 0,05 | 0,05 | 17.000~50.000 | 0,03 | 0,03 | 0,05 |
Important Notes
(1) For stable machining, a more rigid machine is recommended. (2) Air blast or oil mist coolant is recommended. (3) Shorten overhang as much as possible. Woc