Общий каталог Sumitomo 2018 - 2019 - страница 547
Навигация
 Общий каталог Sumitomo 2012
 Каталог Sumitomo резьбонарезной инструмент
 Каталог Sumitomo пластины с режущей кромкой-моноалмаз Sumicristal
 Каталог Sumitomo инструмент для обработки канавок
 Общий каталог Sumitomo 2019 - 2020
 Каталог Sumitomo запасные части
- Pages 3-6_CS6_EN_web
- A 1-20 insert selection EN_web
- B 1-14 grades_EN_web
- C01-17 inserts intro pages_EN_web
- C18-56 negative inserts_EN_web
- C57-86 positive inserts_EN_web
- D 1-46 tool holders_EN_web
- E 1-24 boring bars_EN_web
- F 1-48 grooving_thread tools_EN_web
- G 1-54 milling cutters_EN_web
- H 1-48 insert type endmills_EN_web
- J 1-24 new endmills_EN_web
- J 25-50 endmills_EN_web
- K 1-46 Multi-Drills_EN_web
- K 47-76 Multi-Drills_EN_web
- L 1-28 cbn_pcd grades_EN_web
- M 1-34 cbn_pcd inserts_EN_web
- M 35-56 SHM tools_EN_web
- N1-24 technical guidance_EN_web
- P 1-8 spare parts_neu_EN_web
- P 9-22 index_notes_EN_web
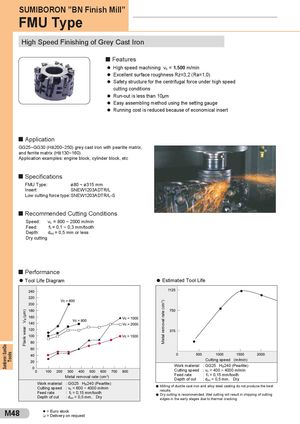
High Speed Finishing of Grey Cast Iron
Features
| l | High speed machining vc = 1.500 m/min |
| l | Excellent surface roughness Rz=3,2 (Ra=1,0) |
| l | Safety structure for the centrifugal force under high speed |
| cutting conditions | |
| l | Run-out is less than 10µm |
| l | Easy assembling method using the setting gauge |
| l | Running cost is reduced because of economical insert |
Application
GG25~GG30 (HB200~250) grey cast iron with pearlite matrix, and ferrite matrix (HB130~160) Application examples: engine block, cylinder block, etc
Specifications
FMU Type: ø80 ~ ø315 mm Insert: SNEW1203ADTR/L Low cutting force type: SNEW1203ADTR/L-S
Recommended Cutting Conditions
Speed: vc = 800 ~ 2000 m/min Feed: f = 0,1 ~ 0,3 mm/tooth t Depth: d = 0,5 mm or less oc Dry cutting
Performance
l Tool Life Diagram l Estimated Tool Life
Cutting speed (m/min) Work material : GG25 H 240 (Pearlite) B Cutting speed : v = 400 ~ 4000 m/min c Feed rate : f = 0,15 mm/tooth Metal removal rate (cm3) t
Depth of cut : d = 0,5 mm, Dry
oc Work material : GG25 H 240 (Pearlite) B Milling of ductile cast iron and alloy steel casting do not produce the best Cutting speed : v = 600 ~ 4000 m/min l
c results. Feed rate : f = 0,15 mm/tooth t Dry cutting is recommended. Wet cutting will result in chipping of cutting
Depth of cut : d = 0,5 mm, Dry l
oc edges in the early stages due to thermal cracking.