Общий каталог Sumitomo 2018 - 2019 - страница 493
Навигация
 Общий каталог Sumitomo 2012
 Каталог Sumitomo резьбонарезной инструмент
 Каталог Sumitomo пластины с режущей кромкой-моноалмаз Sumicristal
 Каталог Sumitomo инструмент для обработки канавок
 Общий каталог Sumitomo 2019 - 2020
 Каталог Sumitomo запасные части
- Pages 3-6_CS6_EN_web
- A 1-20 insert selection EN_web
- B 1-14 grades_EN_web
- C01-17 inserts intro pages_EN_web
- C18-56 negative inserts_EN_web
- C57-86 positive inserts_EN_web
- D 1-46 tool holders_EN_web
- E 1-24 boring bars_EN_web
- F 1-48 grooving_thread tools_EN_web
- G 1-54 milling cutters_EN_web
- H 1-48 insert type endmills_EN_web
- J 1-24 new endmills_EN_web
- J 25-50 endmills_EN_web
- K 1-46 Multi-Drills_EN_web
- K 47-76 Multi-Drills_EN_web
- L 1-28 cbn_pcd grades_EN_web
- M 1-34 cbn_pcd inserts_EN_web
- M 35-56 SHM tools_EN_web
- N1-24 technical guidance_EN_web
- P 1-8 spare parts_neu_EN_web
- P 9-22 index_notes_EN_web
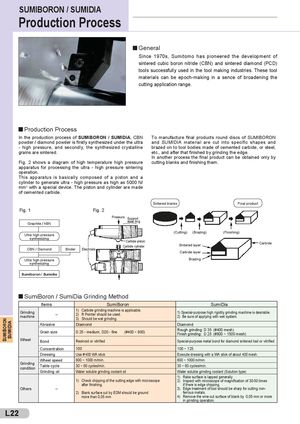
Production Process
General
Since 1970s, Sumitomo has pioneered the development of
sintered cubic boron nitride (CBN) and sintered diamond (PCD)
tools successfully used in the tool making industries. These tool
materials can be epoch-making in a sence of broadening the
cutting application range.
Production Process
| In the production process of SUMIBORON / SUMIDIA, CBN | To manufacture final products round discs of SUMIBORON |
| powder / diamond powder is firstly synthesized under the ultra | and SUMIDIA material are cut into specific shapes and |
| - high pressure, and secondly, the synthesized crystalline | brazed on to tool bodies made of cemented carbide, or steel, |
| grains are sintered. | etc., and after that finished by grinding the edge. |
| In another process the final product can be obtained only by | |
| Fig. 2 shows a diagram of high temperature high pressure | cutting blanks and finishing them. |
apparatus for processing the ultra - high pressure sintering operation. This apparatus is basically composed of a piston and a cylinder to generate ultra - high pressure as high as 5000 N/
mm 2 with a special device. The piston and cylinder are made of cemented carbide. Sintered blanks Final product Fig. 1 Fig. 2 Pressure Support Graphite / hBN steel ring (Cutting) (Brazing) (Finishing) Ultra high pressure synthesizing Carbide piston Carbide Carbide cylinder Sintered layer
CBN / Diamond Binder Electrode
Carbide layer Ultra high pressure Brazing synthesizing Sumiboron / Sumidia
SumiBoron / SumiDia Grinding Method
| Items | SumiBoron | SumiDia | |
| Grinding machine | – | 1) Carbide grinding machine is applicable. 2) R Pointer should be used. 3)Should be wetgrinding. | 1) Special-purpose high rigidity grinding machine is desirable. 2) Be sure of applying with wet system. |
| Abrasive | Diamond | Diamond | |
| Grain size | D 25 - medium, D20 - fine (#400 ~ 800) | Rough grinding: D 35 (#400 mesh) Finish grinding: D 25 (#800~1500 mesh) | |
| Wheel | Bond | Resinoid or vitrified | Special-purpose metal bond for diamond sintered tool or vitrified |
| Concentration | 100 | 100 ~ 125 | |
| Dressing | Use #400 WA stick | Execute dressingwith a WA stick of about 400 mesh. | |
| Wheel speed | 800 ~ 1000 m/min. | 800 ~ 1000 m/min. | |
| Grinding condition | Table cycle | 30 ~ 60 cycles/min. | 30 ~ 60 cycles/min. |
| Grindingoil | Water solublegrindingcoolant oil | Water solublegrindingcoolant(Solution type) | |
| Others | – | 1) Check chipping of the cutting edge with microscope after finishing. 2) Blank surface cut by EDM should be ground more than 0,05 mm | 1) Rake surface is lapped generally 2) Inspect with microscope of magnification of 30-50 times if there is edge chipping. 3) Edge treatment of tool should be sharp for cutting non- ferrous metals. 4) Remove the wire-cut surface of blank by 0,05 mm or more ingrinding operation. |