Общий каталог Sumitomo 2018 - 2019 - страница 486
Навигация
 Общий каталог Sumitomo 2012
 Каталог Sumitomo резьбонарезной инструмент
 Каталог Sumitomo пластины с режущей кромкой-моноалмаз Sumicristal
 Каталог Sumitomo инструмент для обработки канавок
 Общий каталог Sumitomo 2019 - 2020
 Каталог Sumitomo запасные части
- Pages 3-6_CS6_EN_web
- A 1-20 insert selection EN_web
- B 1-14 grades_EN_web
- C01-17 inserts intro pages_EN_web
- C18-56 negative inserts_EN_web
- C57-86 positive inserts_EN_web
- D 1-46 tool holders_EN_web
- E 1-24 boring bars_EN_web
- F 1-48 grooving_thread tools_EN_web
- G 1-54 milling cutters_EN_web
- H 1-48 insert type endmills_EN_web
- J 1-24 new endmills_EN_web
- J 25-50 endmills_EN_web
- K 1-46 Multi-Drills_EN_web
- K 47-76 Multi-Drills_EN_web
- L 1-28 cbn_pcd grades_EN_web
- M 1-34 cbn_pcd inserts_EN_web
- M 35-56 SHM tools_EN_web
- N1-24 technical guidance_EN_web
- P 1-8 spare parts_neu_EN_web
- P 9-22 index_notes_EN_web
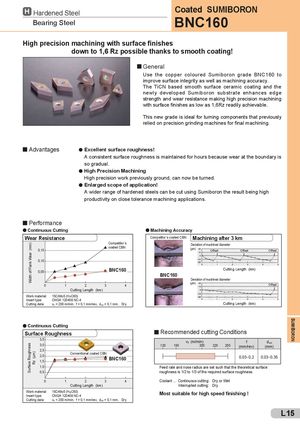
Hardened Steel BNC160
Bearing Steel
High precision machining with surface finishes
down to 1,6 Rz possible thanks to smooth coating!
General
Use the copper coloured Sumiboron grade BNC160 to
improve surface integrity as well as machining accuracy.
The TiCN based smooth surface ceramic coating and the
newly developed Sumiboron substrate enhances edge
strength and wear resistance making high precision machining
with surface finishes as low as 1,6Rz readily achievable.
This new grade is ideal for turning components that previously
relied on precision grinding machines for final machining.
Advantages Excellent surface roughness!
- l
A consistent surface roughness is maintained for hours because wear at the boundary is
so gradual.
l High Precision Machining
High precision work previously ground, can now be turned.
l Enlarged scope of application!
A wider range of hardened steels can be cut using Sumiboron the result being high
productivity on close tolerance machining applications.
Performance
Continuous Cutting Machining Accuracy
| Wear Resistance | Competitor´s coated CBN | Machining after 3 km | |
| Competitor´s | Deviation of machined diameter | ||
| coated CBN | (µm) |
0,15 - Offset Offset Offset
0,10 - BNC160 Cutting Length (km) 0,05 - BNC160 Deviation of machined diameter
llll (µm) 0 1 2 3 4 Offset Cutting Length (km) Work material: 15CrMo5 (HRC60) Insert type: CNGA 120408 NC-4
Cutting data: v = 200 m/min, f = 0,1 mm/rev, d = 0,1 mm, Dry Cutting Length (km)
c oc
Continuous Cutting
Recommended cutting Conditions
Surface Roughness -
| vc(m/min) 120 150 200 220 250 l l l l l | f (mm/rev) | doc (mm) |
| 0,03-0,2 | 0,03-0,35 | |
| Feed rate and nose radius are set such that th roughness is 1/2 to 1/3 of the required surface | e theoretical s roughness. | urface |
| Coolant ... Continuous cutting: Dry or Wet Interrupted cutting: Dry |
Conventional coated CBN 1,5 -
0 1 2 3 4 Work material: 15CrMo5 (HRC60) Most suitable for high speed finishing ! Insert type: CNGA 120408 NC-4 Cutting data: vc = 200 m/min, f = 0,1 mm/rev, doc = 0,1 mm, Dry