Общий каталог Sumitomo 2018 - 2019 - страница 333
Навигация
 Общий каталог Sumitomo 2012
 Каталог Sumitomo резьбонарезной инструмент
 Каталог Sumitomo пластины с режущей кромкой-моноалмаз Sumicristal
 Каталог Sumitomo инструмент для обработки канавок
 Общий каталог Sumitomo 2019 - 2020
 Каталог Sumitomo запасные части
- Pages 3-6_CS6_EN_web
- A 1-20 insert selection EN_web
- B 1-14 grades_EN_web
- C01-17 inserts intro pages_EN_web
- C18-56 negative inserts_EN_web
- C57-86 positive inserts_EN_web
- D 1-46 tool holders_EN_web
- E 1-24 boring bars_EN_web
- F 1-48 grooving_thread tools_EN_web
- G 1-54 milling cutters_EN_web
- H 1-48 insert type endmills_EN_web
- J 1-24 new endmills_EN_web
- J 25-50 endmills_EN_web
- K 1-46 Multi-Drills_EN_web
- K 47-76 Multi-Drills_EN_web
- L 1-28 cbn_pcd grades_EN_web
- M 1-34 cbn_pcd inserts_EN_web
- M 35-56 SHM tools_EN_web
- N1-24 technical guidance_EN_web
- P 1-8 spare parts_neu_EN_web
- P 9-22 index_notes_EN_web
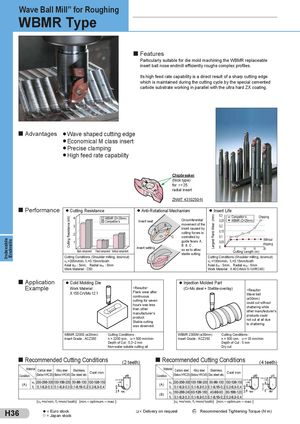
Wave Ball Mill” for Roughing
WBMR Type
Features
Particularly suitable for die mold machining the WBMR replaceable
insert ball nose endmill efficiently roughs complex profiles.
Its high feed rate capability is a direct result of a sharp cutting edge
which is maintained during the cutting cycle by the special cemented
carbide substrate working in parallel with the ultra hard ZX coating.
Advantages Wave shaped cutting edge
l
Economical M class insert
l
Precise clamping
l
High feed rate capability
l
Chipbreaker
(Nick type)
for r= 25
radial insert
ZNMT 4310250-N
Performance Cutting Resistance Anti-Rotational Mechanism Insert Life
l l l
0,3 Competitor’s Chipping
4 WBMR (D=25mm) Circumferential
Competitor’s Insert seat 0,25 WBMR (D=25mm)
| 3 | B movement of the | 0,2 |
| A insert caused by | ||
| cutting forces is | 0,15 | |
| 2 | ||
| C controlled by | 0,1 | |
| guide faces A, | Without | |
| 1 | 0,05 | |
| B & C , | chipping | |
| Insert setting | 0 | |
| Back component Feed component Vertical component | so as to allow | 5 10 15 20 |
| Cutting Length (m) | ||
| Indexable Endmills | stable cutting. | |
| Cutting Conditions (Shoulder milling, downcut) | Cutting Conditions (Shoulder milling, downcut) | |
| v c =200m/min, f t =0.15mm/tooth | vc =100m/min, f t =0.15mm/tooth | |
| Axial d oc : 5mm, Radial woc : 5mm | Axial doc : 5mm, Radial woc : 5mm | |
| Work Material : C50 | Work Material : X 40 CrMoV 5-1(HRC45) | |
| Cold Molding Die Application | Injection Molded Part | |
| l Example | l | |
| Work Material : <Results> | (Cr-Mo steel + Stellite-overlay) | |
| Flank wear after | <Results> | |
| X 155 CrVMo 12 1 | Wave ball | |
| continuous | (ø30mm) | |
| cutting for seven | ||
| hours was less | could cut without | |
| than other | chattering while | |
| manufacturer‘s | other manufacturer‘s | |
| products could | ||
| product. | not cut at all due | |
| Stable cutting | ||
| was observed. | to chattering. | |
| Cutting Conditions : WBMR 2200S (ø20mm) | WBMR 2300M (ø30mm) | Cutting Conditions : |
| n = 2200 rpm, v = 500 mm/min Insert Grade : ACZ350 | Insert Grade : ACZ350 | n = 500 rpm, v = 35 mm/min |
f f Depth of Cut : 0,3~2 mm Depth of Cut : 5 mm Non-water soluble cutting oil Dry cut Recommended Cutting Conditions Recommended Cutting Conditions
(2 teeth) (4 teeth)
| Material | Carbon steel | Stainless, Alloy steel | Material | Stainless, Alloy steel Carbon steel | |
| Condition | (Below HRC25)(Below HRC45) Die steel etc. Cast iron | Condition | (Below HRC25)(Below HRC45) Die steel etc. Cast iron | ||
| vc 200-250-300100-150-200 50-80-100 100-120-150 | vc 200-250-300100-150-200 50-80-100 100-120-150 | ||||
| (A) | (A) | ||||
| f t | 0,1-0,2-0,3 0,1-0,2-0,3 0,1-0,15-0,2 0,2-0,3-0,4 | f t 0,1-0,2-0,3 0,1-0,2-0,3 0,1-0,15-0,2 0,2-0,3-0,4 | |||
| vc 160-200-240 80-120-160 40-60-80 80-100-120 | |||||
| (B) | |||||
| f t 0,1-0,2-0,3 0,1-0,2-0,3 0,1-0,15-0,2 0,2-0,3-0,4 | |||||
| [vc =m/min, ft =mm/ tooth] [min.– optimum – max.] | [vc =m/min, ft =mm/ tooth] [min.– optimum – max.] |
H36 l = Euro stock = Delivery on request Recommended Tightening Torque (N·m)