Общий каталог Sumitomo 2018 - 2019 - страница 288
Навигация
 Общий каталог Sumitomo 2012
 Каталог Sumitomo резьбонарезной инструмент
 Каталог Sumitomo пластины с режущей кромкой-моноалмаз Sumicristal
 Каталог Sumitomo инструмент для обработки канавок
 Общий каталог Sumitomo 2019 - 2020
 Каталог Sumitomo запасные части
- Pages 3-6_CS6_EN_web
- A 1-20 insert selection EN_web
- B 1-14 grades_EN_web
- C01-17 inserts intro pages_EN_web
- C18-56 negative inserts_EN_web
- C57-86 positive inserts_EN_web
- D 1-46 tool holders_EN_web
- E 1-24 boring bars_EN_web
- F 1-48 grooving_thread tools_EN_web
- G 1-54 milling cutters_EN_web
- H 1-48 insert type endmills_EN_web
- J 1-24 new endmills_EN_web
- J 25-50 endmills_EN_web
- K 1-46 Multi-Drills_EN_web
- K 47-76 Multi-Drills_EN_web
- L 1-28 cbn_pcd grades_EN_web
- M 1-34 cbn_pcd inserts_EN_web
- M 35-56 SHM tools_EN_web
- N1-24 technical guidance_EN_web
- P 1-8 spare parts_neu_EN_web
- P 9-22 index_notes_EN_web
WFXH Type
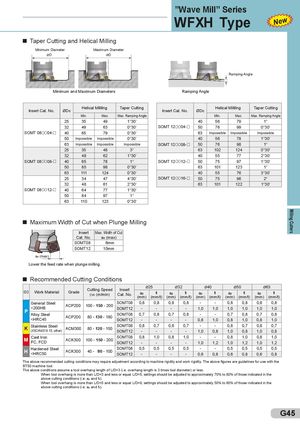
Taper Cutting and Helical Milling
Minimum Diameter Maximum Diameter ØD ØD
Ramping Angle
Minimum and Maximum Diameters Ramping Angle
| Insert Cat. No. | ØDc | Helical | Millilng | Taper Cutting |
| Min. | Max. | Max. Ramping Angle | ||
| 25 | 35 | 49 | 1°30‘ | |
| 32 | 49 | 63 | 0°30‘ | |
| SOMT 08 04- | 40 | 65 | 79 | 0°30‘ |
| 50 | Impossible | Impossible | 0°30‘ | |
| 63 | Impossible | Impossible | Impossible | |
| 25 | 35 | 48 | 3° | |
| 32 | 49 | 62 | 1°30‘ | |
| SOMT 08 08- | 40 | 65 | 78 | 1° |
| 50 | 85 | 98 | 0°30‘ | |
| 63 | 111 | 124 | 0°30‘ | |
| 25 | 34 | 47 | 4°30‘ | |
| 32 | 48 | 61 | 2°30‘ | |
| SOMT 08 12- | 40 | 64 | 77 | 1°30‘ |
| 50 | 84 | 97 | 1° | |
| 63 | 110 | 123 | 0°30‘ |
| Insert Cat. No. | ØDc | Helical | Millilng | Taper Cutting |
| Min. | Max. | Max. Ramping Angle | ||
| 40 | 56 | 79 | 1° | |
| SOMT 12 04- | 50 | 76 | 99 | 0°30‘ |
| 63 | Impossible | Impossible | Impossible | |
| 40 | 56 | 78 | 1°30‘ | |
| SOMT 12 08- | 50 | 76 | 98 | 1° |
| 63 | 102 | 124 | 0°30‘ | |
| 40 | 55 | 77 | 2°30‘ | |
| SOMT 12 12- | 50 | 75 | 97 | 1°30‘ |
| 63 | 101 | 123 | 1° | |
| 40 | 55 | 76 | 3°30‘ | |
| SOMT 12 16- | 50 | 75 | 96 | 2° |
| 63 | 101 | 122 | 1°30‘ |
Maximum Width of Cut when Plunge Milling
| Insert | Max. Width of Cut |
| Cat. No. | ae (max) |
| SOMT08 | 6mm |
| SOMT12 | 10mm |
ae (max) Lower the feed rate when plunge milling.
Recommended Cutting Conditions
| Cuttin Seed | Insert | Ø | 25 | Ø | 32 | Ø | 40 | Ø | 50 | Ø | 63 | |||
| ISO | Wk Mil | Gd | g p | |||||||||||
| or atera | rae | (vc(m/min) | Cat. No. | ap (mm) | ft (mm/t) | ap (mm) | ft (mm/t) | ap (mm) | ft (mm/t) | ap (mm) | ft (mm/t) | ap (mm) | ft (mm/t) | |
| General Steel | SOMT08 | 0,8 | 0,8 | 0,8 | 0,8 | - | - | 0,8 | 0,8 | 0,8 | 0,8 | |||
| P | ACP200 | 100 -150- 200 | SOMT12 | - | - | - | - | 1,0 | 1,0 | 1,0 | 1,0 | 1,0 | 1,0 | |
| Alloy Steel | ACP200 | 80130180 | SOMT08 | 0,7 | 0,8 | 0,7 | 0,8 | - | - | 0,7 | 0,8 | 0,7 | 0,8 | |
| -- | SOMT12 | - | - | - | - | 0,8 | 1,0 | 0,8 | 1,0 | 0,8 | 1,0 | |||
| K | Stainless Steel | ACM300 | 80120150 | SOMT08 | 0,8 | 0,7 | 0,8 | 0,7 | - | - | 0,8 | 0,7 | 0,8 | 0,7 |
| ( | X5CrNiS18 10, other) | -- | SOMT12 | - | - | - | - | 1,0 | 0,8 | 1,0 | 0,8 | 1,0 | 0,8 | |
| M | Cast Iron | ACK | 112 | SOMT08 | 0,8 | 1,0 | 0,8 | 1,0 | - | - | 0,8 | 1,0 | 0,8 | 1,0 |
| FC, FCD | 300 | 00 -50- 00 | SOMT12 | - | - | - | - | 1,0 | 1,2 | 1,0 | 1,2 | 1,0 | 1,2 | |
| Hardened Steel | SOMT08 | 0,5 | 0,5 | 0,5 | 0,5 | - | - | 0,5 | 0,5 | 0,5 | 0,5 | |||
| H | ACK300 | 40 -80- 100 | SOMT12 | - | - | - | - | 0,6 | 0,8 | 0,6 | 0,8 | 0,6 | 0,8 |
The above recommended cutting conditions may require adjustment according to machine rigidity and work rigidity. The above figures are guidelines for use with the BT50 machine tool. The above conditions assume a tool overhang length of L/D=3 (i.e. overhang length is 3 times tool diameter) or less. When tool overhang is more than L/D=3 and less or equal L/D=5, settings should be adjusted to approximately 70% to 80% of those indicated in the above cutting conditions (i.e. ap and fz). When tool overhang is more than L/D=5 and less or equal L/D=8, settings should be adjusted to approximately 50% to 60% of those indicated in the above cutting conditions (i.e. ap and fz).