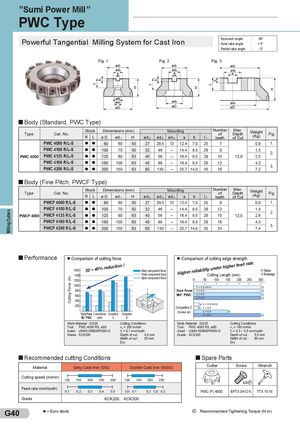
PWC Type
| Powerful Tangential Milling System for Cast Iron | Approach angle | : 88° | |
| Axial rake angle | : + 5° | |
| Radial rake angle : | | - 5° |
Fig. 1 Fig. 2 Fig. 3
Body (Standard, PWC Type)
| Type | Cat. No. | Sto | ck | Dime | nsions( | mm) | | | Moun | ting | | | Number of | Max. Depth | Weight K | Fig. |
| | R | L | ø D | ød1 | H | ød2 | ød3 | ød4 | a | b | l1 | teeth | of Cut | (g) | |
| PWC 4080 R/L-S | l | l | 80 | 60 | 50 | 27 | 29,5 | 13 | 12,4 | 7,0 | 25 | 7 | | 0,9 | 1. |
| PWC 4100 R/L-S | l | l | 100 | 70 | 50 | 32 | 46 | – | 14,4 | 8,5 | 29 | 8 | | 1,3 | |
| PWC 4000 | PWC 4125 R/L-S | l | l | 125 | 80 | 63 | 40 | 56 | – | 16,4 | 9,5 | 29 | 10 | 12,0 | 2,5 | 2. |
| PWC 4160 R/L-S | l | l | 160 | 100 | 63 | 40 | 88 | – | 16,4 | 9,5 | 29 | 12 | | 4,2 | |
| PWC 4200 R/L-S | l | l | 200 | 150 | 63 | 60 | 130 | – | 25,7 | 14,0 | 35 | 16 | | 7,2 | 3. |
Body (Fine Pitch, PWCF Type)
| Type | Cat. No. | R L Stock | ø D Dime | ød1 nsions( | H mm) | ød2 | ød3 | ød4 Moun | a ting | b | l1 | Number of teeth | Max. Depth of Cut | Weight (Kg) | Fig. |
| PWCF 4080 R/L-S | l l | 80 | 60 | 50 | 27 | 29,5 | 13 | 12,4 | 7,0 | 25 | 9 | | 0,9 | 1. |
| PWCF 4100 R/L-S | l l | 100 | 70 | 50 | 32 | 46 | – | 14,4 | 8,5 | 29 | 12 | | 1,4 | |
| PWCF 4000 | PWCF 4125 R/L-S | l l | 125 | 80 | 63 | 40 | 56 | – | 16,4 | 9,5 | 29 | 15 | 12,0 | 2,6 | 2. |
| PWCF 4160 R/L-S | l l | 160 | 100 | 63 | 40 | 88 | – | 16,4 | 9,5 | 29 | 18 | | 4,3 | |
| PWCF 4200 R/L-S | l l | 200 | 150 | 63 | 60 | 130 | – | 25,7 | 14,0 | 35 | 24 | | 7,4 | 3. |
| Performance Comparison of cutting force | | Comparison of cutting edge strength | | | |
| l | | l | | | |
| 1600 - | 20 ~ 40% reduction ! Main component force | Higher reliability under higher feed rate. | | | Stable |
| 1400- | Feed component force | | | Cutting Length (mm) | Breakage |
| Back component force | | 0 | 50 100 150 200 250 300 | |
| 1200 - | | | | | |
| 1000 - | | | lllll l | | |
| | | ft = 0,5 (N=2) | | |
| 800 - | ”Sumi Power | f = 0,5 |
| | t |
| 600 - | Mill” PWC | ft = 0,4 |
| | f = 0,3 |
| 400 - | | t |
| 200 - | | f t = 0,5 (N=2) |
| | | | Competitor C | f = 0,5 | |
| . | | | | t | |
| ”Sumi Power Conventional | Competitor Competitor | | (Screw on) | f t = 0,4 | |
| | | | | f = 0,3 | |
| Mill” PWC | A cutter | B | | t | |
| Work Material : GG25 | | Cutting Conditions | | Work Material : GG25 | | Cutting Conditions |
| Tool : PWC 4080 RS, ø80 | | v | = 200 m/min | Tool : PWC 4080 RS, ø80 | | v = 160 m/min |
| | | c | | | c |
| Insert : LNMX160608PNSN-G | | f t = 0,1 mm/tooth | | Insert : LNMX160608PNSN-G | | f t = 0,3 ~ 0,5 mm/tooth |
| Grade : ACK200 | | Depth of cut : 4,0 mm | | Grade : ACK200 | | Depth of cut : 5,0 mm |
| | Width of cut : | | 50 mm | | 80 mm Width of cut : |
| | Dry | | | | Dry |
| Recommended cutting Conditions | | | | | Spare Parts | |
Material Grey Cast Iron (GG) Ductile Cast Iron (GGG) Cutter Screw Wrench
| Cutting speed (m/min) | l————————––——l | l—————————l | | | |
| 100 150 200 250 300 | 100 150 200 250 | | | 3,0 |
| Feed rate (mm/tooth) | l————————––——l | l—————————l | | | |
| 0,1 0,2 0,3 0,4 0,5 | 0,05 0,1 0,2 0,25 0,3 | PWC (F) 4000 | BFTX 0412 N TTX 15 W | |
Grade ACK200, ACK300
 Общий каталог Sumitomo 2012
 Каталог Sumitomo резьбонарезной инструмент
 Каталог Sumitomo пластины с режущей кромкой-моноалмаз Sumicristal
 Каталог Sumitomo инструмент для обработки канавок
 Общий каталог Sumitomo 2019 - 2020
 Каталог Sumitomo запасные части