Каталог Stellram токарный инструмент - страница 264
Навигация
 Каталог Stellram материалы и сплавы
 Каталог Stellram твердосплавные цельные фрезы
 Каталог Stellram фрез со сменными пластинами
 Каталог Stellram высокопроизводительные фрезерные системы
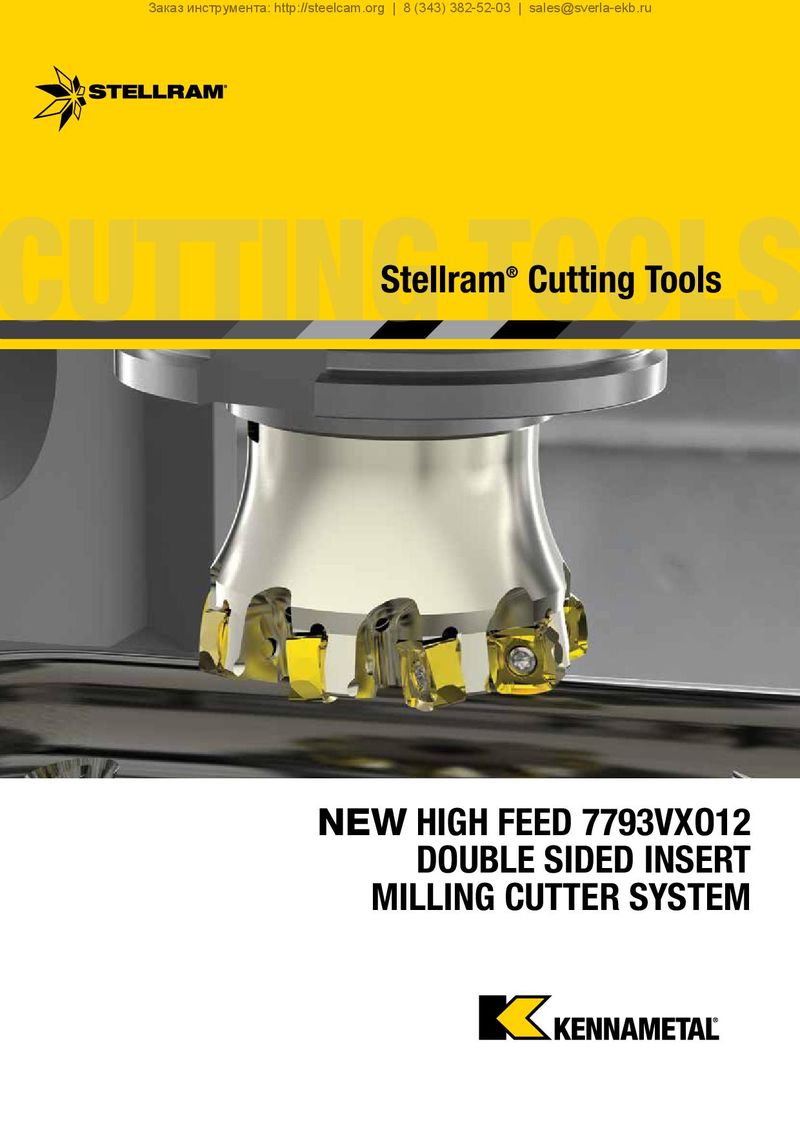 Каталог Stellram системы со сменными пластинами для фрезерования с высокими подачами

Threading Checklist
5 Select Anvil 6 Select Cutting Speed
Note: The 1.5° angle is Standard with
all toolholders Cutting Speed vc
PVD
1.5° Standard 1.5° Standard SP4066
| ISO | Materials | Rm and Hardness | m/min |
| min. - max. | |||
| <600 N/mm2 |
β β <180 HBN 230 - 485
Unalloyed Steel <950 N/mm2 <280 HBN 150 - 315 P 700-950 N/mm 2
200-280 HBN 135 - 290 Negative Helix Alloyed 950-1200 N/mm 2
| Steel | 280-355 HBN | 115 -240 | |
| ß Helix Angle | |||
| 1200-1400 N/mm2 |
| Insert size | 4.5° | 3.5° | 2.5° | 1.5° | 0.5° | 0° | -0.5° | -1.5° 355-415 HBN | 75 - 165 | |||
| Toolholder | ||||||||||||
| mm | Inch | Anvil Part Numbers | ||||||||||
| EX RH / IN LH | YE33P | YE32P | YE31P | YE3 | YE31N | YE31.5N | YE32N | YE33N | Austenitic + Ferritic | |||
| 16 | 3/8" | 300 series | 155 - 330 | |||||||||
| EX LH / IN RH | YI33P | YI32P | YI31P | YI3 | YI31N | YI31.5N | StainlessYI32N YI33N | |||||
| Steel | Martensitic | |||||||||||
| EX RH / IN LH | YE43P | YE42P | YE41P | YE4 | YE41N | YE41.5NM | YE42N | YE43N | ||||
| 22 | 1/2" | 400 series | 160 - 340 | |||||||||
| EX LH / IN RH | YI43P | YI42P | YI41P | YI4 | YI41N | YI41.5N | YI42N | YI43N | ||||
| EX RH / IN LH | YE4U3P | YE4U2P | YE4U1P | YE4U | YE4U1N | YE4U1.5N YE4U2NPH StainlessYE4U3N | Refractory | |||||
| 22U | 1/2" | P.H. 80 - 175 | ||||||||||
| EX LH / IN RH | YI4U3P | YI4U2P | YI4U1P | YI4U | YI4U1N | YI4U1.5N | YI4U2N | YI4U3N | ||||
| See page C205Grey | ||||||||||||
| EX RH / IN LH | YE53P | YE52P | YE51P | YE5 | YE51N | YE51.5N | YE52N | YE53N | GG-Ft 225 - 480 | |||
| 27 | 5/8" | |||||||||||
| EX LH / IN RH | YI53P | YI52P | YI51P | YI5 | YI51N | YI51.5N | YI52N | YI53N | ||||
| K | Cast Iron | Spheroidal-Ductile | ||||||||||
| EX RH / IN LH | YE5U3P | YE5U2P | YE5U1P | YE5U | YE5U1N | YE5U1.5N YE5U2N | YE5U3N | GGG-FGS | 195 - 415 | |||
| 27U | 5/8" | |||||||||||
| EX LH / IN RH | YI5U3P | YI5U2P | YI5U1P | YI5U | YI5U1N | YI5U1.5N | YI5U2N | YI5U3N | Malleable | |||
| GTS - MN/MP | 130 - 280 | |||||||||||
| See page C243 | 7 Select number and depth of passes | |||||||||||
| Iron Based | 35 - 70 | |||||||||||
| I.S.O Metric (ISO) 60°, External (mm)HighCobalt Based | 30 - 60 |
S Temperature Pitch (mm)Pitch (mm)
| Number of | 0,5 | 0,75 | 0,8 | 1,0 | 1,25 | 1,5 | 1,75 2,02,0 | 2,52,5 | 3,03,0 | 3,53,5 | 4,04,0 | 4,54,5 | 5,05,0 | 5,55,5 | 6,06,0 | |
| Passes | Alloys | Nickel Based | 30 - 60 | |||||||||||||
| Radial in-feed per pass (mm) | ||||||||||||||||
| 1 | 0,102 | 0,178 | 0,178 | 0,178 | 0,178 | 0,229 | 0,229 | 0,254 | 0,279 | 0,279 | 0,330 | 0,330 | 0,381 | 0,406 | 0,432 | 0,457 |
| 2 | 0,102 | 0,152 | Titanium Based0,1520,178 | 0,178 | 0,20345 - 950,203 | 0,229 | 0,254 | 0,254 | 0,305 | 0,330 | 0,330 | 0,381 | 0,406 | 0,432 | ||
| 3 | 0,076 | 0,102 | 0,127 | 0,127 | 0,152 | 0,178 | 0,152 | 0,178 | 0,203 | 0,203 | 0,254 | 0,254 | 0,279 | 0,330 | 0,330 | 0,356 |
| 4 | 0,076 | 0,076 | 0,076 | 0,102 | 0,127 | 0,152 | 0,152 | 0,152 | 0,178 | 0,178 | 0,203 | 0,229 | 0,229 | 0,279 | 0,279 | 0,305 |
| 5 | 0,356 | 0,508 | 0,533 | 0,076 | 0,102 | 0,127 | 0,127 | 0,152 | 0,152 | 0,152 | 0,178 | 0,178 | 0,229 | 0,229 | 0,229 | 0,279 |
| 6 | 0,660 | 0,076 | 0,076 | 0,102 | 0,127 | 0,127 | 0,152 | 0,178 | 0,178 | 0,203 | 0,229 | 0,229 | 0,229 | |||
| 7 | 0,813 | 0,965 | 0,102 | 0,102 | 0,127 | 0,127 | 0,152 | 0,152 | 0,178 | 0,203 | 0,203 | 0,229 | ||||
| 8 | 0,076 | 0,076 | 0,102 | 0,127 | 0,152 | 0,152 | 0,178 | 0,178 | 0,178 | 0,203 | ||||||
| 9 | 1,143 | 1,270 | 0,102 | 0,127 | 0,152 | 0,152 | 0,152 | 0,178 | 0,178 | 0,203 | ||||||
| 10 | 0,076 | 0,102 | 0,127 | 0,127 | 0,152 | 0,178 | 0,178 | 0,178 | ||||||||
| 11 | 1,600 | 0,102 | 0,102 | 0,127 | 0,152 | 0,152 | 0,152 | 0,178 | ||||||||
| 12 | 0,076 | 0,076 | 0,127 | 0,127 | 0,152 | 0,152 | 0,152 | |||||||||
| 13 | 1,880 | 2,210 | 0,102 | 0,127 | 0,127 | 0,127 | 0,152 | |||||||||
| 14 | 0,076 | 0,102 | 0,102 | 0,127 | 0,152 | |||||||||||
| 15 | See pages C251 – C259 | 2,515 | 2,819 | 3,124 | 0,127 | 0,127 | ||||||||||
| 16 | 0,102 | 0,102 |
3,429 3,734 Last pass equals total depth of thread.Last pass equals total depth of thread.