Каталог Stellram фрез со сменными пластинами - страница 257
Навигация
 Каталог Stellram твердосплавные цельные фрезы
 Каталог Stellram токарный инструмент
 Каталог Stellram системы со сменными пластинами для фрезерования с высокими подачами
 Каталог Stellram высокопроизводительные фрезерные системы
 Каталог Stellram материалы и сплавы
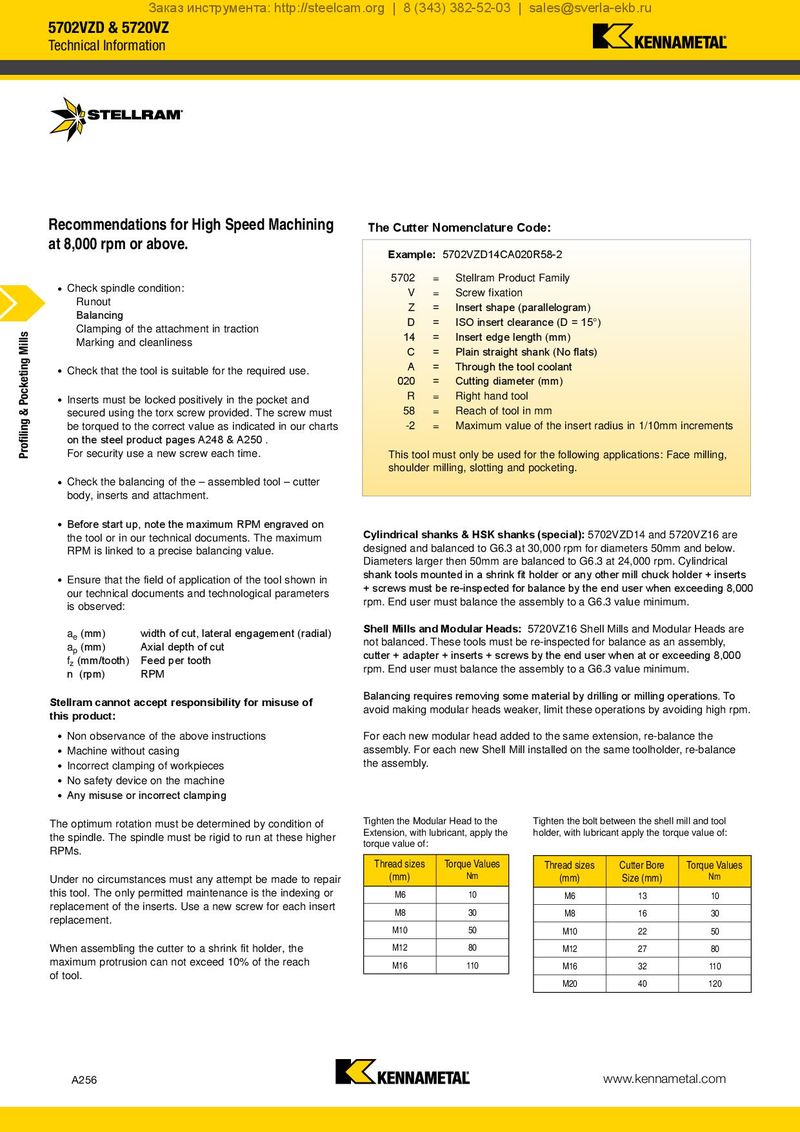
5702VZD & 5720VZ
Recommendations for High Speed Machining The Cutter Nomenclature Code: at 8,000 rpm or above.
Example: 5702VZD14CA020R58-2
5702 = Stellram Product Family
- Check spindle condition:
| V | = | Screw fixation | ||
| Runout | Z | = Insert shape (parallelogram) | ||
| Balancing | ||||
| D | = ISO insert clearance (D = 15°) | |||
| Clamping of the attachment in traction | 14 | = Insert edge length (mm) |
Marking and cleanliness C = Plain straight shank (No flats) A = Through the tool coolant
- Check that the tool is suitable for the required use.
020 = Cutting diameter (mm)
| • | R | = | Right hand tool | |
| Inserts must be locked positively in the pocket and | ||||
| secured using the torx screw provided. The screw must | 58 | = | Reach of tool in mm | |
| be torqued to the correct value as indicated in our charts | -2 | = | Maximum value of the insert radius in 1/10mm increments |
on the steel product pages A248 & A250 . For security use a new screw each time. This tool must only be used for the following applications: Face milling, shoulder milling, slotting and pocketing.
- Check the balancing of the – assembled tool – cutter
body, inserts and attachment.
- Before start up, note the maximum RPM engraved on
Cylindrical shanks & HSK shanks (special): 5702VZD14 and 5720VZ16 are the tool or in our technical documents. The maximum RPM is linked to a precise balancing value. designed and balanced to G6.3 at 30,000 rpm for diameters 50mm and below. Diameters larger then 50mm are balanced to G6.3 at 24,000 rpm. Cylindrical shank tools mounted in a shrink fit holder or any other mill chuck holder + inserts
- Ensure that the field of application of the tool shown in + screws must be re-inspected for balance by the end user when exceeding 8,000
our technical documents and technological parameters rpm. End user must balance the assembly to a G6.3 value minimum. is observed:
| (mm) | width of cut, lateral engagement (radial) | Shell Mills and Modular Heads: 5720VZ16 Shell Mills and Modular Heads are | |
| a | |||
| e | |||
| (mm) | Axial depth of cut | not balanced. These tools must be re-inspected for balance as an assembly, | |
| a | |||
| p | cutter + adapter + inserts + screws by the end user when at or exceeding 8,000 | ||
| f (mm/tooth) Feed per tooth | |||
| z | |||
| n (rpm) | RPM | rpm. End user must balance the assembly to a G6.3 value minimum. | |
| Balancing requires removing some material by drilling or milling operations. To | |||
| Stellram cannot accept responsibility for misuse of | |||
| this product: | avoid making modular heads weaker, limit these operations by avoiding high rpm. |
- Non observance of the above instructions For each new modular head added to the same extension, re-balance the
- Machine without casing assembly. For each new Shell Mill installed on the same toolholder, re-balance
- Incorrect clamping of workpieces the assembly.
- No safety device on the machine
- Any misuse or incorrect clamping
The optimum rotation must be determined by condition of Tighten the Modular Head to the Tighten the bolt between the shell mill and tool
Extension, with lubricant, apply the holder, with lubricant apply the torque value of: the spindle. The spindle must be rigid to run at these higher torque value of: RPMs.
| Thread sizes (mm) | Torque Values Nm | Thread sizes (mm) | Cutter Bore Size (mm) | Torque Values Nm |
| M6 | 10 | M6 | 13 | 10 |
| M8 | 30 | M8 | 16 | 30 |
| M10 | 50 | M10 | 22 | 50 |
| M12 | 80 | M12 | 27 | 80 |
| M16 | 110 | M16 | 32 | 110 |
| M20 | 40 | 120 |
Under no circumstances must any attempt be made to repair
replacement.