Каталог Stellram фрез со сменными пластинами - страница 249
Навигация
 Каталог Stellram твердосплавные цельные фрезы
 Каталог Stellram токарный инструмент
 Каталог Stellram системы со сменными пластинами для фрезерования с высокими подачами
 Каталог Stellram высокопроизводительные фрезерные системы
 Каталог Stellram материалы и сплавы
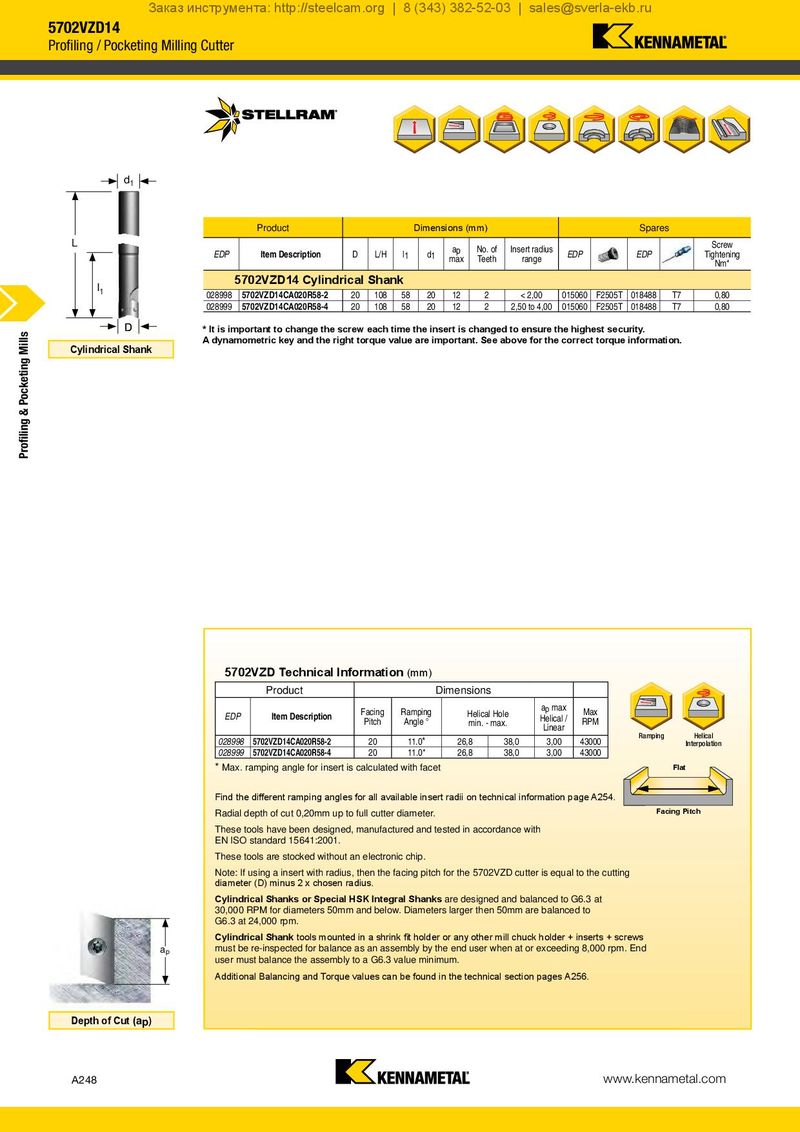
5702VZD14
Profiling / Pocketing Milling Cutter
| d1 | Product | Di | mens | ions ( | mm) | Spar | es | ||||||||
| L I1 | EDP | Item Description 5702VZD14 Cylind | D rical | L/H Shan | l1 k | d1 | ap max | No. of Teeth | Insert radius range | EDP | EDP | Screw Tightening Nm | |||
| 028998 | 5702VZD14CA020R58-2 | 20 | 108 | 58 | 20 | 12 | 2 | < 2,00 | 015060 | F2505T | 018488 | T7 | 0,80 | ||
| Cylindrica | D l Shank | 028999 It is im A dyna | 5702VZD14CA020R58-4 portant to change the s mometric key and the ri | 20 crew ght to | 108 each t rque v | 58 ime th alue a | 20 e ins re im | 12 ert is porta | 2 change nt. See a | 2,50 to 4,00 d to ensure t bove for the | 015060 he high correc | F2505T est sec t torque | 018488 urity. inform | T7 ation. | 0,80 |
5702VZD Technical Information (mm)
| Product | Dimensions | ||||
| amax | |||||
| EDP Item Description | Facing | Ramping ° Helical Hole | p Helical / | Max | |
| Pitch | Angle min. - max. | Linear | RPM | ||
| 028998 5702VZD14CA020R58-2 | 20 | 11.0 26,8 38,0 | 3,00 | 43000 | Ramping Helical Interpolation |
| 028999 5702VZD14CA020R58-4 | 20 | 11.0 26,8 38,0 | 3,00 | 43000 | |
| Max. ramping angle for insert Find the different ramping angle | is calculate s for all ava | d with facet ilable insert radii on technical inf | ormation p | age A254. | Flat |
| Radial depth of cut 0,20mm up t | o full cutter | diameter. | Facing Pitch | ||
| These tools have been designe EN ISO standard 15641:2001. | d, manufac | tured and tested in accordance w | ith | ||
| These tools are stocked without | an electro | nic chip. | |||
| Note: If using a insert with radiu diameter (D) minus 2 x chosen r | s, then the adius. | facing pitch for the 5702VZD cut | ter is equal | to the cutti | ng |
| Cylindrical Shanks or Special 30,000 RPM for diameters 50m G6.3 at 24,000 rpm. | HSK Integ m and belo | ral Shanksare designed and ba w. Diameters larger then 50mm | lanced to are balance | G6.3 at d to | |
| Cylindrical Shanktools mount i must be re-inspected for balanc user must balance the assembl Additional Balancing and Torque | edinashrii e as an ass y to a G6.3 values ca | nk fit holder or any other mill chu embly by the end user when at value minimum. n be found in the technical sectio | i ck holder + or exceedin n pages A | i inserts + s g 8,000 rp 256. | i crews m. End |
p