Каталог Stellram фрез со сменными пластинами - страница 228
Навигация
 Каталог Stellram твердосплавные цельные фрезы
 Каталог Stellram токарный инструмент
 Каталог Stellram системы со сменными пластинами для фрезерования с высокими подачами
 Каталог Stellram высокопроизводительные фрезерные системы
 Каталог Stellram материалы и сплавы
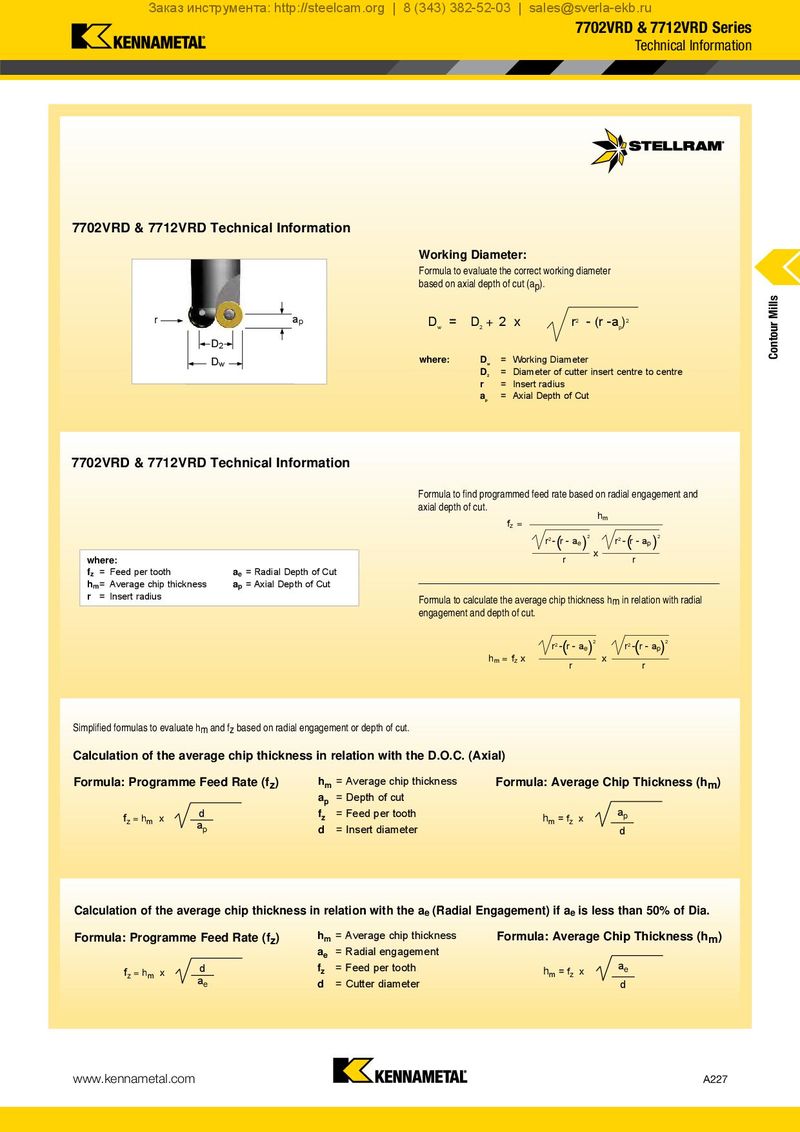
7702VRD & 7712VRD Technical Information
Working Diameter:
Formula to evaluate the correct working diameter
based on axial depth of cut (ap).
r a D = D + 2 x r - (r -a )
p 2 2
| w | 2 | p | |
| D2 |
D where: D = Working Diameter
w w = Diameter of cutter insert centre to centre D = Insert radius2
r a = Axial Depth of Cut p
7702VRD & 7712VRD Technical Information
where: f = Feed per tooth a = Radial Depth of Cut z e
h = Average chip thickness a = Axial Depth of Cut
m p r = Insert radius
Formula to find programmed feed rate based on radial engagement and
axial depth of cut. f h m
z ( (
r 2 - r - a )2 r 2 - r - a )2 e p x r r
Formula to calculate the average chip thickness hm in relation with radial
engagement and depth of cut.
r2 - r - a )2 r 2- r - a )2
| f x | e | x | p | |
| hm = |
z r r
Simplified formulas to evaluate hm and fz based on radial engagement or depth of cut.
Calculation of the average chip thickness in relation with the D.O.C. (Axial)
| Formula: Programme Feed Rate (f ) | h | = Average chip thickness | Formula: Average Chip Thickness (h | ) | |
| z | m | m | |||
| a = Depth of cut | |||||
| p |
| d | = Feed per tooth | a | ||||||
| f | x | f | = f x | p | ||||
| = hm | z | hm | ||||||
| z | a | = Insert diameter | z | d |
p d
Calculation of the average chip thickness in relation with the ae (Radial Engagement) if ae is less than 50% of Dia.
| Formula: Programme Feed Rate (f ) | h | = Average chip thickness | Formula: Average Chip Thickness (h | ) | |
| z | m | m | |||
| a = Radial engagement | |||||
| e |
d = Feed per tooth a
| f | x | f | h | = f x | e | |||
| = hm | z | m | z | |||||
| z | a | = Cutter diameter | d |
e d