Каталог Stellram фрез со сменными пластинами - страница 190
Навигация
 Каталог Stellram твердосплавные цельные фрезы
 Каталог Stellram токарный инструмент
 Каталог Stellram системы со сменными пластинами для фрезерования с высокими подачами
 Каталог Stellram высокопроизводительные фрезерные системы
 Каталог Stellram материалы и сплавы
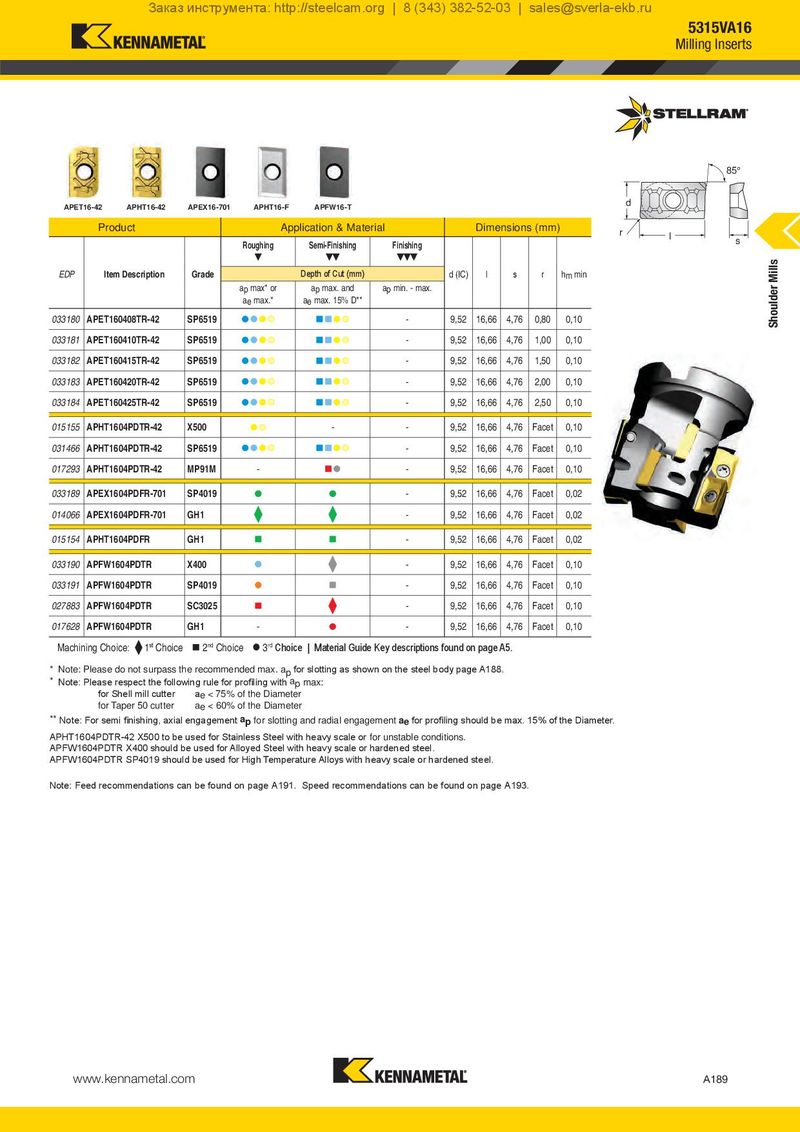
| APET | 16-42 APHT16-42 | APEX16-701 | APHT16-F | APFW16-T | d 85° | ||||||
| Product | Ap | plication & Mate | rial | Dime | nsion | s (mm | ) | l r | |||
| Roughing | Semi-Finishing | Finishing | s | ||||||||
| EDP | Item Description | Grade | Depth of Cut(mm) | d (IC) | l | s | r | hm min | |||
| ap max or ae max. | ap max. and ae max. 15% D | ap min. - max. | |||||||||
| 033180 | APET160408TR-42 | SP6519 | - | 9,52 | 16,66 | 4,76 | 0,80 | 0,10 | |||
| 033181 | APET160410TR-42 | SP6519 | - | 9,52 | 16,66 | 4,76 | 1,00 | 0,10 | |||
| 033182 | APET160415TR-42 | SP6519 | - | 9,52 | 16,66 | 4,76 | 1,50 | 0,10 | |||
| 033183 | APET160420TR-42 | SP6519 | - | 9,52 | 16,66 | 4,76 | 2,00 | 0,10 | |||
| 033184 | APET160425TR-42 | SP6519 | - | 9,52 | 16,66 | 4,76 | 2,50 | 0,10 | |||
| 015155 | APHT1604PDTR-42 | X500 | - | - | 9,52 | 16,66 | 4,76 | Facet | 0,10 | ||
| 031466 | APHT1604PDTR-42 | SP6519 | - | 9,52 | 16,66 | 4,76 | Facet | 0,10 | |||
| 017293 | APHT1604PDTR-42 | MP91M | - | - | 9,52 | 16,66 | 4,76 | Facet | 0,10 | ||
| 033189 | APEX1604PDFR-701 | SP4019 | - | 9,52 | 16,66 | 4,76 | Facet | 0,02 | |||
| 014066 | APEX1604PDFR-701 | GH1 | - | 9,52 | 16,66 | 4,76 | Facet | 0,02 | |||
| 015154 | APHT1604PDFR | GH1 | - | 9,52 | 16,66 | 4,76 | Facet | 0,02 | |||
| 033190 | APFW1604PDTR | X400 | - | 9,52 | 16,66 | 4,76 | Facet | 0,10 | |||
| 033191 | APFW1604PDTR | SP4019 | - | 9,52 | 16,66 | 4,76 | Facet | 0,10 | |||
| 027883 | APFW1604PDTR | SC3025 | - | 9,52 | 16,66 | 4,76 | Facet | 0,10 | |||
| 017628 | APFW1604PDTR | GH1 | - | - | 9,52 | 16,66 | 4,76 | Facet | 0,10 |
Machining Choice: 1st Choice 2nd Choice 3rd Choice | Material Guide Key descriptions found on page A5.
- Note: Please do not surpass the recommended max. ap for slotting as shown on the steel body page A188.
- Note: Please respect the following rule for profiling with ap max:
for Shell mill cutter ae < 75% of the Diameter for Taper 50 cutter ae < 60% of the Diameter ** Note: For semi finishing, axial engagement ap for slotting and radial engagement ae for profiling should be max. 15% of the Diameter. APHT1604PDTR-42 X500 to be used for Stainless Steel with heavy scale or for unstable conditions. APFW1604PDTR X400 should be used for Alloyed Steel with heavy scale or hardened steel. APFW1604PDTR SP4019 should be used for High Temperature Alloys with heavy scale or hardened steel. Note: Feed recommendations can be found on page A191. Speed recommendations can be found on page A193.