Каталог Stellram фрез со сменными пластинами - страница 124
Навигация
 Каталог Stellram твердосплавные цельные фрезы
 Каталог Stellram токарный инструмент
 Каталог Stellram системы со сменными пластинами для фрезерования с высокими подачами
 Каталог Stellram высокопроизводительные фрезерные системы
 Каталог Stellram материалы и сплавы
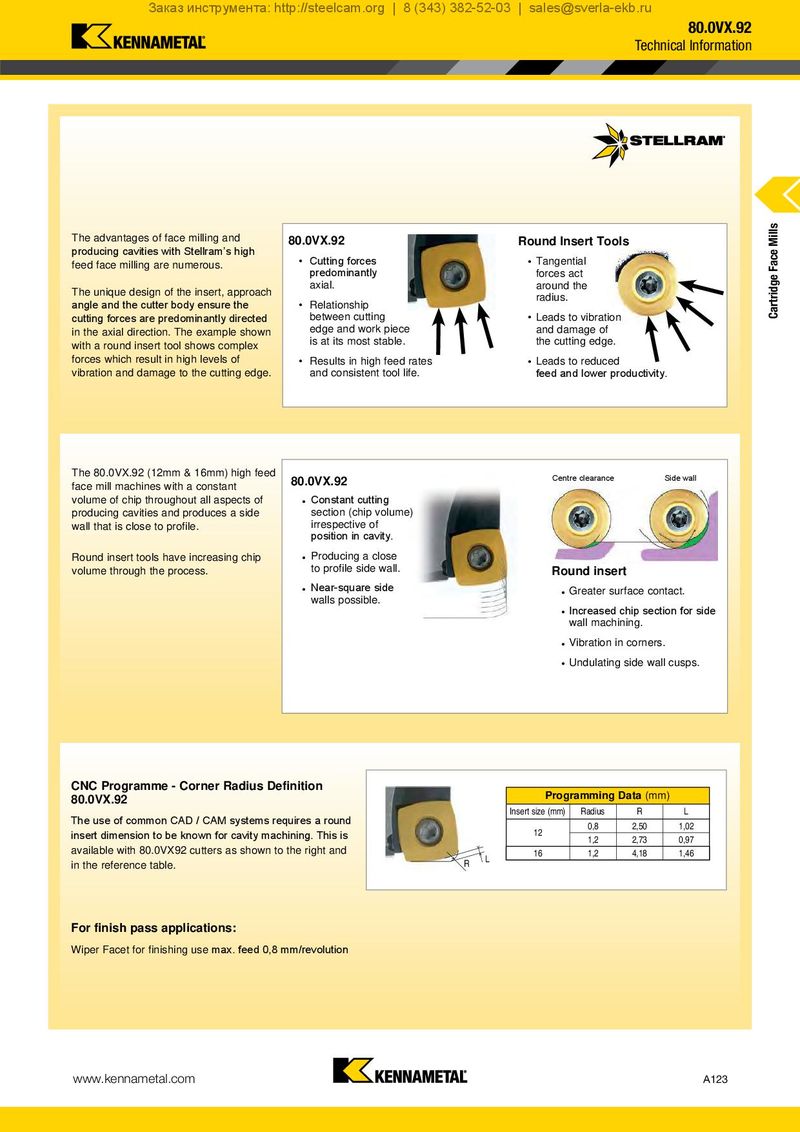
The advantages of face milling and 80.0VX.92 Round Insert Tools
producing cavities with Stellram’s high
- Cutting forces
- Tangential
feed face milling are numerous. predominantly forces act axial. around the The unique design of the insert, approach angle and the cutter body ensure the radius.
- Relationship
| cutting forces are predominantly directed | between cutting | • Leads to vibration | |
| in the axial direction. The example shown | edge and work piece | and damage of | |
| is at its most stable. | the cutting edge. | ||
| with a round insert tool shows complex | |||
| forces which result in high levels of | • Results in high feed rates | • Leads to reduced | |
| vibration and damage to the cutting edge. | and consistent tool life. | feed and lower productivity. |
The 80.0VX.92 (12mm & 16mm) high feed 80.0VX.92 face mill machines with a constant volume of chip throughout all aspects of Constant cutting
| producing cavities and produces a side | section (chip volume) |
| wall that is close to profile. | irrespective of |
| position in cavity. | |
| Round insert tools have increasing chip | • Producing a close |
| volume through the process. | to profile side wall. |
Near-square side walls possible.
Centre clearance Side wall
Round insert
- Greater surface contact. Increased chip section for side
wall machining.
- Vibration in corners.
- Undulating side wall cusps.
CNC Programme - Corner Radius Definition 80.0VX.92 Programming Data (mm)
| Insert size (mm) | Radius | R | L | |
| The use of common CAD / CAM systems requires a round | ||||
| 0,8 | 2,50 | 1,02 | ||
| insert dimension to be known for cavity machining. This is | 12 | |||
| 1,2 | 2,73 | 0,97 | ||
| available with 80.0VX92 cutters as shown to the right and | 16 | 1,2 | 4,18 | 1,46 |
R L in the reference table.
For finish pass applications: Wiper Facet for finishing use max. feed 0,8 mm/revolution