Общий каталог SGS 2018 - страница 50
Навигация
 Каталог SGS шестизубые фрезы T-carb
 Каталог SGS микро инструмент 2021
 Каталог SGS фрезы для алюминия S-carb
 Каталог SGS высокопроизводительные черновые фрезы
 Каталог SGS инструмент для обработки алюминия
 Общий каталог SGS 2015 на русском
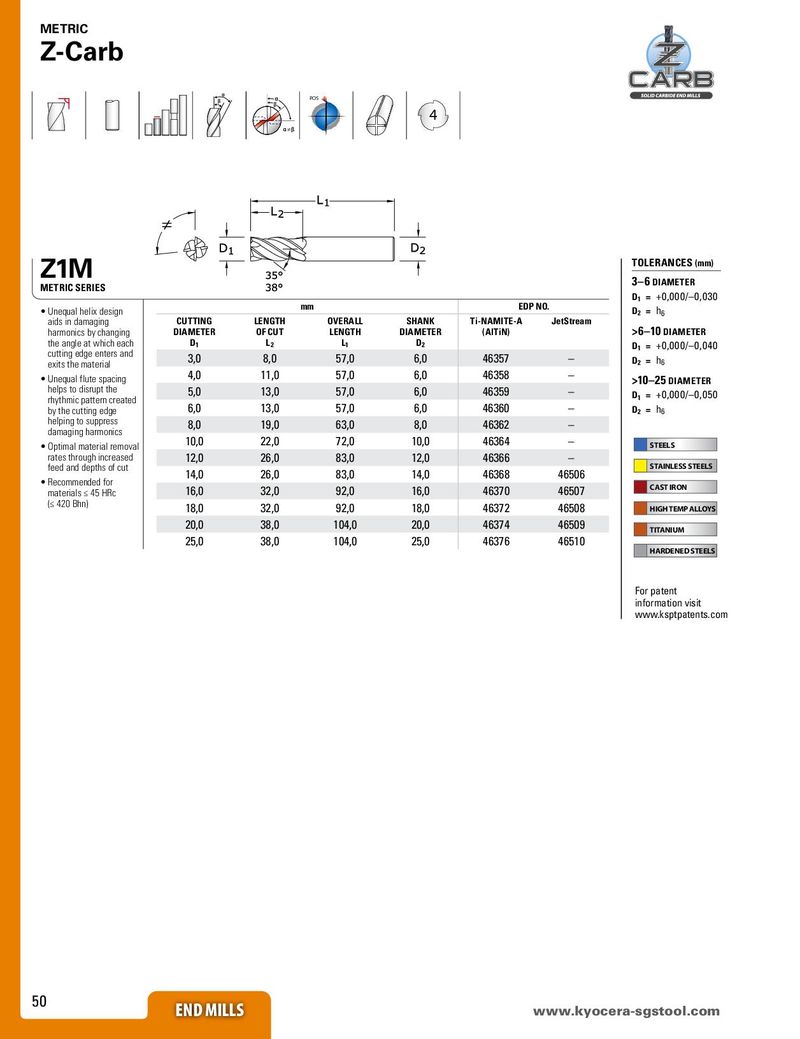
METRIC
Z-Carb
POS
4
≠
Z1M TOLERANCES (mm)
3–6 DIAMETER
METRIC SERIES
D1 = +0,000/–0,030
• Unequal helix design mm EDP NO. D2 = h6
aids in damaging CUTTING LENGTH OVERALL SHANK Ti-NAMITE-A JetStream
harmonics by changing DIAMETER OF CUT LENGTH DIAMETER (AlTiN) >6–10 DIAMETER
the angle at which each D1 L2 L1 D2 D1 = +0,000/–0,040
cutting edge enters and
exits the material
3,0 8,0 57,0 6,0 46357 – D2 = h6
• Unequal flute spacing 4,0 11,0 57,0 6,0 46358 – >10–25 DIAMETER
helps to disrupt the 5,0 13,0 57,0 6,0 46359 – D1 = +0,000/–0,050
rhythmic pattern created
by the cutting edge 6,0 13,0 57,0 6,0 46360 – D2 = h6
helping to suppress 8,0 19,0 63,0 8,0 46362 –
damaging harmonics
• Optimal material removal 10,0 22,0 72,0 10,0 46364 – STEELS
rates through increased 12,0 26,0 83,0 12,0 46366 –
feed and depths of cut STAINLESS STEELS
14,0 26,0 83,0 14,0 46368 46506
• Recommended for CAST IRON
materials ≤ 45 HRc 16,0 32,0 92,0 16,0 46370 46507
(≤ 420 Bhn)
18,0 32,0 92,0 18,0 46372 46508 HIGH TEMP ALLOYS
20,0 38,0 104,0 20,0 46374 46509 TITANIUM
25,0 38,0 104,0 25,0 46376 46510
HARDENED STEELS
For patent
information visit
www.ksptpatents.com
50
END MILLS END MILLS
www.kyocera-sgstool.com