Общий каталог SGS 2018 - страница 129
Навигация
 Каталог SGS шестизубые фрезы T-carb
 Каталог SGS микро инструмент 2021
 Каталог SGS фрезы для алюминия S-carb
 Каталог SGS высокопроизводительные черновые фрезы
 Каталог SGS инструмент для обработки алюминия
 Общий каталог SGS 2015 на русском
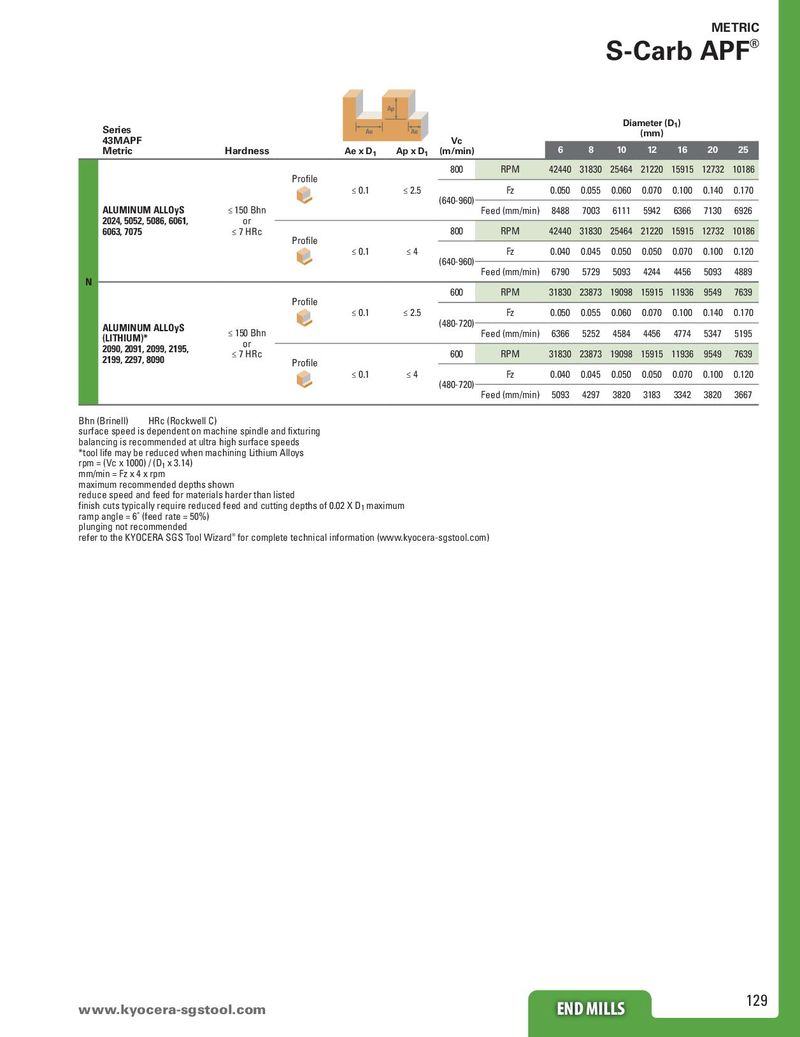
| Series 43MAPF | Ae | Ap Ae | Vc | Di | ameter (mm) | (D1) | |||||||
| Metric | Hardness | Ae x D1 | Ap x D1 | (m/min) | 6 | 8 | 10 | 12 | 16 | 20 | 25 | ||
| Profile | 800 | RPM | 42440 | 31830 | 25464 | 21220 | 15915 | 12732 | 10186 | ||||
| ≤ 0.1 | ≤ 2.5 | (640960) | Fz | 0.050 | 0.055 | 0.060 | 0.070 | 0.100 | 0.140 | 0.170 | |||
| ALUMINUM ALLOyS 2024 5052 5086 6061 | ≤ 150 Bhn | - | Feed (mm/min) | 8488 | 7003 | 6111 | 5942 | 6366 | 7130 | 6926 | |||
| , , , , 6063, 7075 | or ≤ 7 HRc | Profile | 800 | RPM | 42440 | 31830 | 25464 | 21220 | 15915 | 12732 | 10186 | ||
| ≤ 0.1 | ≤ 4 | (640-960) | Fz | 0.040 | 0.045 | 0.050 | 0.050 | 0.070 | 0.100 | 0.120 | |||
| N | Feed (mm/min) | 6790 | 5729 | 5093 | 4244 | 4456 | 5093 | 4889 | |||||
| Pfil | 600 | RPM | 31830 | 23873 | 19098 | 15915 | 11936 | 9549 | 7639 | ||||
| roe | |||||||||||||
| ≤ 0.1 | ≤ 2.5 | Fz | 0.050 | 0.055 | 0.060 | 0.070 | 0.100 | 0.140 | 0.170 | ||||
| ALUMINUM ALLOyS (LITHIUM) | ≤ 150 Bhn | (480-720) | Feed (mm/min) | 6366 | 5252 | 4584 | 4456 | 4774 | 5347 | 5195 | |||
| 2090, 2091, 2099, 2195, 2199, 2297, 8090 | or ≤ 7 HRc | Profile | 600 | RPM | 31830 | 23873 | 19098 | 15915 | 11936 | 9549 | 7639 | ||
| ≤ 0.1 | ≤ 4 | Fz | 0.040 | 0.045 | 0.050 | 0.050 | 0.070 | 0.100 | 0.120 | ||||
| (480-720) | Feed (mm/min) | 5093 | 4297 | 3820 | 3183 | 3342 | 3820 | 3667 |
Bhn (Brinell) HRc (Rockwell C) surface speed is dependent on machine spindle and fixturing balancing is recommended at ultra high surface speeds *tool life may be reduced when machining Lithium Alloys rpm = (Vc x 1000) / (D x 3.14) 1 mm/min = Fz x 4 x rpm maximum recommended depths shown reduce speed and feed for materials harder than listed finish cuts typically require reduced feed and cutting depths of 0.02 X D maximum 1 ramp angle = 6˚ (feed rate = 50%) plunging not recommended refer to the KYOCERA SGS Tool Wizard® for complete technical information (www.kyocera-sgstool.com)